PE CNC Machining Services

High-Precision Machining for Lightweight, Durable & Chemical-Resistant PE Parts
Custom Prototypes and Production with Reliable CNC Technology

What is PE CNC Machining?

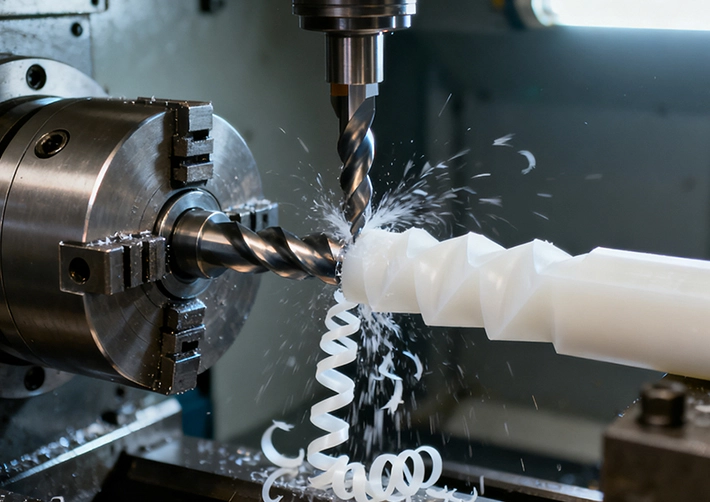
Polyethylene (PE) covers LDPE, MDPE, HDPE, HMW-PE and UHMW-PE. It’s lightweight, tough, and highly chemical-resistant—ideal for trays, guards, wear parts, and fluid-handling components.

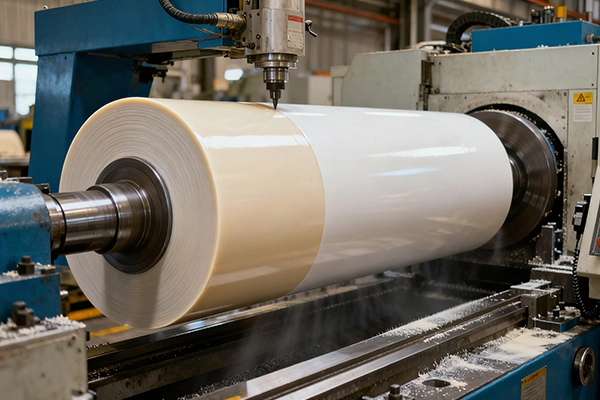
  • Tooling: Razor-sharp O-flute / polished carbide; high rake to shear clean chips.
  • Heat control: Air blast or light mist; avoid melting and chip-weld.
  • Feeds/Speeds: Higher feed, shallow step-over; steady chip load reduces fuzz.
  • Workholding: Vacuum/soft jaws; short stick-out for panels and thin walls.
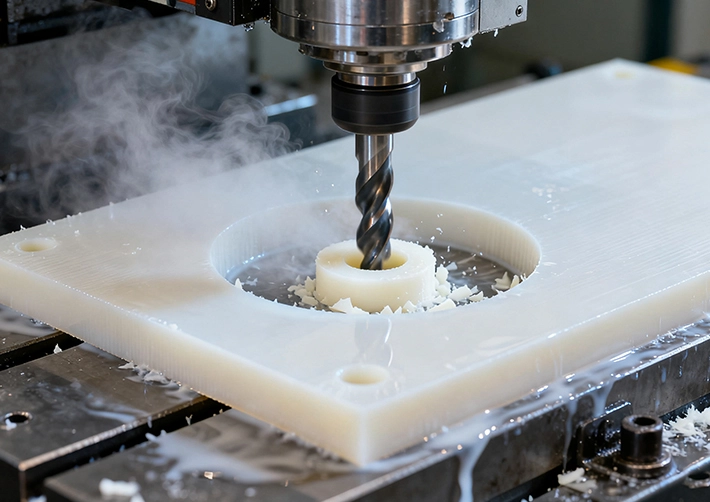
Polyethylene CNC machining overview with O-flute tooling and air blast
PE machining: wear parts, smooth finish, chemical resistance

Key Considerations

Use climb milling for cleaner edges, firm clamping, and a light finish pass on show faces. Deburr gently (blade/tumble) to avoid whitening.

For tight flatness and fit: rough → let the part rest/condition → finish passes. Mind thermal expansion and creep on large or thin geometries.

Precision PE CNC Machining

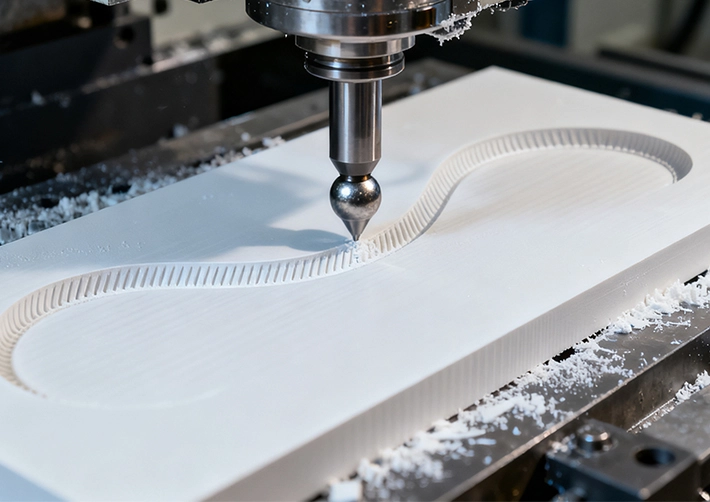
PE 3/4/5-axis CNC milling with vacuum fixturing and O-flute tools

3, 4, 5-Axis CNC Milling

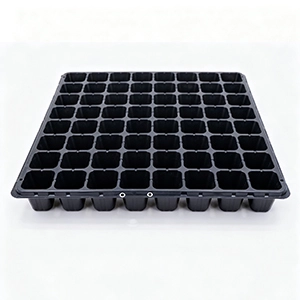
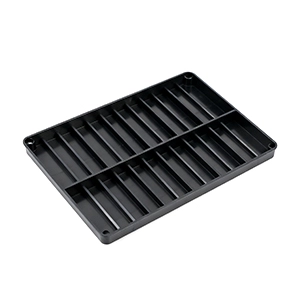
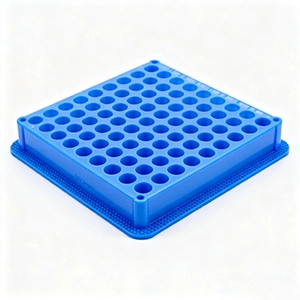
High-speed pocketing/contouring for trays, covers, nests, and manifolds. Sharp cutters and air blast deliver clean, uniform textures ready for assembly.

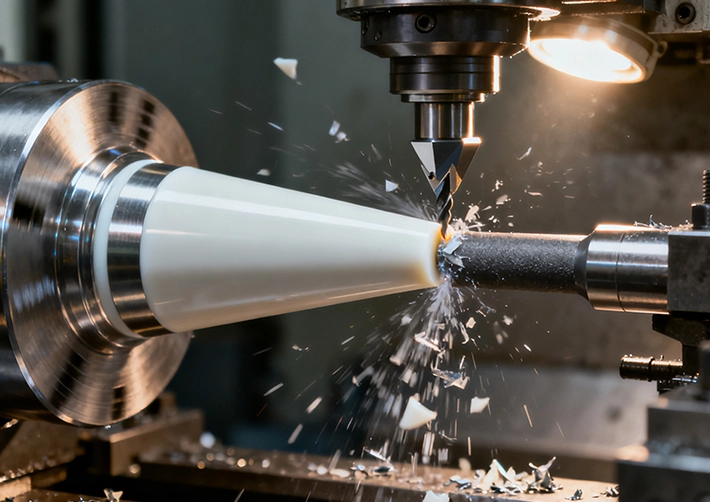
PE CNC turning and mill-turn for caps, spacers, and bushings

CNC Turning & Mill-Turn

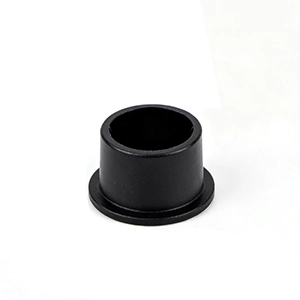
Smooth OD/ID finishes for fittings and spacers. Positive-rake inserts with generous chip-breaker geometry reduce fuzz and hold consistent diameters.

PE CNC Machining Capabilities

StandardsDetail
Max Part Size (X/Y/Z)2300 × 1500 × 600mm
Minimum Feature Size⊘1mm
Wall Thickness0.25mm
Tolerance+/-0.01
Surface Finish (as milled)Ra0.5–Ra3.2
Standard Lead Time3 working-days for rapid prototyping
Pricing LevelTo be confirmed after design review
Type of MachineGantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc...
Common Grades LDPE (Low-Density), HMW-PE (PE500), UHMW-PE (PE1000)

Machinable PE Grades

Choose the best balance of stiffness, wear, and dimensional stability.

LDPE machined panel with clean pockets (3:2)

LDPE (Low-Density)

  • Softer, more flexible; easy to cut
  • Great chemical resistance
  • Guards, covers, ducting
  • Economical choice

Use sharp O-flute, firm support; plan a light finish pass for clean edges.

HMW-PE abrasion-resistant plate and guide block for heavy-duty applications.

HMW-PE (PE500)

  • Higher wear/impact than LDPE/HDPE
  • Guides, wear plates, liners
  • Low water absorption
  • Good machinability

Moderate SFM and firm feed; skim pass for smooth cosmetic faces.

UHMW-PE wear rail and sliders (3:2)

UHMW-PE (PE1000)

  • Ultra-low friction & excellent wear
  • Very tough; more “gummy” to cut
  • Chute liners, rails, star wheels
  • Outstanding impact resistance

Use razor-sharp tools, generous chip-breaker geometry, and steady feed to avoid smearing.

Display of Our PE CNC Machining Parts

Material Machining Guide

PE CNC Machining: Selection, Process, and Quality Notes

PE is commonly considered for lightweight components, liners, guides, and general plastic machined parts. It is selected because of impact resistance and low moisture absorption. For CNC machining, the final result depends on material grade, toolpath strategy, tolerance allocation, surface finish, and inspection planning.

Good Fit

Use PE when the application benefits from impact resistance and low moisture absorption and the design can be machined with stable workholding.

Watch Points

Confirm wall thickness, hole depth, thread callouts, burr control, cosmetic surfaces, and finish buildup before production.

Quality Planning

Define critical dimensions, inspection method, tolerance class, and documentation requirements before the first article.

TopicPractical Guidance for PE
Design reviewSend 3D CAD, 2D drawings, material grade, finish notes, quantity, and critical-to-function dimensions.
Machining processMTSPi can review whether milling, turning, drilling, tapping, boring, or a combined route is best for the geometry.
Surface finishPlan cosmetic and functional finishing early, especially where coating thickness, polishing, or deburring affects fit.
InspectionUse calipers, micrometers, gauges, CMM, or visual inspection based on tolerance risk and assembly function.

FAQ

Is PE suitable for CNC machining?

Yes, PE can be CNC machined when the grade, geometry, tooling, workholding, and tolerance requirements are planned correctly.

What should I send for a PE machining quote?

Send CAD files, 2D drawings, quantity, material grade, finish requirements, tolerance notes, and any inspection or packaging needs.

Can PE parts be finished after machining?

Often yes. The right finish depends on the material family and part function. Confirm finish thickness and cosmetic expectations before machining.

How do I reduce cost on PE CNC parts?

Use practical tolerances, avoid unnecessary deep pockets or tiny holes, simplify setups, and reserve tight control for functional features.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

PE CNC Machining

We'll Send You Back with Price Immediately!