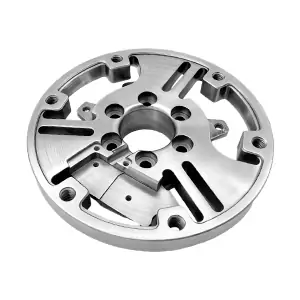
Any material considered suitable for 3-axis CNC machining must balance machinability,
dimensional stability, and in-service performance. Below are commonly used options
for prismatic parts and general milling.
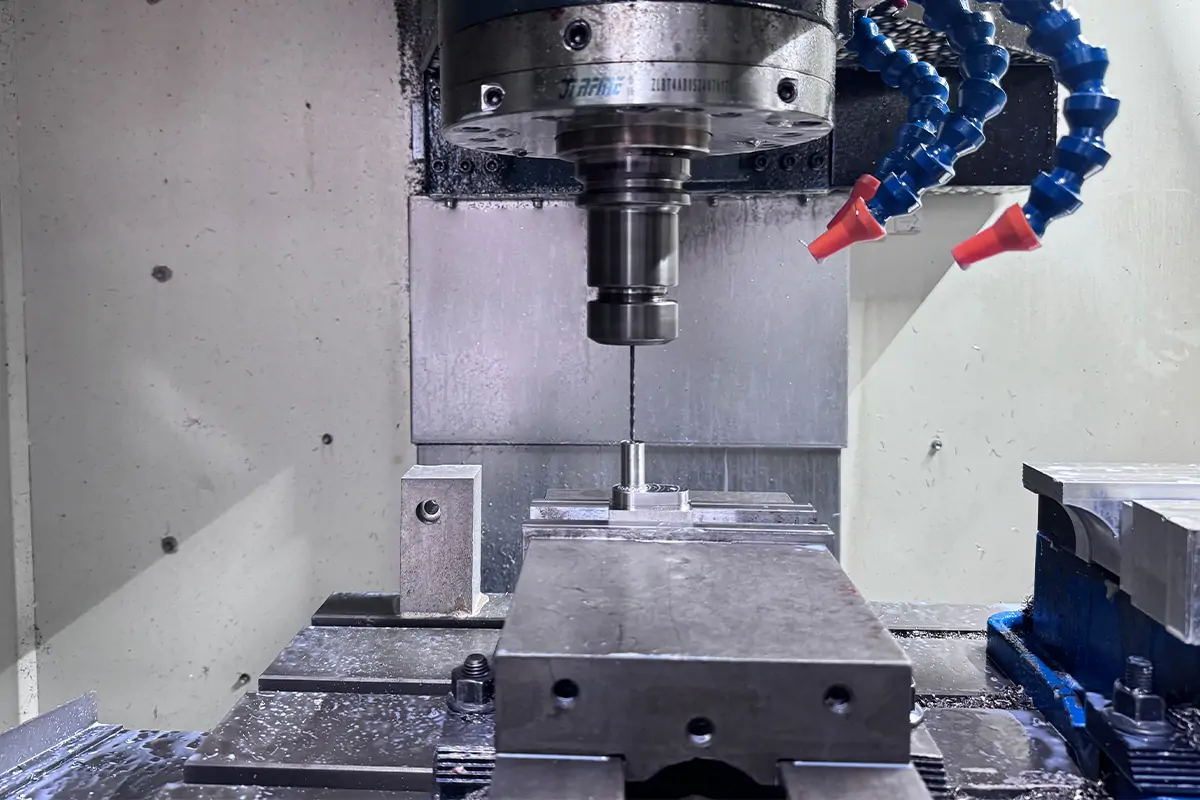
A 3-axis CNC machine moves its cutting tool along three linear axes: X (left-right), Y (front-back), and Z (up-down). This enables machining of surfaces, slots, and contours on one side per setup.
Cost Efficiency
Simpler setups and fast cycles lower part cost for prototypes and production.
Short Lead Times
Standard tools, fixtures and proven CAM libraries accelerate programming and machining.
Stable Accuracy
Straightforward kinematics and rigid workholding support tight tolerances.
Material Flexibility
Aluminum, steels, stainless, copper alloys and engineering plastics.
Scalable Production
Repeatable processes suited to batch runs, Kanban and VMI programs.
Consistent Finish
As‑milled Ra 1.6–3.2 µm typical; post‑finish options for cosmetic surfaces.
We standardize workholding and tool libraries across machines for repeatable results. In-process probing, SPC checks and documented setups keep tolerance and finish on target—shift after shift.

| 3-Axis Machining – Capacity & Typical Quality | ||
|---|---|---|
| Size | Metric units | Imperial units |
| Max. part size (XYZ travel) | 1100 × 650 × 500 mm | 43.3 × 25.6 × 19.7 in |
| Typical tolerance (milled) | ±0.005 mm | ±0.0002 in |
| Hole tolerance (reamed) | ±0.005 mm | ±0.0002 in |
| Surface finish (as-milled) | Ra 0.8–3.2 μm | Ra 32–126 µin |
| Surface finish (polished) | Ra ≤0.2 μm | Ra ≤8 µin |
*Adjust values to your actual machine envelope and QA capability.

Any material considered suitable for 3-axis CNC machining must meet high standards of reliability and performance. The following are some commonly used materials for CNC machining:
Meitesi provides surface finishes for 3-axis parts, enhancing appearance, smoothness, durability, and hiding tool marks for high-quality results.
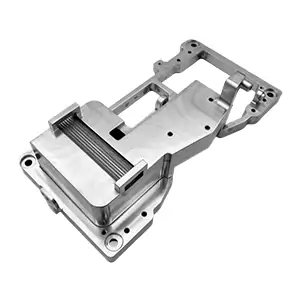
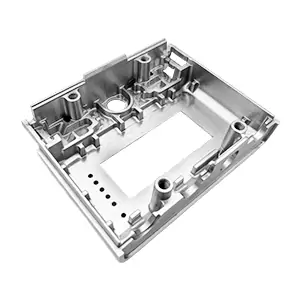
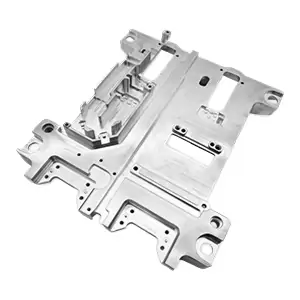
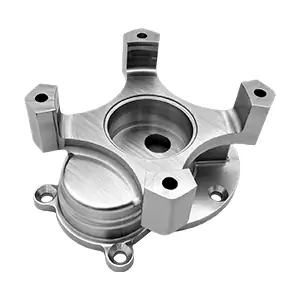
3-axis CNC machining is often the most efficient route for flat, prismatic, and one-side-access parts such as plates, brackets, housings, covers, fixtures, adapter blocks, and simple pockets. MTSPi CNC uses 3-axis milling when the part can be made accurately with X, Y, and Z movement without unnecessary repositioning.
For buyers, the main question is not only whether a part can be milled, but whether the drawing has realistic internal radii, reachable pocket depths, clear datums, and practical tolerance notes. Our team reviews these details before quoting so 3-axis machining stays cost-effective and repeatable.
| Buyer need | Why it matters | Typical parts |
|---|---|---|
| Simple milled geometry | Lower setup complexity and efficient toolpaths | Brackets, plates, covers, fixtures, and housings |
| Tight pockets and hole patterns | Stable milling, drilling, tapping, counterboring, and reaming | Assembly plates, manifolds, adapters, and mounting blocks |
| Prototype to low volume | Fast route for real metal and plastic functional parts | Engineering samples, test fixtures, and short production runs |
| Cost-sensitive machining | Avoids multi-axis setup when geometry does not require it | Parts where one or two setups can complete the required features |
For accurate quoting, send 3D CAD data, 2D drawings, material grade, quantity, tolerance notes, finish requirements, and any assembly or inspection concerns. MTSPi CNC can review manufacturability before machining so the process matches the part function, not only the page name.
These related pages help buyers compare machining routes, material choices, cost drivers, and inspection requirements.
What parts are best for 3-axis CNC machining? 3-axis machining is best for plates, brackets, fixtures, housings, covers, blocks, and other milled parts where most features can be reached from one or a few flat setups.
When should I choose 4-axis or 5-axis instead? Choose 4-axis when rotary access reduces repositioning or supports cylindrical features. Choose 5-axis when angled faces, complex contours, or multiple hard-to-reach surfaces require better tool access.
How can I lower 3-axis machining cost? Use realistic tolerances, allow larger internal radii, avoid very deep narrow pockets, identify only critical dimensions, and clarify finish requirements before quoting.