PEI Machining CNC Services

High-Precision Machining for Heat-Resistant & High-Strength PEI Components
Custom Prototypes and Production with Advanced CNC Expertise

What is PEI CNC Machining?

Polyetherimide (PEI), often known by the trade name ULTEM®, is a high-temperature engineering plastic with excellent rigidity, creep resistance, and dimensional stability. It machines crisply with sharp carbide and controlled heat, making it ideal for aerospace, semiconductor, and medical components.

  • Tooling: Sharp micro-polished carbide (TiAlN/TiCN when needed); high positive rake.
  • Heat control: Air blast or light mist; avoid local overheating and stress whitening.
  • Feeds/Speeds: Moderate SFM with steady chip load; finish pass for critical faces.
  • Workholding: Rigid fixturing/soft jaws; minimize vibration on thin walls.
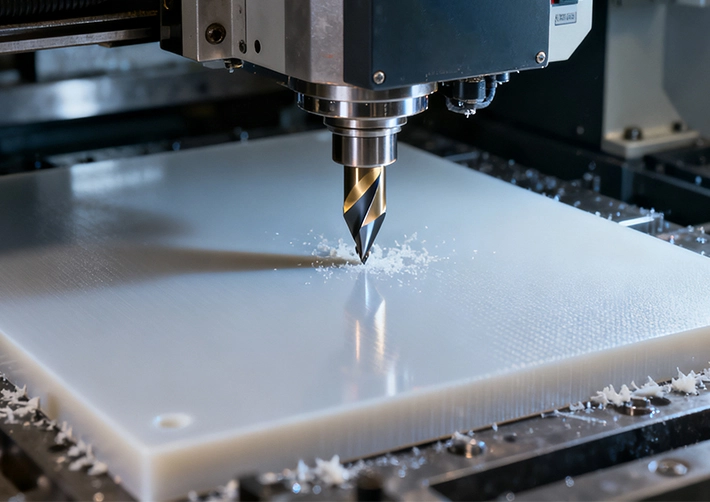
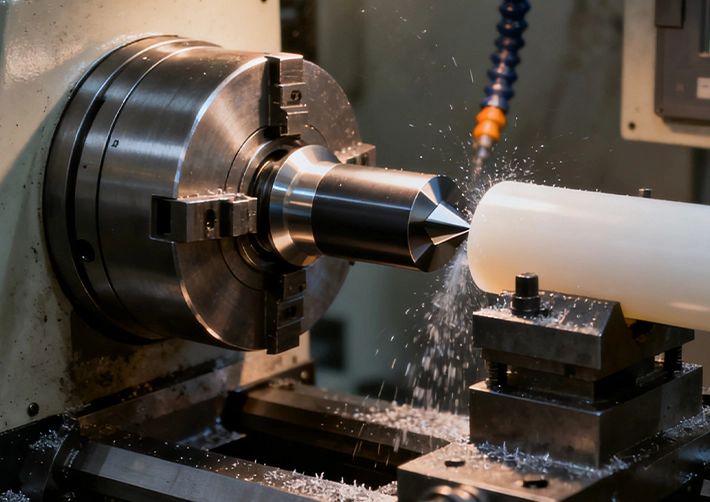
PEI (ULTEM) CNC machining with air blast and sharp carbide tooling
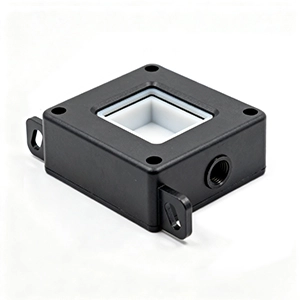
PEI machined parts highlighting dimensional stability and heat resistance

Key Considerations

PEI is notch-sensitive—avoid sharp internal corners and heavy deburr pressure. For tight stability on large or thin parts, use a rough → condition/anneal → finish approach.

Keep moisture low (dry stock before machining if required). Use climb milling for cleaner edges and a light skim on show surfaces to unify color/texture.

Precision PEI CNC Machining

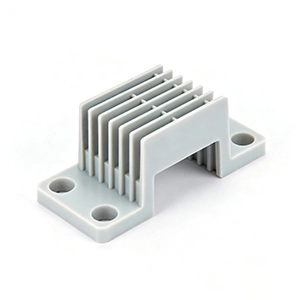
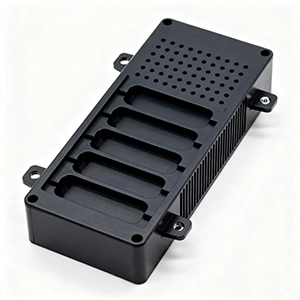
PEI 3/4/5-axis CNC milling for precision brackets and housings

3, 4, 5-Axis CNC Milling

Accurate pocketing/contouring with excellent dimensional stability. Balanced holders, sharp cutters, and controlled step-over deliver clean edges ready for assembly or finishing.

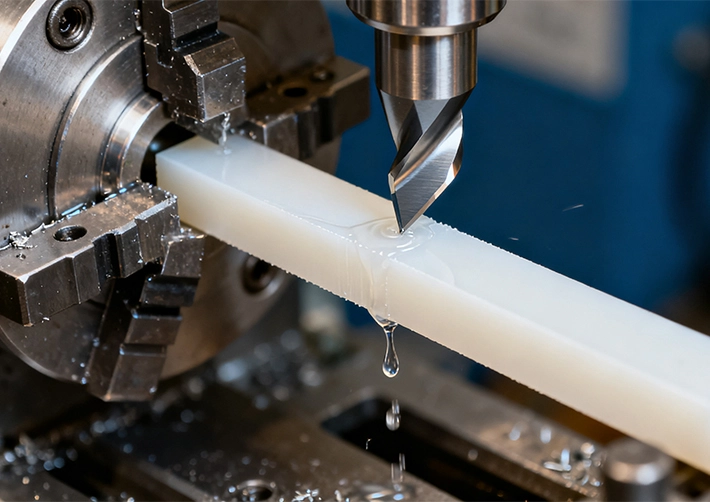
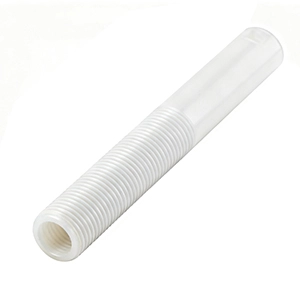
PEI CNC turning and mill-turn for bushings, insulators, and manifolds

CNC Turning & Mill-Turn

Smooth OD/ID finishes on rings, insulators, and manifolds. Positive-rake geometry and steady chip load help avoid haze and hold tight diametric tolerance.

PEI CNC Machining Capabilities

StandardsDetail
Max Part Size (X/Y/Z) 2300 × 1500 × 600mm
Minimum Feature Size ⊘1mm
Wall Thickness 0.25mm
Tolerance +/-0.01
Surface Finish (as milled) Ra0.5–Ra3.2
Standard Lead Time 3 working-days for rapid prototyping
Pricing Level To be confirmed after design review
Type of Machine Gantry CNC / 3-4-5-Axis CNC / Mill-Turn Compound CNC / Swiss-Type CNC / Turning Machine...etc...
Common Grades Unfilled PEI (ULTEM® 1000), Glass-Filled 30% (ULTEM® 2300), ESD / Carbon-Loaded PEI, Black / Pigmented PEI

Machinable PEI Grades

Select the right balance of stiffness, heat resistance, and ESD/weight targets.

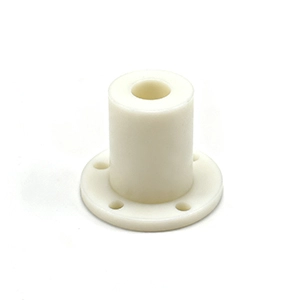
Unfilled PEI (ULTEM 1000) machined parts (3:2)

Unfilled PEI (ULTEM® 1000)

  • High heat & rigidity, excellent stability
  • Good dielectric properties
  • Clean machining; finish pass recommended
  • Aerospace/semiconductor manifolds, covers

Dry stock if needed; use sharp carbide and steady chip load to avoid edge haze.

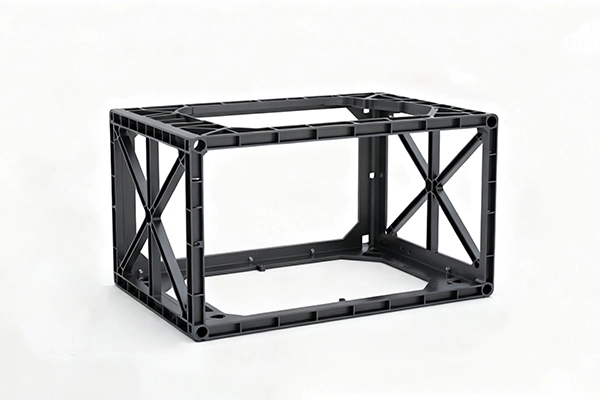
Glass-filled PEI (ULTEM 2300 GF30) structural bracket (3:2)

Glass-Filled 30% (ULTEM® 2300)

  • Much higher stiffness & HDT
  • More abrasive—use coated tools
  • Dimensional stability improved
  • Housings, brackets, fixtures

Lower SFM and steady feed; inspect edges frequently to maintain finish and tolerance.

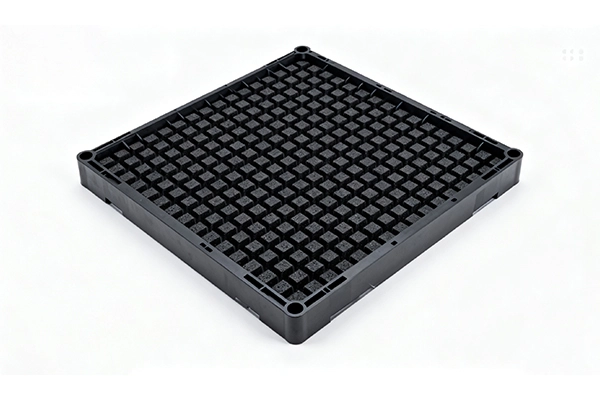
ESD-safe PEI fixture and tray (3:2)

ESD / Carbon-Loaded PEI

  • Static-safe parts & tooling
  • Fillers change chip behavior
  • Trays, nests, covers
  • Surface resistivity to spec

Tune feeds for sharp edges; confirm resistivity targets and cleaning/handling requirements.

Black pigmented PEI machined housing (3:2)

Black / Pigmented PEI

  • Light-blocking for enclosures
  • Similar parameters to unfilled
  • Consistent color/texture control
  • Great for cosmetic housings

Use a light skim pass on show surfaces to unify gloss/texture; follow cosmetic specs if any.

Display of Our PEI CNC Machining Parts

Material Machining Guide

PEI CNC Machining: Selection, Process, and Quality Notes

PEI is commonly considered for high-temperature electrical, aerospace, and precision plastic components. It is selected because of heat resistance and dimensional stability. For CNC machining, the final result depends on material grade, toolpath strategy, tolerance allocation, surface finish, and inspection planning.

Good Fit

Use PEI when the application benefits from heat resistance and dimensional stability and the design can be machined with stable workholding.

Watch Points

Confirm wall thickness, hole depth, thread callouts, burr control, cosmetic surfaces, and finish buildup before production.

Quality Planning

Define critical dimensions, inspection method, tolerance class, and documentation requirements before the first article.

TopicPractical Guidance for PEI
Design reviewSend 3D CAD, 2D drawings, material grade, finish notes, quantity, and critical-to-function dimensions.
Machining processMTSPi can review whether milling, turning, drilling, tapping, boring, or a combined route is best for the geometry.
Surface finishPlan cosmetic and functional finishing early, especially where coating thickness, polishing, or deburring affects fit.
InspectionUse calipers, micrometers, gauges, CMM, or visual inspection based on tolerance risk and assembly function.

FAQ

Is PEI suitable for CNC machining?

Yes, PEI can be CNC machined when the grade, geometry, tooling, workholding, and tolerance requirements are planned correctly.

What should I send for a PEI machining quote?

Send CAD files, 2D drawings, quantity, material grade, finish requirements, tolerance notes, and any inspection or packaging needs.

Can PEI parts be finished after machining?

Often yes. The right finish depends on the material family and part function. Confirm finish thickness and cosmetic expectations before machining.

How do I reduce cost on PEI CNC parts?

Use practical tolerances, avoid unnecessary deep pockets or tiny holes, simplify setups, and reserve tight control for functional features.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

PEI CNC Machining

We'll Send You Back with Price Immediately!