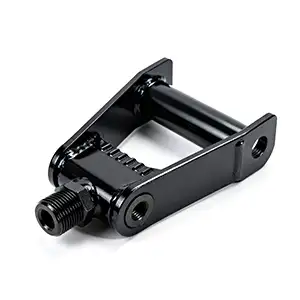
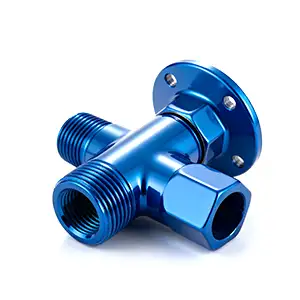
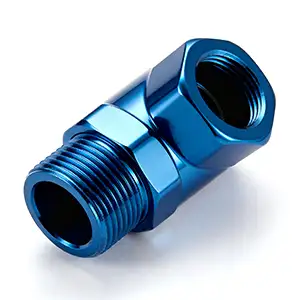
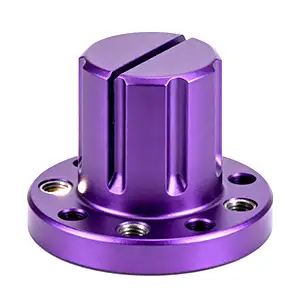
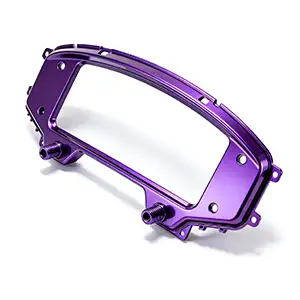
Our E-Coating service provides a uniform, corrosion-resistant, and environmentally friendly finish.
It ensures even coverage on complex geometries, delivers long-lasting protection, and serves as
an excellent primer or final coating for industrial components.
Our E-Coating service provides a uniform, corrosion-resistant, and environmentally friendly finish. It ensures even coverage on complex geometries, delivers long-lasting protection, and serves as an excellent primer or final coating for CNC and industrial components.
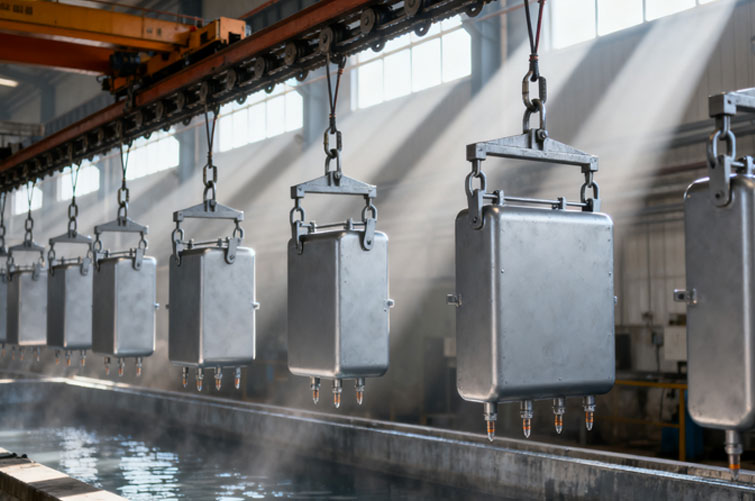
E-coating (electrophoretic deposition) applies electrically charged paint particles to a conductive part immersed in a bath, then bakes the film to cure. The process yields a thin, highly uniform coating with excellent edge and recess coverage, reaching complex geometries where spray can’t. Typical thickness is tightly controlled (e.g., ~15–35 µm), providing strong corrosion protection and a smooth, consistent appearance.
Because coverage is so complete and repeatable, E-coating is ideal for parts that demand durability and consistency before or instead of topcoats. It’s widely used across automotive, heavy equipment, and appliances for chassis, brackets, housings, and fasteners, often paired with powder coat or paint for color and added weathering performance.
Ensures complete and consistent coating, even on complex geometries.
Delivers superior resistance against rust and environmental degradation.
Uses water-based formulations with minimal VOCs for a sustainable finish.
| Feature | Info |
|---|---|
| Coverage | Uniform deposition, reaches edges, recesses, and cavities |
| Durability | Resistant to corrosion, chemicals, and environmental stress |
| Applications | Automotive, appliances, construction, industrial machinery |
| Lead Time | Typically 3–7 business days depending on part complexity |
| Quality Checks | Thickness measurement, adhesion testing, corrosion resistance evaluation |
E-Coating Service for CNC Metal Components helps CNC part buyers create uniform protective coating on complex surfaces, recesses, and internal areas. MTSPi CNC reviews the machined geometry, material grade, tolerance-sensitive areas, cosmetic expectations, and inspection needs before recommending a finishing route.
This page is written for sourcing and engineering teams that need practical finishing decisions, not just a process name. Share drawings, material, quantity, finish standard, color or texture target, masking requirements, and critical dimensions with the RFQ.
| Buyer question | Why it matters | Practical action |
|---|---|---|
| Material compatibility | Confirm that the material and alloy can accept the finish reliably | Avoid adhesion, color, hardness, or corrosion problems |
| Dimensional impact | Review coating thickness, edge build-up, holes, threads, masking, and critical fits | Protect assembly dimensions after finishing |
| Appearance standard | Define visible faces, gloss, matte texture, color range, and acceptable marks | Keep cosmetic expectations realistic |
| Inspection needs | Select visual checks, thickness checks, hardness checks, adhesion tests, or sample approval as needed | Match evidence to part function and buyer risk |
Surface treatment should be planned before final machining whenever possible. Threads, bores, bearing fits, sealing faces, electrical contact areas, and cosmetic surfaces may need different handling. For repeat work, keep a finish sample, color reference, thickness target, and packaging instruction with the drawing revision.
What should I confirm before choosing this finish? Confirm material grade, part function, cosmetic standard, masking needs, tolerance-sensitive surfaces, expected environment, and inspection requirements.
Can MTSPi CNC machine and finish the same parts? Yes. MTSPi CNC can support machining, finishing coordination, inspection, and packaging so the finish plan matches the machined part requirements.
Will surface treatment affect dimensions? Some finishes add thickness, change edges, or affect holes and threads. Critical fits should be marked on the drawing and masking or post-finish checks should be discussed early.