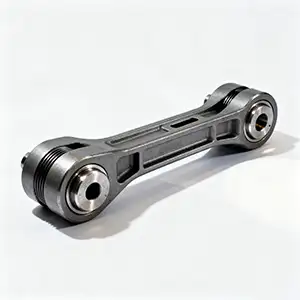
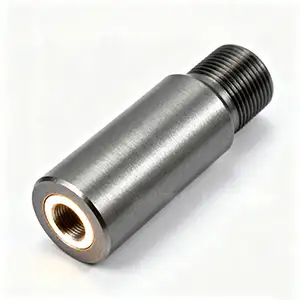
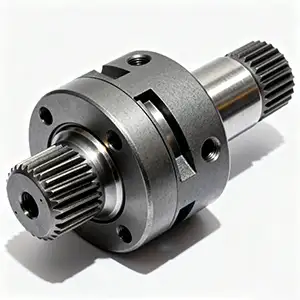
Nitriding is a heat treatment process that enriches the surface of steel with nitrogen, producing a hard,
wear-resistant layer while maintaining a strong and stable core.
CNC nitriding services enhance surface hardness, fatigue life, and corrosion resistance without compromising core toughness. Perfect for gears, shafts, molds, and high-performance parts in demanding industries.
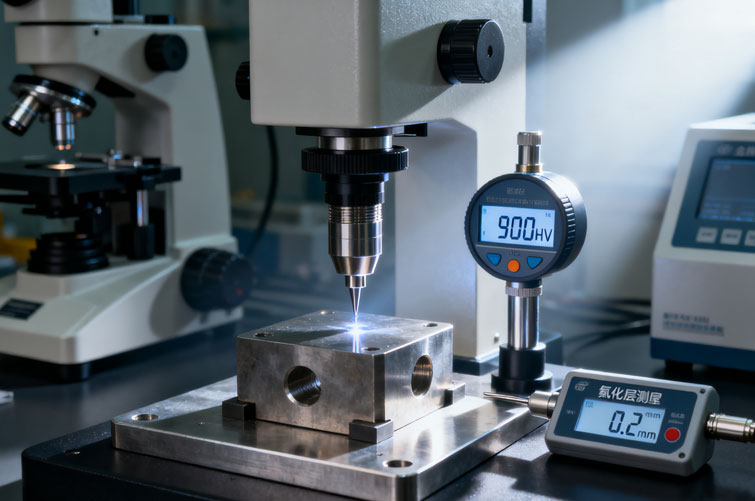
Nitriding is a thermochemical surface treatment in which nitrogen atoms diffuse into the surface of steel or alloy parts at relatively low temperatures (500–550°C). The process creates a hard nitride layer that significantly improves wear resistance and surface hardness.
Because nitriding does not require quenching, distortion is minimized, making it an excellent choice for precision CNC machined components. It also enhances fatigue resistance and provides some corrosion protection, especially when applied to alloy steels with nitride-forming elements such as chromium, molybdenum, or aluminum.
Produces a hard nitride surface layer that resists abrasion and extends part life.
Performed at lower temperatures, reducing distortion in precision CNC components.
Boosts fatigue life and provides added corrosion protection for demanding parts.
| Feature | Info |
|---|---|
| Case Depth | 0.1–0.6 mm, depending on process and duration. |
| Surface Hardness | Typically 900–1200 HV, providing excellent wear resistance. |
| Distortion Control | Low processing temperatures minimize dimensional changes. |
| Industries | Automotive, aerospace, tooling, precision engineering. |
Nitriding Service for Hardened Steel CNC Parts helps CNC part buyers increase surface hardness and wear resistance with lower distortion than some high-temperature hardening routes. MTSPi CNC reviews the machined geometry, material grade, tolerance-sensitive areas, cosmetic expectations, and inspection needs before recommending a finishing route.
This page is written for sourcing and engineering teams that need practical finishing decisions, not just a process name. Share drawings, material, quantity, finish standard, color or texture target, masking requirements, and critical dimensions with the RFQ.
| Buyer question | Why it matters | Practical action |
|---|---|---|
| Material compatibility | Confirm that the material and alloy can accept the finish reliably | Avoid adhesion, color, hardness, or corrosion problems |
| Dimensional impact | Review coating thickness, edge build-up, holes, threads, masking, and critical fits | Protect assembly dimensions after finishing |
| Appearance standard | Define visible faces, gloss, matte texture, color range, and acceptable marks | Keep cosmetic expectations realistic |
| Inspection needs | Select visual checks, thickness checks, hardness checks, adhesion tests, or sample approval as needed | Match evidence to part function and buyer risk |
Surface treatment should be planned before final machining whenever possible. Threads, bores, bearing fits, sealing faces, electrical contact areas, and cosmetic surfaces may need different handling. For repeat work, keep a finish sample, color reference, thickness target, and packaging instruction with the drawing revision.
What should I confirm before choosing this finish? Confirm material grade, part function, cosmetic standard, masking needs, tolerance-sensitive surfaces, expected environment, and inspection requirements.
Can MTSPi CNC machine and finish the same parts? Yes. MTSPi CNC can support machining, finishing coordination, inspection, and packaging so the finish plan matches the machined part requirements.
Will surface treatment affect dimensions? Some finishes add thickness, change edges, or affect holes and threads. Critical fits should be marked on the drawing and masking or post-finish checks should be discussed early.