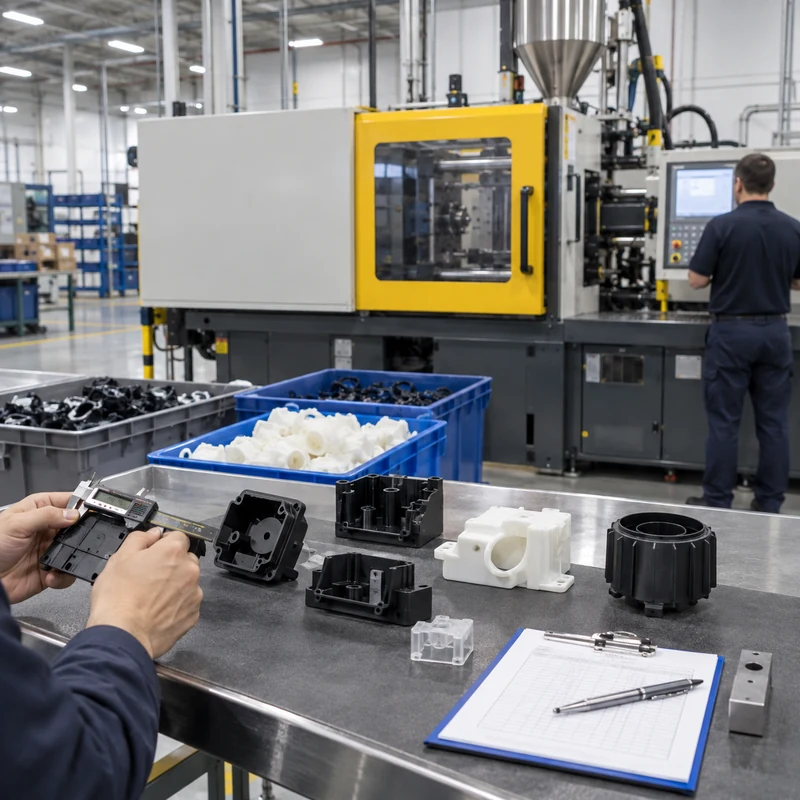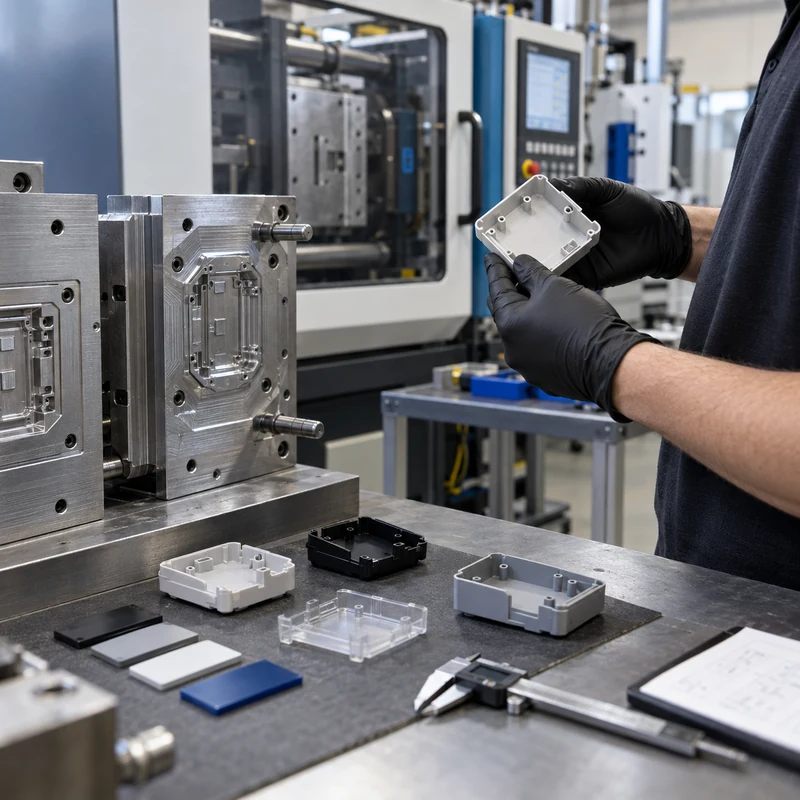
Low-volume injection molding fills the gap between prototypes and stable mass production. It can supply pilot builds, bridge production, market tests, service parts, regulated validation lots, and products with modest lifetime demand. The supplier must optimize for change, speed, and risk rather than only maximum press utilization.
This guide explains how to compare low-volume injection molding companies using evidence that affects your actual program: tooling approach, DFM, resin experience, dimensional control, revision handling, capacity, and total cost.
Quick Answer
Choose a supplier that matches your volume and uncertainty. Aluminum or simplified steel tooling can shorten lead time, but tooling decisions must still support resin temperature, surface finish, tolerances, expected shots, and future changes. Validate geometry before hardening the supply chain.
Key Differences at a Glance
| Factor | Option A | Option B | Engineering note |
|---|---|---|---|
| Tool objective | Fast bridge or prototype mold | Long-life production mold | Choose around lifetime shots and revision risk |
| Typical flexibility | High | Lower after completion | Early programs benefit from replaceable inserts |
| Automation | Selective | Often extensive | Do not pay for automation without volume |
| Validation | Fit-for-purpose | Full production qualification | Regulatory needs may require either |
| Unit cost | Higher | Lower at volume | Compare total program cost |
Define Low Volume Before Requesting Quotes
Low volume may mean dozens of parts for one company and tens of thousands for another. State annual demand, lot size, product life, launch date, and demand uncertainty. Include expected resin, color, cosmetic class, tolerances, and secondary operations.
Tooling Strategies
Prototype molds may use aluminum, pre-hardened steel, modular bases, manual inserts, or single-cavity layouts. Each choice trades tooling cost against cycle time, life, maintenance, finish, and repeatability.
- Ask who owns the mold and CAD data
- Confirm expected tool life and maintenance
- Define included sampling rounds
- Clarify transfer rights and compatible press base
- Use replaceable inserts for likely design changes
DFM and Mold-Flow Review
A supplier should review draft, wall thickness, ribs, bosses, undercuts, gate location, weld lines, venting, cooling, shrinkage, and ejection. A quote with no engineering questions may simply defer risk until the first sample.
- Use uniform walls where practical
- Keep ribs thinner than adjacent walls
- Provide draft based on texture and depth
- Protect cosmetic surfaces from gates and ejectors
- Identify dimensions that truly control function
Quality and First-Article Approval
Low quantity does not eliminate the need for a stable process. Define an inspection plan and approval sample. For critical dimensions, ask how variation across cavities, cycles, resin lots, and environmental conditions will be controlled.
- Material certificates and lot traceability
- First Article Inspection
- Color and cosmetic limit samples
- Gauge strategy for recurring lots
- Documented process settings and change control
Lead Time and Capacity
Fast tooling is useful only if the supplier also has press time, resin, secondary operations, and inspection capacity. Ask for a schedule from DFM approval through tool build, T1 sample, revisions, validation, and production release.
CNC Prototypes Before Molding
CNC machining can validate production-intent material, fasteners, sealing surfaces, flatness, and interfaces before mold steel is cut. It is particularly useful when a late dimensional change would require welding and re-machining a mold insert.
- Prototype high-risk interfaces first
- Use the same controlled drawing revision
- Record assembly findings
- Update both CAD and inspection plan before tooling
Supplier Red Flags
Warning signs include vague tool ownership, no discussion of resin drying or shrinkage, unrealistic lead time without a schedule, weak change control, and an inability to explain how critical dimensions will be measured.
Frequently Asked Questions
What quantity suits low-volume injection molding?
It depends on part size, tool complexity, and economics. Programs can range from hundreds to tens of thousands of parts; compare molding with CNC, urethane casting, and additive manufacturing using total program cost.
Is aluminum tooling suitable?
Often yes for prototype and bridge programs, but abrasive or high-temperature resins, complex slides, tight cosmetics, and long life may justify steel.
How can tooling risk be reduced?
Complete DFM, prototype critical features, identify likely revisions, use modular inserts where practical, and define sample approval before production.