

Categories
Blog Design, Cost & Sourcing Manufacturing Process Comparisons

Progressive Die Stamping: How to Know If It Fits Your Part

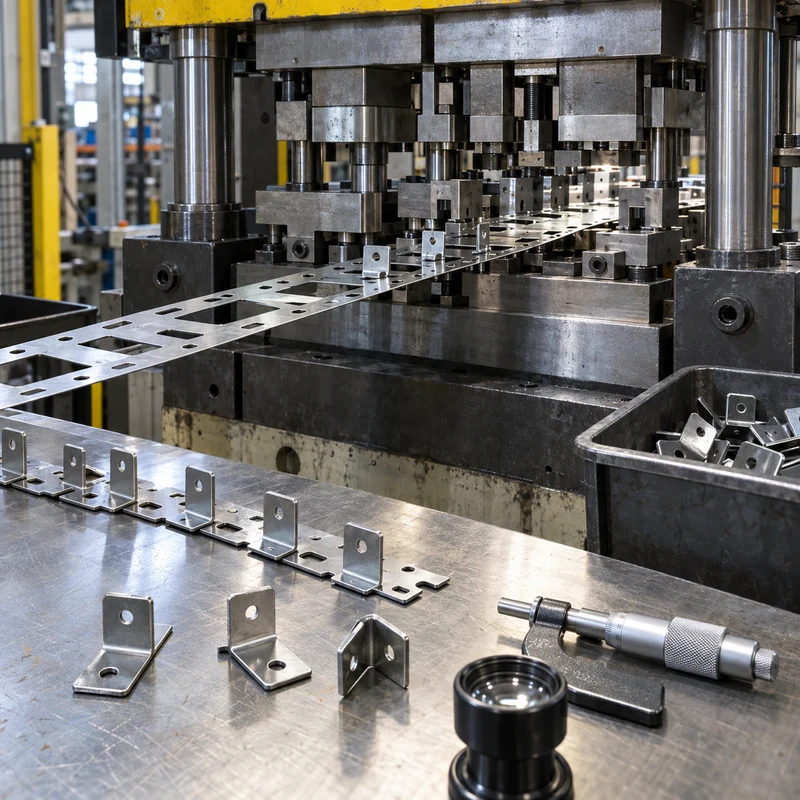
Progressive die stamping moves a continuous metal strip through a sequence of stations. Each press stroke performs operations such as piercing, trimming, coining, bending, drawing, and cutoff. Once the tool is proven, the process can produce complex sheet-metal parts at high speed and low unit cost.

The economic advantage depends on suitable geometry and enough stable volume to recover tooling investment. This guide shows how to decide whether a part belongs in a progressive die or should remain with laser cutting, forming, machining, or another process.

Quick Answer

Progressive die stamping fits repeatable sheet-metal parts with high annual volume, stable design, coil-compatible material, and features that can be formed through sequential stations. It is a poor fit for uncertain demand, frequent revisions, very low quantities, thick 3D geometry, or tolerances that require extensive secondary machining.

Key Differences at a Glance

Factor Option A Option B Engineering note
Volume High repeat demand Prototype or low demand Tooling payback drives the decision
Design stability Frozen geometry Frequent revisions Tool changes can be expensive
Geometry Sequential sheet operations Deep 3D machined features A feasible strip layout is essential
Unit cost Very low after launch Higher but flexible Include scrap and maintenance
Lead time Longer tooling launch Short setup Bridge production may be needed

How the Progressive Die Works

Stock uncoils and advances by a fixed pitch. Pilot features register the strip, while each station adds a controlled operation. The carrier keeps parts connected until cutoff. Strip layout determines material use, station count, force balance, progression, and tool size.

Best-Fit Part Characteristics

Good candidates are small to medium sheet-metal parts with repeated holes, tabs, forms, embosses, and bends. Terminals, clips, brackets, shields, contacts, and retainers are common examples.

  • Stable annual demand
  • Consistent coil material and thickness
  • Features that can be reached from the press direction
  • Tolerances compatible with stamping and springback
  • Sufficient web and carrier material

Design Factors That Control Feasibility

Hole-to-edge distance, bend radius, material grain, formed-feature spacing, burr direction, flatness, and springback all influence the tool. Very tight features may require shaving, coining, restriking, sensors, or secondary operations.

  • Use bend radii appropriate to the alloy and temper
  • Keep holes away from bend deformation zones
  • Identify burr direction when assembly or safety matters
  • Avoid unnecessary flatness across heavily formed parts
  • Define functional tolerances separately from general dimensions

Volume and Break-Even Analysis

Compare annual volume, expected product life, tool cost, material utilization, press rate, labor, maintenance, scrap, and secondary operations. A low stamped piece price does not justify a tool if demand may disappear before payback.

  • Model conservative and expected demand
  • Include tool modifications and spare details
  • Account for coil scrap and startup scrap
  • Compare bridge and backup processes
  • Review design-change risk before approval

Tooling, Sensors, and Maintenance

Progressive tools include punches, dies, pilots, lifters, strippers, guides, and forming inserts. Sensors can detect feed errors, part ejection, buckle, or stock position. Preventive maintenance protects dimensional stability and avoids damage that can affect every station.

Quality Planning

Inspection should focus on dimensions that can drift through punch wear, springback, strip feed, and material variation. Optical inspection, gauges, CMM checks, and in-die monitoring may be combined depending on risk.

  • Approve strip and finished-part samples
  • Track tool wear on critical punches
  • Control coil width, thickness, hardness, and grain
  • Use capability studies for key dimensions
  • Define reaction plans for sensor alarms

Alternatives to Progressive Stamping

Laser cutting and press-brake forming suit prototypes and changing designs. CNC machining suits thick or three-dimensional precision parts. Compound or transfer dies may fit different geometries and volumes. A staged route can use soft tooling before progressive production.

Frequently Asked Questions

What volume justifies a progressive die?

There is no universal threshold. Calculate payback using tool cost, expected lifetime demand, unit savings, scrap, maintenance, and design-change risk.

Can tight tolerances be stamped?

Yes for selected features with appropriate tool design and process control, but CNC-level tolerances everywhere can make the tool unnecessarily complex and expensive.

Can a progressive stamped part be machined afterward?

Yes. Secondary CNC operations can add precision holes, threads, flat sealing faces, or interfaces that are not economical to hold in the die.
Related MTSPi CNC Resources

Categories
Manufacturing Process Comparisons

CNC Machining vs Stamping: Which Process Wins for Your Project?

Choosing between CNC machining and stamping is a common manufacturing crossroads. This guide breaks down their core differences in cost, precision, and application to help you decide which fabrication process is the winner for your specific project needs.

Understanding the Basics: What Are We Comparing?

When you’re planning a new part, you’ll likely hear about CNC machining services and metal stamping processes. They’re both fantastic, but they work in completely different ways. Think of it like cooking: one is a meticulous chef carving a sculpture from a block of material (CNC), and the other is a high-speed cookie cutter pressing shapes out of sheet metal (stamping). Let’s get to know each one a bit better.

What is CNC Machining?

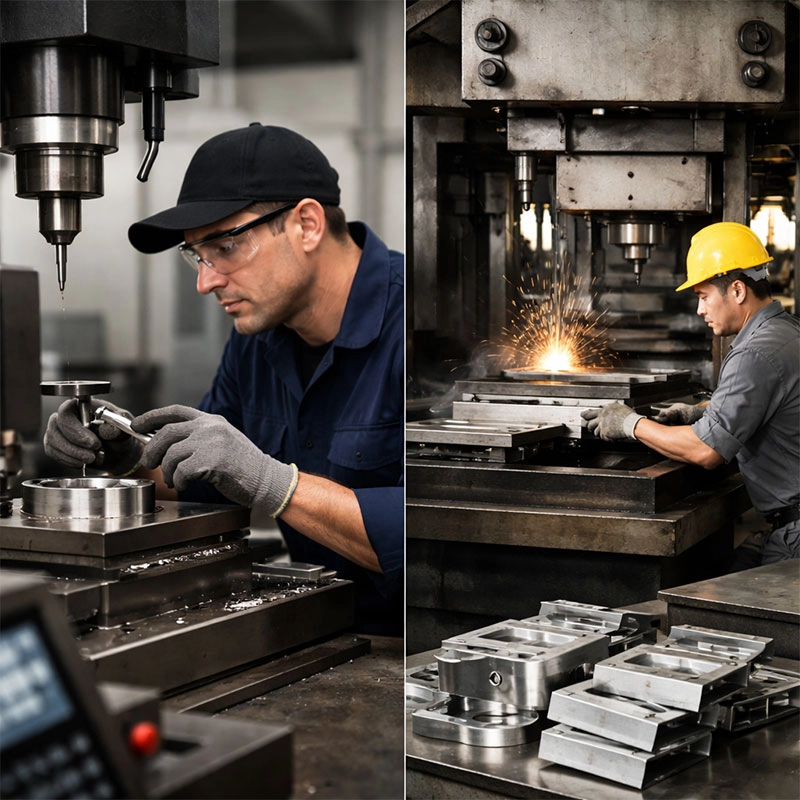
CNC, or Computer Numerical Control machining, is a subtractive manufacturing process. It starts with a solid block of material—like metal, plastic, or even wood—and uses computer-controlled cutting tools to remove material, carving out the final part. It’s incredibly precise and is perfect for creating complex, three-dimensional geometries. If you’re looking into precision machining for prototypes or low-volume custom parts, this is often the go-to method.

What is Metal Stamping?

Metal stamping, on the other hand, is a forming process. It uses a stamping press and a set of custom dies (like a specialized mold) to punch, bend, or shape sheet metal into a desired form. The key here is the die. Creating it is a significant upfront investment, but once it’s made, you can produce parts at lightning speed. This makes stamping ideal for high-volume sheet metal fabrication of components like brackets, enclosures, or automotive parts.

Head-to-Head Comparison: Where Each Process Shines

Now that we know the players, let’s put them side-by-side. This isn’t about which one is “better,” but about which one is better *for you*. I often tell my clients that the choice between CNC milling vs stamping comes down to a few key project factors.

Cost and Production Volume

This is the biggest deciding factor for most projects. CNC machining has low startup costs—you just need the digital file. But, the cost per part remains relatively high. Stamping has very high initial costs due to die creation, but the cost per part plummets as you make more. So, the rule of thumb is: low-volume production favors CNC, while high-volume manufacturing is where stamping wins on economics. For a deep dive on manufacturing economics, the Modern Machine Shop has a great resource on cost drivers.

Material and Design Flexibility

CNC is the clear champion here. It can handle a vast range of materials, from aluminum and stainless steel to engineering plastics. You can make incredibly complex parts with undercuts, deep cavities, and fine details. Stamping is primarily for ductile metals (like steel, aluminum, copper) and is best for parts with a relatively uniform thickness. Changing a design with CNC is as simple as tweaking the CAD file. With stamping, a design change often means a new, expensive die.

Precision and Surface Finish

Both can be precise, but in different ways. CNC machining typically offers tighter tolerances and superior surface finishes right off the machine. It’s the choice for parts that must fit together perfectly or have a cosmetic finish. Stamped parts can be very precise, but the precision is built into the die. The surface might have marks from the forming process and often requires secondary operations. For applications demanding the utmost accuracy, CNC turning and milling usually takes the lead.

Speed and Lead Time

For getting a first part in your hands quickly, CNC wins. There’s no tooling wait time. For mass production, however, nothing beats the sheer speed of a stamping press once it’s running. So, consider your timeline: need a prototype next week? CNC. Need a million parts over the next year? Stamping’s production rate is unbeatable.

Making the Right Choice for Your Project

So, which process wins? It depends entirely on your project’s recipe. Here’s a simple way to think about it:

Choose CNC Machining if your project involves: – Low to medium volumes (prototypes, custom parts, batches of 1-10,000). – Complex 3D geometries, tight tolerances, or excellent surface finish. – Frequent design changes or a wide variety of materials. – You need parts fast for testing or initial production.

Choose Metal Stamping (or progressive die stamping) if your project involves: – Very high volumes (tens of thousands to millions of parts). – Relatively simple, flat or bent parts made from sheet metal. – A finalized design where the cost of the die can be amortized. – The primary goal is the lowest possible cost per part at high speed.

Sometimes, the best solution uses both! A common approach is to use CNC to prototype and test a part, then transition to stamping for the full production run once the design is locked in. The team at ASM International’s handbook on metalworking discusses these hybrid manufacturing strategies. My advice? Start by clearly defining your volume, budget, timeline, and part complexity. With those in hand, the winning process for your custom part fabrication will become much clearer.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

CNC Machining vs Stamping: Which Process Wins for Your Project?

We'll Send You Back with Price Immediately!