

Categories
Blog CNC Materials Quality & Tolerances

Is Nickel Magnetic? What CNC Buyers Should Know

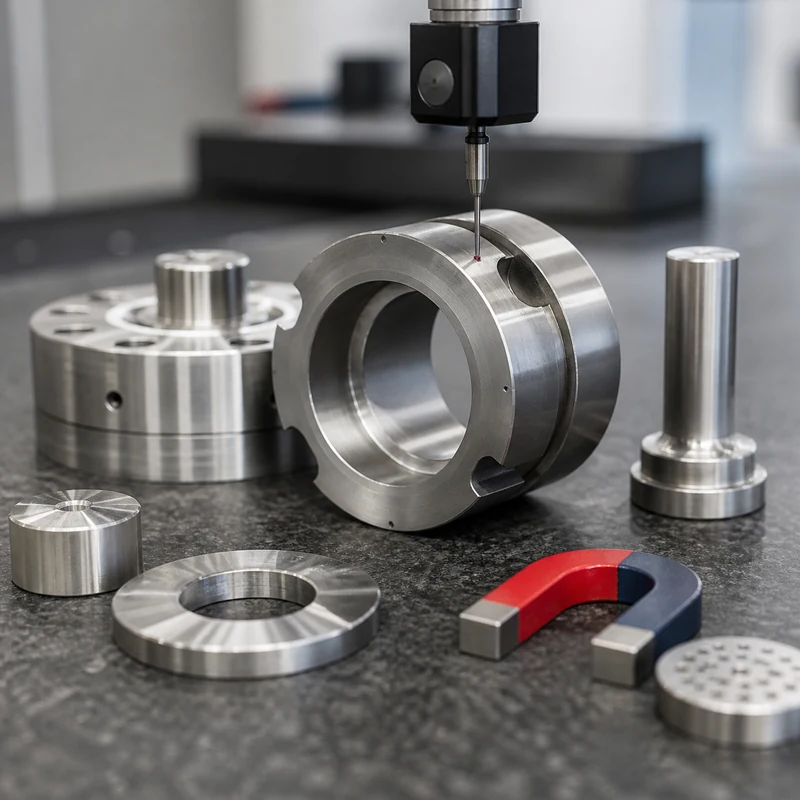
Pure nickel is one of the common engineering metals that can respond to a magnet. That simple answer is useful, but it is not enough for machined-part purchasing because most real projects use nickel alloys, plated surfaces, or stainless and high-temperature alloys that contain nickel in different amounts.

For CNC buyers, magnetic behavior should be treated as a material requirement in the same way as hardness, corrosion resistance, surface finish, and tolerance. MTSPi reviews these details together with CNC material options and the intended application before selecting a practical machining route.

Short Answer: Pure Nickel Is Magnetic

Pure nickel is ferromagnetic at normal room temperature. It can be attracted by a magnet because its internal magnetic domains can align under a magnetic field. Its response is usually weaker than iron, and it changes when nickel is alloyed with other elements.

Material or alloy family Typical magnetic response CNC buyer note
Pure nickel Magnetic Confirm whether magnetic response is acceptable near sensors or electronic assemblies.
Nickel-copper alloys Usually low to moderate Composition and processing history matter.
Nickel-chromium alloys Often weak or nearly non-magnetic Useful where corrosion and heat resistance are more important than magnetism.
Austenitic stainless steel Usually non-magnetic or weakly magnetic Cold working or machining can increase local response.

Why Nickel Alloy Magnetism Varies

A material name alone rarely tells the whole story. Alloying additions, crystal structure, cold work, heat treatment, and service temperature all affect magnetic behavior. Two parts with similar nickel content can react differently if one has been heavily worked or heat treated.

This is why the drawing should state any magnetic requirement directly. If the part will sit near magnetic sensors, motors, instruments, or sensitive electronics, include that condition in the RFQ along with dimensions and finish. MTSPi can review it during drawing review before machining starts.

Temperature and the Curie Point

Nickel loses its ferromagnetic behavior when heated above its Curie temperature, about 358 C. Below that point, pure nickel can remain magnetic. Above it, the magnetic domains no longer align in the same way. For high-temperature equipment, this property should be checked against the real operating temperature rather than assumed from room-temperature behavior.

Machining Considerations for Nickel Materials

Nickel and many nickel alloys can be demanding to machine because they may work harden, retain heat, and wear tools quickly. Good process planning matters as much as material selection. Depending on the geometry, MTSPi may compare CNC milling service with CNC turning service or use a mixed process for features that need stable datums.

Practical controls include sharp tooling, correct cutting parameters, rigid workholding, suitable coolant, and inspection after critical operations. Surface damage, burrs, and residual stress can affect both function and cosmetic finish, so deburring and finishing should not be left until the last minute.

When Magnetic Behavior Should Be Specified

Application condition Why it matters What to tell the supplier
Sensor housings Magnetic response can affect readings State allowable magnetic behavior and test method.
Medical or laboratory tools Equipment may operate near magnets or instruments Confirm material grade and inspection expectations.
Aerospace or electronics fixtures Magnetic attraction may interfere with assembly or service Share operating environment and certification needs.
General mechanical parts Magnetism may not affect function Do not over-specify if it adds cost without benefit.

Inspection and Documentation

If magnetism is a functional requirement, define how it will be verified. A casual magnet check is not the same as a controlled inspection plan. Buyers can combine material certificates, dimensional reports, and special checks through CNC machining quality inspection when the application requires traceability.

The best specification is clear enough for quoting, machining, and receiving inspection. It should name the material grade, finish, tolerance, operating temperature, and any magnetic limits that affect the assembly.

Conclusion

Nickel is magnetic in pure form, but CNC projects usually require a more specific answer. Alloy composition, manufacturing route, temperature, and inspection requirements determine whether magnetic behavior matters. Treat it as an engineering requirement, not a trivia fact, and include it in the drawing package when it can affect performance.
Categories
CNC Machining Basics

Master Machining Heat-Resistant Alloys: 5 Expert Tips for Success

Working with heat-resistant superalloys can feel like a tough challenge for any CNC shop. These materials are incredibly strong at high temperatures, but that same strength makes them difficult to machine. This guide breaks down the process into five practical, expert-backed tips to help you achieve better finishes, longer tool life, and greater success on your next job.

Understanding the Challenge

Before we dive into the tips, let’s get on the same page about what we’re dealing with. When we talk about machining high-temperature alloys like Inconel, Hastelloy, or Waspaloy, we’re facing a unique set of obstacles. It’s not just harder steel; it’s a different ball game. I like to think of it as trying to carve a piece of hardened gum—it’s gummy, it work-hardens quickly, and it loves to eat cutting tools for breakfast. Successfully processing heat-resistant superalloys starts with respecting these inherent properties.

What Makes Them So Tough?

The main hurdles come down to three things: incredible strength at elevated temperatures, a tendency to work-harden, and low thermal conductivity. While their ability to retain strength under heat is why they’re used in jet engines and turbines, it means they resist cutting forces fiercely. The low thermal conductivity is a double-edged sword; instead of the heat flowing into the chip, it stays concentrated at the cutting edge, accelerating tool wear. Understanding this is the first step to choosing the right strategy.

Tip 1: Master Your Tool Selection

This is arguably the most critical step. Using the wrong tool is a fast track to frustration and wasted money. For cutting refractory metals and superalloys, you need tools that are as tough as the material itself. We strongly recommend premium-grade carbide inserts with specialized coatings. Look for grades designed for high-temperature alloys, often with a tough substrate and a PVD (Physical Vapor Deposition) coating like AlTiN. These coatings provide excellent heat resistance and lubricity. For some operations, especially finishing, you might explore CBN (Cubic Boron Nitride) tools. They’re more expensive but can be game-changers for achieving fine surface finishes on hardened alloys. A great resource for understanding advanced tool materials is the ASM International website.

Tip 2: Dial in Your Cutting Parameters

Forget the speeds and feeds you use for aluminum or mild steel. With nickel-based superalloy machining, the rules change. The golden rule here is to maintain a consistent, controlled chip load to manage heat and prevent work hardening. We suggest starting with a lower surface speed (SFM) than you initially think, but with a moderately high feed rate. This creates thicker chips that carry away heat more effectively. A light depth of cut can often lead to more rubbing and heat generation, so don’t be afraid to take a more substantial, but controlled, cut. It’s all about finding that sweet spot where the tool is working efficiently without overheating.

Tip 3: Prioritize Rigidity and Cooling

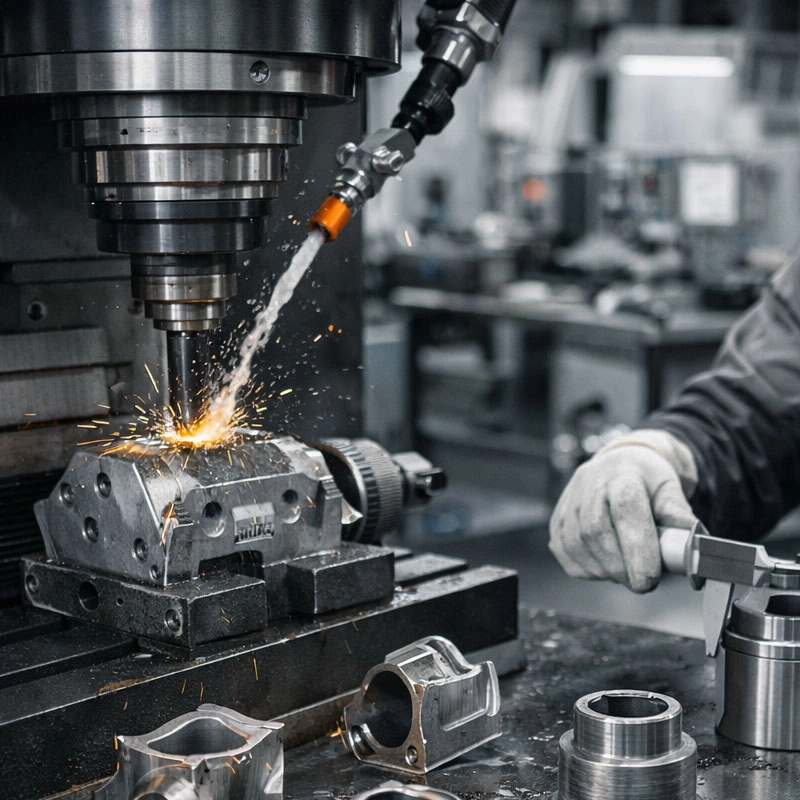
Any chatter or vibration is your enemy when fabricating with high-performance alloys. Ensure your workpiece is clamped as securely as possible using sturdy vises, fixtures, or even custom workholding. Next, let’s talk coolant. This isn’t optional; it’s essential. Use a high-quality, high-pressure coolant system aimed directly at the cutting zone. The goal is twofold: to remove heat and to help evacuate chips. Flood coolant is good, but through-tool coolant is even better as it gets right to the heart of the heat. Proper chip evacuation is crucial, as recutting chips is a surefire way to ruin your insert and your part finish.

Tip 4: Optimize Your Toolpaths and Strategy

How you move the tool is just as important as the tool itself. Modern CAM software offers powerful strategies for tough materials. For roughing, consider trochoidal or high-efficiency milling paths. These use a constant engagement angle, which provides a smoother, cooler cut compared to traditional zig-zag patterns that can shock the tool. When finishing, use climb milling to ensure the chip is thickest at the start and thin at the end, promoting a cleaner shear. Always program a lead-in and lead-out arc to avoid dwell marks. Think of your toolpath as a roadmap for managing stress on both the tool and the material.

Tip 5: Don’t Skimp on Inspection and Machine Care

This final tip is about diligence. Superalloy component manufacturing is precise work. Implement in-process checks to catch any deviation early, especially since these materials are so costly. Regularly check your tool for wear—don’t wait for it to fail completely. A slightly worn tool in a superalloy can quickly lead to work hardening on the part surface. Furthermore, keep your machine tool in top condition. Check for spindle runout and ensure way covers are clean. A well-maintained machine provides the stable platform you need for success. For official standards on material properties and testing, the ASTM International portal is an authoritative reference.

Wrapping It Up: Your Path to Success

Tackling heat resistant alloy fabrication doesn’t have to be a nightmare. By focusing on these five pillars—selecting the right tools, dialing in conservative but effective parameters, ensuring rock-solid rigidity and cooling, using smart toolpaths, and maintaining rigorous inspection habits—you’ll turn a daunting job into a repeatable process. Start by applying one or two of these tips to your next project. You’ll likely notice an improvement in tool life and part quality, giving you the confidence to master even the toughest alloys on your CNC floor. Happy machining!

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

Master Machining Heat-Resistant Alloys: 5 Expert Tips for Success

We'll Send You Back with Price Immediately!