Categories
Blog CNC Machining Basics Quality & Tolerances

What Is a Micrometer? Precision Measurement for CNC Machined Parts

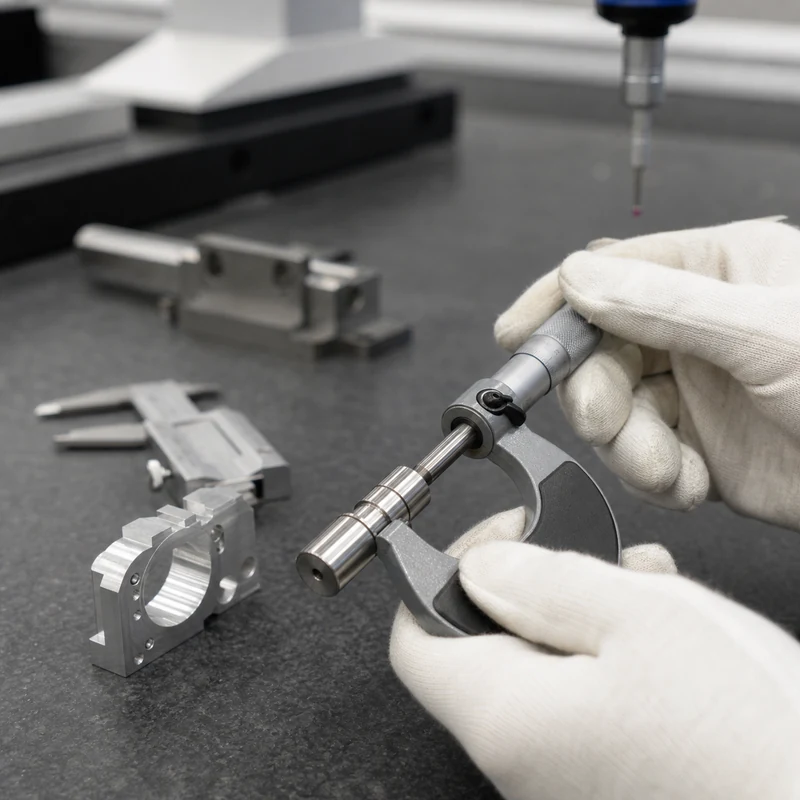
A micrometer is a precision measuring tool used to check small dimensions such as outside diameter, thickness, step height, groove width, and depth. In CNC machining, it is often used for fast, repeatable checks on features that need tighter control than a basic ruler or many general-purpose caliper checks can provide.

Micrometers are important because CNC parts are judged by measurable dimensions, not appearance alone. A shaft may look correct but still fail if its diameter, roundness, or fit tolerance is outside the drawing requirement. MTSPi combines micrometer checks with CNC machining quality inspection, CMM inspection, gauges, and documented quality procedures.

How a Micrometer Works

Most micrometers use a precision screw mechanism. As the thimble turns, the spindle moves toward or away from the anvil by a known distance. The part is placed between the anvil and spindle, and the scale or digital display shows the measured dimension.

Part of the Micrometer Function Inspection Note
Frame Holds the anvil and spindle in alignment A rigid frame helps reduce measurement error
Anvil Fixed measuring face Must be clean and free of burrs
Spindle Moving measuring face Should contact the part with controlled force
Sleeve and thimble Mechanical scale used to read the measurement Requires correct reading technique
Ratchet or friction stop Applies consistent measuring pressure Helps different inspectors get similar results
Lock Holds the spindle position Useful when recording or comparing a reading

Common Types of Micrometers

Micrometer Type Typical Use Example CNC Part Feature
Outside micrometer External diameters and thicknesses Turned shafts, plates, bosses, spacers
Inside micrometer Internal widths and larger bore sizes Housings, slots, internal steps
Depth micrometer Depths of holes, pockets, grooves, and shoulders Milled pockets and blind holes
Blade micrometer Narrow grooves and recessed features Thin slots or retaining-ring grooves
Point micrometer Small grooves or difficult contact areas Fine turned details
Digital micrometer Fast reading and data capture Production inspection and operator checks

Micrometer Accuracy and Resolution

A micrometer is commonly available with fine resolution, but resolution is not the same as total measurement accuracy. Accuracy depends on calibration, operator technique, temperature, tool condition, part cleanliness, and whether the measuring faces contact the intended feature correctly.

  • A clean measuring surface prevents chips or oil from creating a false reading.
  • Consistent ratchet force reduces operator-to-operator variation.
  • Temperature matters because both the part and the tool can expand or contract.
  • Calibration records are needed when measurements support formal quality documentation.

How Micrometers Are Used in CNC Machining

Machinists and inspectors often use micrometers at three stages: incoming material checks, in-process checks, and final inspection. The tool is fast enough for shop-floor use but precise enough to help control critical dimensions.

Incoming Material Checks

Before machining starts, a micrometer can verify bar diameter, plate thickness, stock condition, or pre-machined blanks. This prevents a job from starting with material that cannot clean up to the final dimension.

In-Process Inspection

During machining, micrometers help operators confirm whether tool wear, thermal drift, offsets, or workholding movement are affecting critical features. Early checks reduce scrap because corrections can be made before the entire batch is finished.

Final Inspection

After machining, micrometer measurements may be recorded with other inspection results. For complex geometry, micrometers are usually paired with CMM inspection, bore gauges, thread gauges, height gauges, surface roughness checks, or functional gauges.

Micrometer vs Caliper

Tool Strength Limitation
Micrometer Higher repeatability for specific external, internal, or depth measurements Less versatile; each type covers a narrower measurement range
Caliper Fast general measurements across many feature types Usually less repeatable for very tight tolerances

A caliper is useful for quick checks and general dimensions. A micrometer is preferred when the feature has tighter tolerance, when repeatability matters, or when the contact geometry of the tool better matches the measured feature.

Best Practices for Reliable Micrometer Readings

  • Clean the part and measuring faces before every critical reading.
  • Use the ratchet or friction stop instead of squeezing the part by hand pressure.
  • Measure at multiple positions when checking round parts for taper or out-of-round conditions.
  • Let precision parts stabilize near inspection temperature before final measurement.
  • Store micrometers in a clean case and keep calibration records current.
  • Use the correct micrometer type and range for the feature being inspected.

Where Micrometers Fit in a Quality System

Micrometers are only one part of a complete inspection plan. MTSPi uses them alongside calipers, CMM inspection, thread gauges, pin gauges, visual checks, surface finish checks, and documented process controls. The right inspection method depends on the feature function, tolerance, drawing requirement, and production risk. Learn more on our quality assurance page.

Typical CNC Features Checked With Micrometers

Feature Common Tool What to Watch
Shaft diameter Outside micrometer Check several positions for taper or ovality
Plate thickness Outside micrometer Avoid chips, burrs, and clamping marks
Groove depth Depth or blade micrometer Confirm contact surfaces match the drawing reference
Small step height Depth micrometer Verify datum surface cleanliness
Bore-related features Inside micrometer or bore gauge Confirm the tool is suitable for the bore size and tolerance

How MTSPi Controls Precision Measurements

For custom CNC machining projects, MTSPi reviews the drawing before production to identify critical dimensions, inspection methods, and reporting needs. For tight tolerance parts, we combine stable machining processes with in-process checks and final inspection records. Related services include CNC milling, CNC turning, 5-axis machining, and surface treatment.

Related MTSPi Resources

FAQ

What is a micrometer used for in CNC machining?

A micrometer is used to measure critical dimensions such as shaft diameters, part thicknesses, step heights, grooves, and other features that require repeatable precision checks.

Is a micrometer more accurate than a caliper?

For many tight-tolerance features, yes. A micrometer usually provides better repeatability for a specific measurement, while a caliper is more versatile for general checking.

How often should a micrometer be calibrated?

Calibration frequency depends on usage, required accuracy, quality procedures, and inspection risk. In professional machining environments, micrometers should be checked and calibrated on a defined schedule.
Categories
Blog CNC Machining Basics Design, Cost & Sourcing

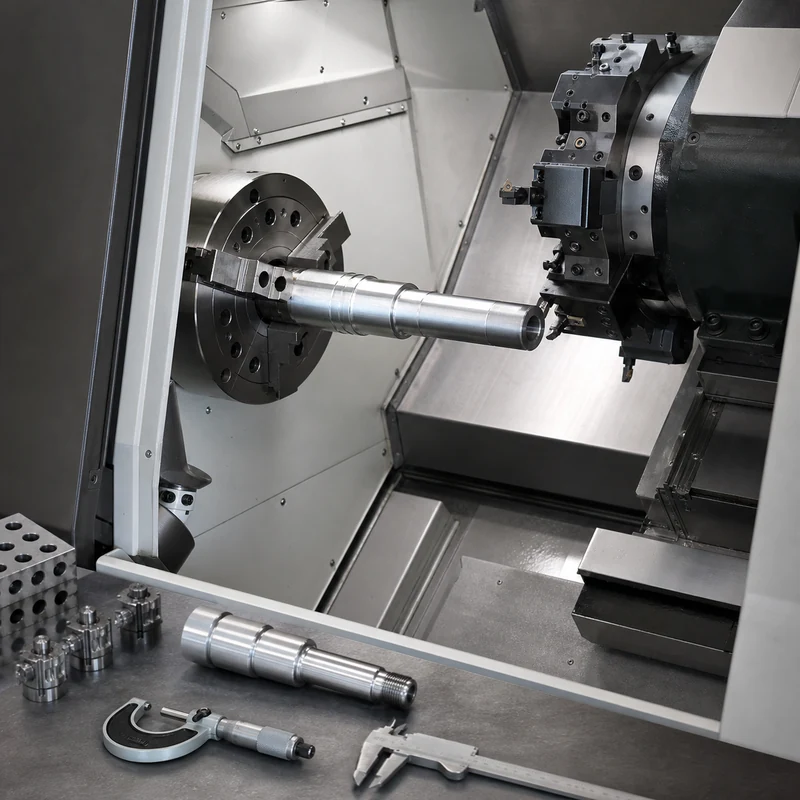
CNC Turning Center Specifications: Axes, Capacity, Tooling, Accuracy, and Buyer Notes

Quick answer: CNC turning center specifications describe what size, shape, material, accuracy, and features a lathe can produce. Important specs include chuck size, bar capacity, maximum turning diameter, turning length, spindle speed, turret tooling, live tooling, axes, and tolerance capability.

CNC Turning Center Specifications

A turning center is selected based on the part, not only on machine size. Shaft length, diameter, bore depth, thread type, groove position, live-milled features, material, and batch quantity all influence the best machine choice.

Key Points for Buyers and Engineers

Topic What to know Practical impact
Chuck size Workholding capacity for blanks Affects maximum part size.
Bar capacity Maximum bar diameter through spindle Important for production turned parts.
Turning length Maximum practical part length Controls shaft and sleeve feasibility.
Live tooling Milling/drilling tools on lathe Useful for cross holes, flats, and slots.
Axes X/Z plus C/Y or sub-spindle options Reduces secondary operations for complex parts.

How This Affects CNC Machined Parts

Turning centers are used for shafts, bushings, pins, sleeves, spacers, threaded parts, and round precision components. Review MTSPi’s CNC turning service for process fit.

Design and Purchasing Checklist

  • Provide maximum diameter and overall length.
  • Identify cross holes, flats, slots, and off-center features.
  • Confirm material, heat treatment, and finish.
  • Mark thread standards and inspection requirements.
  • Ask whether live tooling or secondary milling is needed.

Related MTSPi Resources

FAQ

What is a CNC turning center?

It is a CNC lathe that machines rotating workpieces and may include a turret, live tooling, sub-spindle, or additional axes.

What parts are made on turning centers?

Shafts, pins, bushings, sleeves, spacers, threaded fittings, and many round components.

What is live tooling?

Live tooling allows milling, drilling, or tapping operations on a turning center without moving the part to a separate mill.

Need help with CNC turning center part review?

Send drawings, material, quantity, finish, tolerance notes, and application requirements. MTSPi can review manufacturability before quoting.

Contact MTSPi for engineering and quote support

Practical Buyer Notes

Turning center specification pages should explain how machine specs affect real parts. Chuck size, bar capacity, turning length, spindle bore, turret stations, live tooling, and sub-spindle options all change what can be made efficiently.

Buyers usually do not need every machine parameter. They need to know whether their part diameter, length, material, thread, bore, cross holes, and tolerance fit the supplier’s turning capability.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Part diameter Check chuck size and turning diameter Determines whether the blank can be held and machined
Bar-fed production Check bar capacity Important for repeated small turned parts
Cross features Look for live tooling or secondary milling Reduces extra setups
Long shafts Review length, support, and runout control Prevents deflection and poor concentricity

Common Mistakes to Avoid

  • Selecting a turning supplier based only on maximum diameter.
  • Ignoring cross holes, flats, slots, and off-center features.
  • Forgetting to define thread standards and gauges.
  • Not discussing runout, concentricity, or surface finish for rotating parts.

Recommended MTSPi Review Workflow

MTSPi should review turned parts by diameter, length, material, features, tolerance, and quantity. This determines whether standard turning, Swiss-type machining, mill-turn, or secondary milling is best.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send the drawing with diameter, length, bore, thread, groove, surface finish, material, quantity, and any runout or concentricity requirements.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Deeper Engineering Notes

For CNC turning center specifications, the strongest page is not just a definition. It should help a buyer decide what information belongs on the drawing, what questions to ask a supplier, and which details affect cost, quality, and delivery. In real RFQ work, the important details are usually bar capacity, chuck size, turning length, live tooling, sub-spindle use, runout, and concentricity. These details decide whether the supplier can quote confidently or has to return with repeated questions.

The common risk is ignoring cross holes, flats, slots, and secondary features when choosing a turning supplier. That risk can make the content look complete on the surface but weak in a real manufacturing situation. A stronger specification connects the topic to material behavior, machine access, tolerance control, finishing, and inspection before the order is released.

Example Specification Review

Review area Question to answer Good specification practice
Function What does this feature or part need to do? Describe the load, fit, motion, appearance, sealing, or assembly requirement.
Material Is the selected material suitable for the environment? Confirm strength, heat, corrosion, wear, chemical exposure, and cosmetic needs.
Geometry Can the feature be reached by standard tools? Review depth, corner radius, wall thickness, tool clearance, and setup direction.
Tolerance Which dimensions are truly critical? Use tight tolerances only where function requires them and keep general dimensions practical.
Verification How will acceptance be checked? Define gauges, CMM checks, roughness measurement, thread inspection, or visual standards when needed.

How This Page Should Support Ranking

This topic can attract both beginner searches and buyer searches. The beginner wants a clear answer; the buyer wants enough detail to make a manufacturing decision. A page has a better chance to rank when it answers the simple question first, then adds examples, process limits, design notes, comparison tables, and practical next steps.

That is also why internal links should be helpful rather than forced. A reader should naturally move from this page to a process page, material page, surface finish page, inspection page, or quote page only when that next step solves a real question.

Conclusion

Turning center specifications matter because they determine whether a part can be made efficiently in one setup. Clear drawings help the supplier choose the right turning route.

Categories
Blog CNC Machining Basics Industries & Applications

What Can You Make With a CNC Machine? Parts, Products, and Applications

CNC machines can make a wide range of products, from simple plates and brackets to precision housings, shafts, heat sinks, fixtures, molds, connectors, robotic parts, and medical or aerospace components. The same core idea applies across all of them: a digital toolpath controls a cutting process so the finished part matches the model and drawing.

The best CNC product is not defined only by shape. It also depends on material, tolerance, surface finish, quantity, inspection level, and how the part will be assembled. MTSPi supports custom machined parts through CNC machined products, material planning, and production-oriented quality control.

Examples of CNC-Made Products

Product Type Examples Common Process
Structural parts Brackets, plates, frames, mounting blocks, machine bases 3-axis milling, 4-axis milling, 5-axis machining
Rotational parts Shafts, bushings, spacers, collars, rollers, pins CNC turning, Swiss-type machining, mill-turn
Enclosures and housings Sensor housings, electronics cases, motor covers, valve bodies Milling, drilling, tapping, boring
Thermal parts Heat sinks, cold plates, cooling blocks, finned components Milling, drilling, surface finishing
Tooling and fixtures Inspection fixtures, assembly jigs, soft jaws, nests, gauges Milling, turning, grinding-ready machining
Molds and dies Mold inserts, cavities, cores, die details 3-axis and 5-axis milling
Decorative or functional panels Nameplates, engraved plates, dashboard panels, prototypes Milling, engraving, finishing

Parts by Industry

Aerospace and drones

CNC machining can produce lightweight brackets, sensor mounts, landing gear parts, housings, antenna components, and structural frames. Aluminum and titanium are common because weight and strength matter.

Medical and life science

Medical projects often use stainless steel, titanium, aluminum, and engineering plastics for instrument components, housings, fixtures, and test hardware. Inspection, material control, and finish quality are especially important.

Robotics and automation

Robots need accurate joints, grippers, end-effectors, actuator housings, bearing blocks, shafts, sensor mounts, and lightweight plates. CNC machining is useful because fit and repeatability affect motion performance.

Electronics and semiconductor equipment

CNC machines can make enclosures, heat sinks, vacuum-compatible components, connector blocks, precision plates, and fixture hardware for electronics and semiconductor workflows.

Materials Used for CNC Products

  • Aluminum for lightweight prototypes, housings, brackets, and heat sinks.
  • Stainless steel for corrosion-resistant and durable components.
  • Brass and copper for fittings, contacts, thermal parts, and electrical components.
  • PEEK, POM, nylon, ABS, PC, and acrylic for insulated, lightweight, or low-friction parts.

What Cannot Be Made Efficiently With CNC?

CNC machining is not always the best answer. Thin sheet-metal parts may be better suited to laser cutting and bending. Very high-volume plastic parts may justify injection molding. Extremely large cast shapes may need casting first, followed by CNC finishing. The right process depends on geometry, volume, material, and cost target.

Design Tips for CNC-Made Products

  • Use realistic internal radii instead of sharp inside corners.
  • Avoid very deep narrow pockets unless they are functionally necessary.
  • Specify only the tolerances that affect fit, motion, sealing, or inspection.
  • Choose finishes early because anodizing, plating, polishing, and coating change dimensions and appearance.
  • Include drawings for threads, critical dimensions, flatness, surface roughness, and inspection notes.

From Idea to Finished Part

A typical project starts with CAD files and a drawing, then moves through manufacturability review, material selection, machining strategy, finishing, inspection, and shipment. For early-stage designs, rapid prototyping helps test fit and function before committing to a larger production run.

Related MTSPi Resources

FAQ

Can a CNC machine make finished products?

Yes. CNC machines can make finished components and, in some cases, complete products. Many projects still require secondary operations such as finishing, assembly, marking, or inspection.

Is CNC better for metal or plastic parts?

CNC works well for both. The best material depends on strength, weight, temperature, friction, chemical exposure, appearance, and cost.

Categories
Blog CNC Machining Basics Industries & Applications

What Is a CNC Machine Used For? Applications, Parts, and Manufacturing Examples

Quick answer: A CNC machine is used to cut, drill, turn, mill, engrave, tap, and shape metal or plastic parts with computer-controlled motion. It is commonly used for prototypes, production parts, fixtures, housings, shafts, brackets, molds, tooling, and precision components.

Common Uses of CNC Machines

CNC machines are used anywhere a part needs repeatable dimensions, controlled surfaces, accurate holes, or consistent production quality. The same basic technology can make a single prototype, a replacement component, or a batch of production parts.

Use Typical parts Best machine route
Prototypes Test housings, brackets, plates, adapters, fixtures CNC milling or turning
Machinery components Shafts, bushings, mounts, plates, tooling blocks Milling, turning, drilling
Aerospace and robotics Lightweight brackets, structural parts, precision interfaces Milling and multi-axis machining
Medical and electronics Small housings, connectors, fixtures, instrument components Precision milling and inspection
Maintenance parts Custom spacers, repair parts, replacement pins, covers Turning, milling, fast turnaround machining

Why Manufacturers Use CNC Instead of Manual Machining

Manual machining depends heavily on operator control. CNC machining uses programmed motion, making it better for repeatability, complex geometry, documented setups, and consistent batches. Manual work still has value for simple repairs, but CNC is stronger when repeatable production or tight drawing control is needed.

What Materials Can CNC Machines Cut?

CNC machines can cut many machining materials, including aluminum, stainless steel, carbon steel, brass, copper, titanium, ABS, POM, nylon, acrylic, PC, and PEEK. Aluminum is common for prototypes and lightweight parts, while stainless steel is selected for strength and corrosion resistance.

Which CNC Process Fits Which Part?

Flat, block-like, pocketed, or bracket-style parts usually fit CNC milling. Round parts such as shafts, pins, spacers, threaded sleeves, and bushings usually fit CNC turning. Parts with both round and milled features may require combined operations.

Industries That Use CNC Machines

  • Automation equipment and robotics
  • Automotive and electric vehicle hardware
  • Aerospace prototypes and lightweight structural parts
  • Medical devices, test fixtures, and instrument components
  • Electronics enclosures, heat sinks, and connectors
  • Industrial machinery, packaging equipment, and tooling

How to Decide If CNC Is Right for Your Part

CNC is a strong choice when you need real material properties, accurate dimensions, functional testing, low-volume production, or a part that cannot be easily molded without tooling. If the design needs very organic geometry or internal channels, 3D printing may be worth comparing.

FAQ

Can a CNC machine make one part?

Yes. CNC machining is often used for one-off prototypes, custom replacement parts, and short-run production.

Can CNC machines make plastic parts?

Yes. CNC machining is common for ABS, POM, nylon, acrylic, PC, PEEK, and other engineering plastics.

What is the difference between CNC milling and CNC turning?

Milling uses rotating cutting tools against a fixed workpiece, while turning rotates the workpiece against cutting tools.

Are CNC machines used for mass production?

Yes, but the economics depend on part geometry, cycle time, fixture design, material, and quantity.

Need help choosing a machining route?

Send MTSPi your drawing, material, quantity, finish, and inspection requirements. We will review the part for manufacturability before quoting.

Contact MTSPi for a CNC machining quote

Practical Buyer Notes

When buyers ask what a CNC machine is used for, the real question is usually whether CNC is the right manufacturing route for a specific part. CNC is strongest when the part needs real engineering material, controlled dimensions, repeatable features, and faster development than mold tooling.

For sourcing decisions, separate prototype use from production use. A prototype may focus on fit and function, while a production order must also consider cycle time, fixture repeatability, inspection method, packaging, and long-term cost stability.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Prototype or production Use CNC for real-material prototypes and low-volume production Avoids tooling cost while keeping functional material properties
Part geometry Match flat parts to milling and round parts to turning The right route lowers setup time and improves accuracy
Assembly risk Mark mating faces, holes, threads, and datums These features usually decide whether the part works
Finish requirement Define cosmetic and protective finishes early Finishing can change appearance, lead time, and dimensions

Common Mistakes to Avoid

  • Treating CNC as one single process instead of choosing milling, turning, drilling, or multi-axis machining.
  • Asking for tight tolerances on every dimension instead of only functional features.
  • Choosing a material by name without checking strength, heat, corrosion, and finish needs.
  • Forgetting to define threads, inserts, cosmetic faces, and burr requirements.

Recommended MTSPi Review Workflow

For application-driven pages, MTSPi reviews the part by use case first, then chooses the machining route. This keeps the page useful for information searches and also helps real buyers understand the quoting path.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

A faster quote needs more than a screenshot or rough size. The best input package explains what the part does, how it assembles, which features are critical, and what finish or inspection level is required.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Conclusion

A CNC machine is used to turn digital designs into accurate physical parts. The best results come from matching the part shape to the right machining route, choosing a suitable material, and defining the important tolerances clearly before production.

Categories
Blog CNC Machining Basics Guides Manufacturing Process Comparisons Quality & Tolerances

DMLS Dense Metal Parts: Porosity, HIP, CNC Post-Processing, and Inspection

DMLS can build metal parts with impressive density, but dense does not mean simple. Metal powder quality, laser parameters, scan strategy, part orientation, support design, heat treatment, and inspection all affect the final result. For engineers, the real question is not only whether a part can be printed, but whether it can meet strength, fatigue, sealing, machining, and assembly requirements after printing.

This guide explains how Direct Metal Laser Sintering builds dense metal parts, what creates porosity, how post-processing improves performance, and when CNC machining should be used after printing. It complements MTSPi’s broader DMLS and CNC post-processing guide, but focuses specifically on density, voids, quality control, and functional metal part performance.

What Does Dense Mean in DMLS?

In DMLS, density describes how much of the part volume is solid metal compared with voids, pores, or incomplete fusion areas. A highly dense printed part has very little internal porosity. This matters because pores can reduce strength, fatigue life, pressure tightness, thermal conductivity, and confidence in critical applications.

Bulk density is sometimes reported as a percentage of theoretical density. However, a single number does not tell the whole story. The size, shape, location, and distribution of pores can matter as much as total pore volume. A few pores near a stressed surface or sealing feature may be more important than small isolated pores in a low-stress region.

How DMLS Builds Dense Metal Parts

DMLS uses a laser to fuse thin layers of metal powder. Each layer must melt or sinter consistently enough to bond with the previous layer and neighboring scan tracks. If laser energy is too low, powder may not fully fuse. If energy is too high, vaporization, spatter, or keyhole porosity can occur. Stable density depends on a balanced process window.

Process Factor How It Affects Density Engineering Note
Powder quality Particle size, shape, flowability, oxygen level, and contamination affect fusion Use qualified powder and controlled reuse practices
Laser power and speed Controls melt pool size and bonding between tracks Wrong energy can cause lack of fusion or keyhole pores
Layer thickness Affects resolution, build time, and fusion consistency Thinner layers may improve detail but increase time
Scan strategy Controls heat distribution and overlap Poor strategy can increase distortion or porosity
Shielding gas Limits oxidation and stabilizes the build atmosphere Gas flow and cleanliness matter
Part orientation Changes support needs, thermal behavior, and defect risk Orient parts with post-machining and inspection in mind

Common Types of Porosity

Not all pores have the same cause. Understanding the defect type helps engineers decide whether the issue is a process problem, design problem, material issue, or inspection requirement.

  • Lack-of-fusion porosity happens when powder or scan tracks do not bond completely.
  • Gas porosity can come from trapped gas inside powder particles or the melt pool.
  • Keyhole porosity can occur when excessive energy creates an unstable deep melt pool.
  • Contamination-related pores may appear when powder handling or atmosphere control is poor.
  • Surface-connected porosity may affect sealing, coating, fatigue, or machining results.

DMLS Density vs CNC Machined Metal

CNC machining starts from wrought, cast, forged, or extruded stock. Material density and internal quality depend on that stock form and material certification. DMLS builds the material at the same time it builds the shape, so density depends strongly on the build process. This is why DMLS parts usually need more process qualification than conventional custom CNC machining parts.

Comparison Point DMLS Metal Part CNC Machined Metal Part
Material formation Built layer by layer from powder Cut from existing billet, bar, plate, or casting
Internal defects Porosity and lack of fusion must be controlled Depends on stock quality, inclusions, casting voids, or forging quality
Geometry freedom Excellent for internal channels and lattices Limited by tool access and cutting geometry
Precision surfaces Often require post-machining Can be produced directly with suitable machining strategy
Certification focus Build parameters, powder, heat treatment, density, inspection Material certs, machining inspection, finish, heat treatment if required

Why Dense DMLS Parts Still Need Post-Processing

A dense printed part can still have rough surfaces, residual stress, support marks, dimensional variation, and features that are not accurate enough for assembly. Post-processing turns a good printed blank into a functional part. The exact sequence depends on material and application.

  • Stress relief reduces residual stress from rapid heating and cooling.
  • HIP can close some internal pores and improve fatigue performance for certain applications.
  • Support removal clears anchors and rough attachment areas.
  • CNC machining finishes datums, holes, threads, sealing faces, bearing seats, and flat surfaces.
  • Polishing, blasting, or coating controls surface finish and appearance.
  • Inspection confirms density, dimensions, and functional features.

HIP: Hot Isostatic Pressing and Density Improvement

Hot Isostatic Pressing, or HIP, uses high temperature and high pressure to reduce internal porosity in certain metal parts. It can improve fatigue life, ductility, and reliability when used correctly. HIP is common in aerospace, medical, and high-performance metal additive applications, but it is not a shortcut for poor printing practice.

Design teams should confirm whether HIP is required by the application, material, standard, or customer specification. After HIP, critical features may still need CNC machining because dimensional changes and surface requirements must be controlled.

CNC Machining After DMLS

CNC post-processing is often the practical bridge between additive geometry and precision assembly. DMLS may create an internal cooling channel, lightweight lattice, or complex bracket form, while 5-axis machining or precision milling finishes the surfaces that need to mate with other parts.

  • Machine datums first so later inspection has stable references.
  • Leave machining allowance on printed bosses, pads, holes, and sealing faces.
  • Avoid printing final precision holes unless the tolerance is loose.
  • Tap or thread-machine critical threads after printing.
  • Plan fixturing early because organic DMLS shapes can be hard to hold.
  • Use inspection data to confirm both printed and machined zones.

Design Tips for Dense DMLS Parts

A dense DMLS part starts with good design. If the part traps powder, overheats in thick sections, has unsupported overhangs, or leaves no allowance for machining, density alone will not make it successful.

  • Avoid unnecessary thick masses that create thermal gradients and long build times.
  • Use lattice structures only where they serve load, weight, airflow, or heat-transfer goals.
  • Add powder escape paths for internal cavities.
  • Design supports so they can be removed without damaging functional areas.
  • Separate as-printed surfaces from post-machined precision surfaces on the drawing.
  • Define density, porosity, and inspection requirements only where they matter.
  • Confirm whether the part needs heat treatment, HIP, or surface finishing.

Inspection Methods for Dense Metal Printed Parts

DMLS inspection can include dimensional checks, visual review, microscopy, density measurement, CT scanning, metallography, tensile coupons, hardness testing, and surface roughness measurement. For many projects, inspection should be matched to risk. A concept prototype may only need basic measurement. A pressure part, medical part, or aerospace bracket may need a much stronger quality assurance plan.

Inspection Method What It Checks When It Helps
Dimensional inspection Size, flatness, position, machined features Almost every functional part
CT scanning Internal pores, cracks, trapped powder, channels Complex or critical internal geometry
Metallography Microstructure, fusion quality, pores Process validation and high-risk parts
Tensile coupons Strength, elongation, material response Material qualification and critical builds
Surface roughness testing As-printed or machined surface condition Sealing, fatigue, flow, and cosmetic surfaces

Applications Where Density Matters

Density matters most when a part carries load, sees fatigue, holds pressure, transfers heat, or must pass strict validation. Examples include aerospace brackets, medical implants or instruments, heat exchangers, manifolds, tooling inserts with conformal cooling, lightweight robotic structures, and high-performance prototypes.

For less critical visual prototypes, density may be less important than appearance, geometry, and lead time. In those cases, polymer printing, CNC machining, or rapid prototyping with another process may be more practical.

When to Choose CNC Instead of DMLS

If a part is a simple bracket, plate, shaft, housing, or block with accessible features, CNC machining is usually the stronger first option. It typically offers better surface finish, tighter tolerances, broader material availability, and lower cost for conventional geometry. DMLS becomes more attractive when geometry complexity is doing real work.

For conventional metal parts, compare aluminum CNC machining, stainless steel CNC machining, titanium CNC machining, and other material options before committing to metal additive manufacturing.

How MTSPi Can Support Dense DMLS Projects

MTSPi focuses on CNC machining, rapid prototyping, materials guidance, surface finishing, and inspection support. If a project uses DMLS for complex geometry, MTSPi can help review the post-machined features: datums, holes, threads, sealing areas, pads, tolerances, finish requirements, and inspection needs.

Send your CAD model, drawing, material requirements, expected load case, quantity, post-machining notes, and inspection requirements through the contact page. We can help decide which surfaces should be printed, which should be machined, and where design allowances are needed.

FAQ

Can DMLS parts be as dense as wrought metal?

DMLS parts can reach high density, but equivalence to wrought metal depends on material, process qualification, heat treatment, HIP, orientation, and inspection. Critical applications should not rely on generic claims alone.

What is the biggest risk with DMLS density?

The biggest risk is hidden porosity or lack of fusion in a functional area, especially near loaded surfaces, pressure boundaries, sealing faces, or fatigue-critical regions.

Does HIP remove all porosity?

HIP can reduce or close certain internal pores, but it does not replace proper process control, design review, support strategy, and inspection.

Should DMLS holes be printed or machined?

Loose clearance holes may be printed, but precision holes, threaded holes, reamed holes, and sealing bores are usually better machined after printing.

Is DMLS good for production parts?

DMLS can be used for production when geometry, quantity, material, certification, and inspection requirements justify it. For simple shapes, CNC machining is often more practical.

Can MTSPi machine DMLS printed blanks?

MTSPi can support CNC post-processing planning for printed blanks, including machined datums, holes, threads, sealing surfaces, finishing, and inspection requirements.

Categories
Blog CNC Machining Basics Guides Manufacturing Process Comparisons

Direct Metal Laser Sintering (DMLS): Metal 3D Printing and CNC Post-Processing Guide

Direct Metal Laser Sintering, commonly shortened to DMLS, is a metal 3D printing process used to build complex metal parts directly from digital CAD data. Instead of cutting material away from a billet, DMLS fuses fine metal powder layer by layer with a high-energy laser. The result can be a dense metal part with shapes that would be difficult, expensive, or impossible to make with conventional machining alone.

For engineers sourcing prototypes or low-volume parts, DMLS should not be viewed as a replacement for every CNC machined component. It is a complementary process. The strongest projects use each method where it makes sense: DMLS for design freedom and complex forms, then CNC machining, turning, finishing, and inspection for critical surfaces.

What Is Direct Metal Laser Sintering?

DMLS is a powder-bed fusion process. A thin layer of metal powder is spread across a build platform. A laser traces the cross-section of the part and fuses selected areas. The platform lowers, a new powder layer is applied, and the process repeats until the full part is built. After printing, loose powder is removed and the part is separated from the build plate.

The process is often grouped with metal 3D printing, selective laser melting, and laser powder bed fusion. Naming can vary by machine supplier and material system, but the practical idea is the same: create metal geometry layer by layer from powder and laser energy.

How DMLS Works Step by Step

  • A 3D CAD model is prepared and oriented for printing.
  • Support structures are added where needed to anchor the part and control heat distortion.
  • A thin metal powder layer is spread across the machine bed.
  • The laser fuses the cross-section of the part in that layer.
  • The build platform lowers and the next powder layer is applied.
  • The completed part is cooled, removed from the powder, and cut from the build plate.
  • Post-processing such as heat treatment, support removal, CNC machining, polishing, blasting, or inspection is completed.

DMLS Materials

DMLS is commonly used with metal materials such as stainless steel, aluminum alloys, titanium alloys, cobalt chrome, nickel alloys, maraging steel, and tool steel depending on supplier capability. The right material depends on strength, weight, corrosion resistance, temperature, fatigue, biocompatibility, and finishing requirements. For machined alternatives, compare options in MTSPi’s CNC machining materials library.

Material Family Why It Is Used in DMLS CNC Selection Note
Stainless steel Corrosion resistance and general mechanical strength CNC may be better for simple shafts, fittings, plates, and precision faces
Aluminum alloys Lightweight functional prototypes and aerospace-style parts CNC aluminum is often faster and smoother for conventional geometry
Titanium alloys High strength-to-weight ratio and medical or aerospace applications CNC titanium can finish critical surfaces after printing
Nickel alloys Heat and corrosion resistance Post-machining may be required for mating surfaces and tight features
Tool or maraging steel High strength tooling, inserts, and conformal cooling concepts Heat treatment and final machining must be planned carefully

Advantages of DMLS

  • Can produce complex internal channels, lattice structures, and lightweight forms.
  • Reduces assembly count by combining several parts into one printed component.
  • Useful for functional metal prototypes without hard tooling.
  • Supports design iterations before casting, forging, or machining strategy is finalized.
  • Can create conformal cooling channels, medical structures, aerospace brackets, and custom tooling inserts.

Limitations of DMLS

  • Surface finish is usually rougher than CNC machining unless post-processed.
  • Tolerances may not match precision machining on critical holes, flats, threads, and sealing areas.
  • Support structures can leave marks and require removal.
  • Build orientation affects strength, surface quality, support needs, and dimensional accuracy.
  • Material choices are narrower than conventional CNC stock materials.
  • Simple prismatic or turned parts are often cheaper and faster by CNC machining.

DMLS vs CNC Machining

DMLS and CNC machining solve different problems. DMLS creates geometry by adding material, so it is excellent when the geometry is complex. CNC machining removes material from solid stock, so it is excellent when the part needs accurate surfaces, holes, threads, flatness, repeatability, and a broad material choice.

Decision Point Choose DMLS When Choose CNC Machining When
Geometry Internal channels, lattice structures, organic shapes, topology-optimized parts Prismatic parts, shafts, plates, housings, brackets, pockets, threaded features
Tolerance Moderate tolerance is acceptable or post-machining is planned Tight dimensions, datums, flatness, bore accuracy, and threads are critical
Surface finish As-printed or blasted surface is acceptable Smooth machined, polished, anodized, plated, or sealing surfaces are required
Quantity Complex prototypes or specialized low-volume components Prototypes through production batches with repeatable geometry
Cost Complexity justifies the process Geometry is simple enough to machine efficiently

For conventional metal prototypes, rapid prototyping through CNC machining is often the more practical choice. For complex parts with internal channels or lightweight structures, DMLS may be better first, followed by CNC post-processing.

When DMLS Parts Need CNC Post-Processing

Many DMLS parts are not finished when they leave the printer. Support removal and heat treatment are common, and precision features often need secondary machining. A printed bracket may need CNC-milled mounting faces. A printed manifold may need reamed holes, tapped ports, or machined sealing surfaces. A printed insert may need ground or polished functional areas.

  • Machine flat datum surfaces that locate the part in an assembly.
  • Drill, ream, or bore precision holes after printing.
  • Tap threads instead of relying only on printed thread geometry.
  • Machine sealing surfaces and bearing seats.
  • Use polishing, blasting, or coating to control surface finish.
  • Inspect critical features with gauges, CMM, or optical methods.

Design Rules for DMLS Parts

Designing for DMLS is different from designing for CNC machining. A geometry that prints well may be difficult to inspect or post-machine. A geometry that machines well may not use the full value of additive manufacturing. The best design considers both printing and secondary operations from the beginning.

  • Avoid unnecessary solid mass; use ribs, shells, or lattice only where they support function.
  • Plan support access and removal before approving the design.
  • Add machining allowance on critical faces, holes, and sealing areas.
  • Orient the part to balance accuracy, surface finish, strength direction, and support requirements.
  • Avoid enclosed powder traps unless powder removal is designed into the part.
  • Mark post-machined features clearly on the drawing.
  • Define inspection requirements for functional surfaces rather than over-tolerancing the whole part.

Tolerances and Surface Finish

DMLS tolerances depend on machine, material, part size, orientation, heat treatment, and post-processing. Small details can be impressive, but precision mating features usually need machining. Surface finish is also process-dependent. As-printed metal surfaces often have a granular texture, while machined faces are smoother and more dimensionally controlled.

If the part needs a controlled finish, consider the full process route: print, stress relieve, remove supports, CNC machine, inspect, then apply finishing if needed. For finish options on metal parts, see MTSPi’s surface treatment guide.

Common Applications

DMLS is useful where geometry complexity creates real value. Typical applications include aerospace brackets, lightweight robotic parts, conformal cooling inserts, medical implants or instruments, custom manifolds, heat exchangers, complex housings, and low-volume metal prototypes.

In many of these applications, DMLS and CNC are combined. A lightweight printed shape may still need 5-axis machining to finish complex datum surfaces or angled features. A printed round feature may need turning or grinding for final fit.

Cost Drivers in DMLS

  • Build volume and part height affect machine time.
  • Material powder cost varies significantly by alloy.
  • Support structures add build time and removal labor.
  • Heat treatment, HIP, machining, polishing, and inspection add cost.
  • Poor orientation can increase supports, distortion, and post-processing difficulty.
  • A part designed like a conventional machined block may waste the benefits of DMLS.

How to Decide Between DMLS, CNC, and Hybrid Manufacturing

Start with the function. If the part is a simple plate, bracket, shaft, spacer, or housing with accessible features, CNC machining is usually the first option to quote. If the part has internal flow channels, impossible undercuts, topology-optimized load paths, or a design that combines many parts into one, DMLS becomes more attractive.

For the strongest decision, split the part into functional zones. Which surfaces need precision? Which areas carry load? Which areas only need clearance? Which features can remain as-printed? Which features must be machined after printing? This approach avoids paying for unnecessary precision while protecting the features that actually matter.

How MTSPi Can Support DMLS-Related Projects

MTSPi focuses on custom CNC machining, rapid prototyping, surface finishing, and inspection support. Even when a project starts with metal 3D printing, CNC post-processing may be required to turn the printed blank into a functional assembly-ready part. MTSPi can help review drawings for machined datums, holes, threads, sealing faces, finish requirements, and inspection planning.

If your project is comparing metal 3D printing and machining, send your CAD model, drawing, material requirements, quantity, tolerance notes, and application details through the contact page. We can help identify which features should be printed, which should be CNC machined, and where design changes may reduce risk.

FAQ

What is DMLS used for?

DMLS is used for complex metal prototypes and low-volume parts such as lightweight brackets, manifolds, conformal cooling inserts, medical structures, aerospace components, and custom tooling.

Is DMLS the same as SLS?

They are related powder-bed processes, but SLS is often used for polymers while DMLS refers to metal powder fusion. Naming varies across suppliers, so material and process details should be confirmed.

Are DMLS parts fully dense?

DMLS parts can achieve high density when processed correctly, but final properties depend on material, machine parameters, orientation, heat treatment, and quality control.

Can DMLS make threads?

Threads can sometimes be printed, but functional precision threads are often tapped or machined after printing for better accuracy and strength.

When is CNC machining better than DMLS?

CNC machining is usually better for simple geometry, tight tolerance, smooth finish, broad material selection, and repeatable production at lower cost.

Can MTSPi machine DMLS parts after printing?

MTSPi can support CNC post-processing considerations such as machined faces, holes, threads, datum surfaces, finishing, and inspection planning for metal prototype projects.

Categories
Blog CNC Machining Basics

What Is NC Machining? Process, Types, and CNC Comparison

NC machining, or numerical control machining, is the earlier form of automated machine control that uses coded instructions to move machine tools. It created the foundation for modern CNC machining.

The key difference is that CNC uses computer-based control, easier program editing, feedback, simulation, and more flexible automation. NC is historically important, but CNC dominates modern precision manufacturing.

Quick Guide to Nc Machining

Item Purpose Manufacturing Note
NC machining Older automated machine tools Less flexible and harder to edit
CNC machining Modern milling, turning, drilling, routing Computer-controlled and highly repeatable
Manual machining One-off adjustments and simple work Operator skill drives consistency
CAM workflow Programming complex parts Generates efficient toolpaths for CNC

Process Selection Notes

The best process depends on material, geometry, tolerance, quantity, surface finish, heat effects, burr requirements, and whether the part needs secondary machining or finishing.

  • Match the process to the material and geometry.
  • Confirm critical dimensions before quoting.
  • Plan finishing and inspection before production.
  • Use prototypes to validate fit when the assembly risk is high.

Common Applications

Nc Machining is relevant for prototypes, custom components, fixtures, low-volume manufacturing, maintenance parts, and engineering projects where function, cost, and lead time must be balanced.

Cost Factors

Cost usually depends on setup time, material price, number of operations, tool access, tolerance requirements, surface finish, inspection depth, and batch quantity.

Design and Sourcing Notes

The safest design approach is to define the part’s function first, then assign tolerances only where they affect assembly, movement, sealing, safety, or long-term performance.

  • Avoid unnecessary tight tolerances on non-critical surfaces.
  • Keep internal corners, hole depths, wall thickness, and tool access realistic.
  • Call out cosmetic surfaces separately from functional surfaces.
  • Include material, finish, quantity, and inspection notes in the RFQ package.

Quality Checks That Matter

Quality control may include visual inspection, dimensional measurement, thread checks, gauge checks, flatness checks, runout checks, surface finish checks, or CMM inspection depending on the part’s risk and function.

Related MTSPi Resources

FAQ

What is the main consideration for NC machining?

The main consideration is whether the design, material, and process can meet the functional requirements without adding unnecessary cost or risk.

Can MTSPi help with custom parts for this topic?

Yes. MTSPi can review drawings, material requirements, tolerances, finishing, and inspection needs for custom CNC machined or related manufacturing parts.

What should I send for a quote?

Send 3D CAD, 2D drawings, material grade, quantity, surface finish requirements, tolerance notes, and any critical assembly information.

Categories
Blog CNC Machining Basics

Sheet Metal Hemming: Process, Types, Advantages, and Design Rules

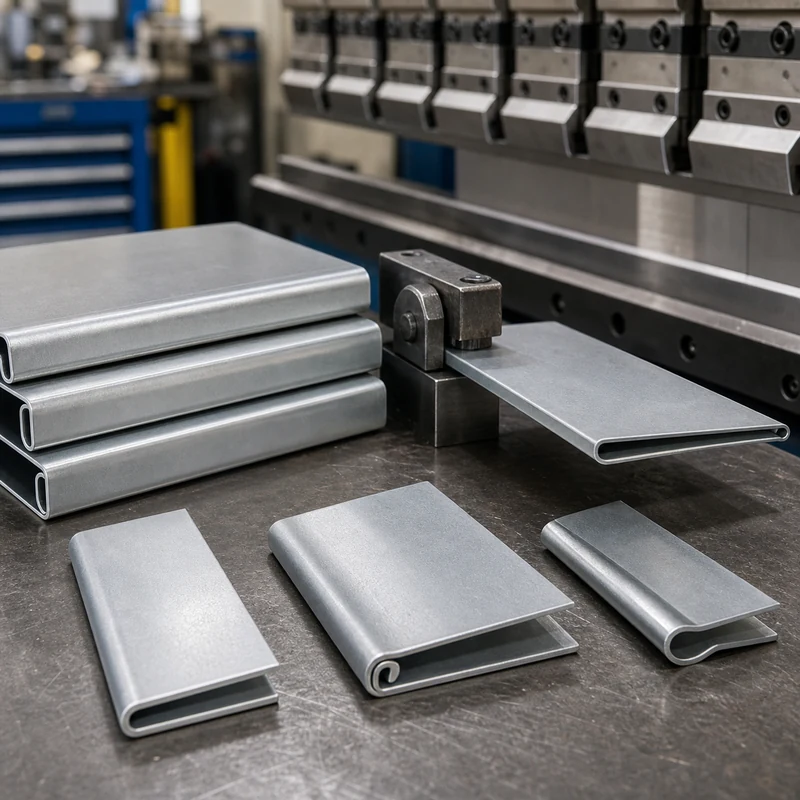
Sheet metal hemming folds an edge back onto itself to create a safer, stronger, and cleaner border. It is common in panels, covers, doors, automotive parts, enclosures, and consumer products.

A hem can remove sharp edges, improve stiffness, hide a raw cut edge, and help two sheets join together. The process must be planned with bend radius, material thickness, grain direction, and tooling clearance in mind.

Quick Guide to Sheet Metal Hemming

Item Purpose Manufacturing Note
Open hem Edge is folded but leaves a small gap Useful when material may crack if flattened
Closed hem Edge is folded flat Clean appearance but higher forming stress
Teardrop hem Rounded internal gap Good for harder or thicker materials
Rope hem Rolled circular edge Adds stiffness and safer handling

Process Selection Notes

The best process depends on material, geometry, tolerance, quantity, surface finish, heat effects, burr requirements, and whether the part needs secondary machining or finishing.

  • Match the process to the material and geometry.
  • Confirm critical dimensions before quoting.
  • Plan finishing and inspection before production.
  • Use prototypes to validate fit when the assembly risk is high.

Common Applications

Sheet Metal Hemming is relevant for prototypes, custom components, fixtures, low-volume manufacturing, maintenance parts, and engineering projects where function, cost, and lead time must be balanced.

Cost Factors

Cost usually depends on setup time, material price, number of operations, tool access, tolerance requirements, surface finish, inspection depth, and batch quantity.

Design and Sourcing Notes

The safest design approach is to define the part’s function first, then assign tolerances only where they affect assembly, movement, sealing, safety, or long-term performance.

  • Avoid unnecessary tight tolerances on non-critical surfaces.
  • Keep internal corners, hole depths, wall thickness, and tool access realistic.
  • Call out cosmetic surfaces separately from functional surfaces.
  • Include material, finish, quantity, and inspection notes in the RFQ package.

Quality Checks That Matter

Quality control may include visual inspection, dimensional measurement, thread checks, gauge checks, flatness checks, runout checks, surface finish checks, or CMM inspection depending on the part’s risk and function.

Related MTSPi Resources

FAQ

What is the main consideration for sheet metal hemming?

The main consideration is whether the design, material, and process can meet the functional requirements without adding unnecessary cost or risk.

Can MTSPi help with custom parts for this topic?

Yes. MTSPi can review drawings, material requirements, tolerances, finishing, and inspection needs for custom CNC machined or related manufacturing parts.

What should I send for a quote?

Send 3D CAD, 2D drawings, material grade, quantity, surface finish requirements, tolerance notes, and any critical assembly information.

Categories
Blog CNC Machining Basics

Tack Welding Explained: Purpose, Types, Advantages, and Design Notes

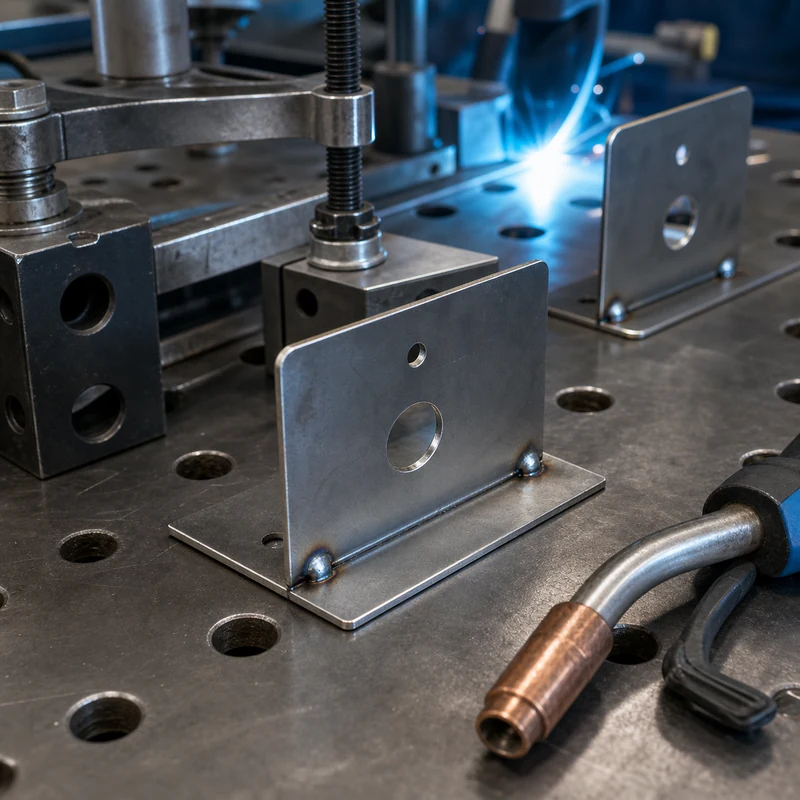
Tack welding is the temporary or semi-permanent weld used to hold parts in position before the final weld is completed. It may look small, but it controls alignment, gap, distortion, and assembly repeatability during sheet metal and welded structure production.

For CNC machined and fabricated assemblies, tack welding is not just a shop-floor shortcut. It is part of process planning. Poor tack weld placement can pull brackets out of position, create stress, or make final welding harder. Good tack welding keeps the part stable while leaving enough access for final welding, grinding, inspection, and finishing.

Quick Comparison of Tack Welding Methods

Tack Weld Type Best Use Main Risk
Small intermittent tacks Thin sheet metal and light brackets Can break if handling is rough
Bridge tacks Maintaining a root gap before final welding Must be removed or fused correctly
Strong temporary tacks Heavy fixtures and structural parts May add distortion if oversized
Corner tacks Boxes, frames, and folded assemblies Can lock in misalignment if sequence is wrong

Why Tack Welding Is Used

Tack welds keep individual pieces from moving while a welder checks fit-up and prepares the final weld sequence. They reduce the need for complex clamps, shorten setup time, and help maintain the intended geometry of brackets, frames, covers, panels, and welded fixtures.

  • Holds parts before final welding
  • Maintains spacing and joint alignment
  • Reduces assembly movement during handling
  • Helps control distortion when used with the right sequence

Where Tack Welding Fits in Fabrication

Tack welding is common in sheet metal enclosures, welded frames, automotive brackets, machinery guards, equipment bases, and prototype metal assemblies. It is especially useful when parts are cut, bent, machined, then welded into a final assembly.

Common Mistakes

The most common problems are oversized tacks, poor cleaning, wrong sequence, bad fit-up, and putting tack welds where final weld access is blocked. A tack weld should support the process, not create a defect that must be repaired later.

Design and Sourcing Notes

Designers should think about tack welding while defining joint access, bend sequence, hole locations, and finishing requirements.

  • Leave enough weld access around corners and flanges.
  • Avoid placing cosmetic surfaces where tack marks will be difficult to remove.
  • Specify critical dimensions after welding if distortion matters.
  • Plan surface treatment after welding and cleanup.

Quality Checks That Matter

Inspection should check alignment, gap, cracks, incomplete fusion, and distortion before final welding proceeds. For precision assemblies, dimensional inspection after welding may be more important than measuring each flat part before welding.

Related MTSPi Resources

FAQ

Is tack welding permanent?

It can become part of the final weld if properly fused, but many tack welds are temporary positioning welds.

Does tack welding cause distortion?

Yes, if tack welds are too large or placed in a poor sequence. Balanced tack placement helps reduce movement.

Should tack welds be inspected?

Yes. Cracked or poorly placed tack welds can affect the final weld and part alignment.

Categories
Blog CNC Machining Basics

Hole Machining in CNC: Drilling, Boring, Reaming, Tapping, and Design Rules

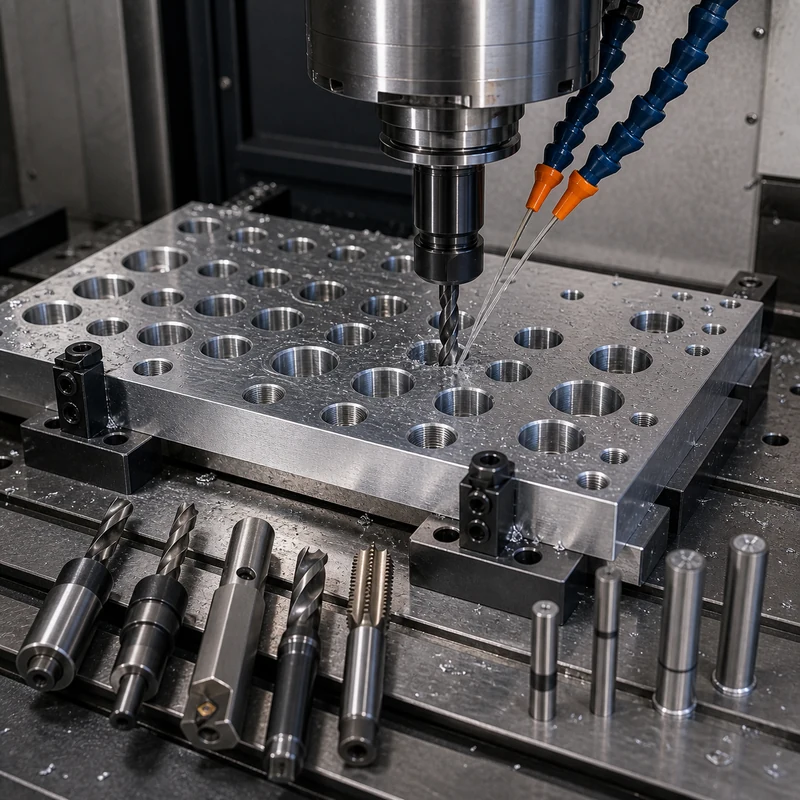
Quick answer: Hole machining is the CNC process of creating or finishing holes using drilling, boring, reaming, tapping, countersinking, counterboring, or thread milling. The right method depends on hole size, depth, tolerance, surface finish, thread requirement, and inspection needs.

Why Hole Machining Matters

Holes often control how a part assembles. They may locate dowel pins, accept screws, support bearings, pass fluid, reduce weight, or align mating parts. Small errors in hole position, diameter, depth, or thread fit can cause major assembly problems.

Common CNC Hole Machining Methods

Method Purpose Best use
Drilling Creates a basic round hole Clearance holes, pilot holes, general features
Boring Improves or enlarges an existing hole Accurate diameters and alignment-critical bores
Reaming Finishes a hole to closer size and smoother surface Dowel holes, bearing fits, precision diameters
Tapping Cuts internal threads Screw assembly and fastener holes
Thread milling Mills internal or external threads Large threads, hard materials, blind holes, flexible thread control
Countersinking / counterboring Creates screw head seating geometry Flush screws, socket head clearance, assembly hardware

Drilling vs Boring vs Reaming

Drilling is usually the first operation because it creates the hole. Boring improves hole location, straightness, or diameter after drilling. Reaming is used when the hole needs a more accurate final size and better finish than drilling alone can provide.

Design Rules for Better Holes

  • Avoid very deep holes unless they are truly required.
  • Keep hole diameters standard where possible.
  • Leave enough edge distance around holes.
  • Specify whether threads are blind or through.
  • Use realistic tolerances for non-critical clearance holes.
  • Define datum references for hole position when assembly matters.

Hole Tolerances and Inspection

Hole inspection may use pin gauges, bore gauges, CMM inspection, thread gauges, depth gauges, or optical tools. For critical hole patterns, connect the drawing to a clear inspection method before machining.

Material Effects

Aluminum is generally easy to drill and tap. Stainless steel can work-harden and needs suitable tools. Brass cuts cleanly but may grab with the wrong drill geometry. Plastics may require sharp tools and heat control. Material choice should be reviewed through the CNC material guide.

Related CNC Processes

Hole machining appears in both CNC milling and CNC turning. Milled parts often need bolt patterns, dowel holes, and tapped holes. Turned parts often need center holes, bores, cross holes, threads, and counterbores.

FAQ

What is hole machining?

Hole machining is the process of creating or finishing holes with drilling, boring, reaming, tapping, or related operations.

Is drilling enough for precision holes?

Not always. Precision holes may need boring or reaming after drilling.

What is the best method for threaded holes?

Tapping is common for standard threads, while thread milling is useful for larger threads, hard materials, and blind holes.

How do I reduce hole machining cost?

Use standard sizes, avoid unnecessary tight tolerances, limit deep holes, and provide clear thread and depth notes.

Need help choosing a machining route?

Send MTSPi your drawing, material, quantity, finish, and inspection requirements. We will review the part for manufacturability before quoting.

Contact MTSPi for a CNC machining quote

Practical Buyer Notes

Hole machining deserves depth because holes are often the most important assembly features on a part. A simple drilled hole, reamed dowel hole, tapped blind hole, bearing bore, and counterbore all require different planning.

The page should make it clear that drilling is only one hole-making method. Accuracy, surface finish, position, roundness, thread fit, and depth may require boring, reaming, tapping, thread milling, or CMM inspection.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Hole function Classify holes as clearance, threaded, dowel, bearing, fluid, or weight-reduction Function decides tolerance and process
Machining method Use drilling, boring, reaming, tapping, or thread milling as needed Different methods create different accuracy levels
Depth and access Review deep holes, blind holes, and tool clearance Avoids broken tools and poor finish
Inspection Use gauges, CMM, or thread checks for critical holes Prevents assembly failures

Common Mistakes to Avoid

  • Expecting drilled holes to meet precision bore requirements.
  • Leaving thread depth or blind-hole bottom clearance undefined.
  • Putting holes too close to edges, bends, or thin walls.
  • Not defining position tolerance for hole patterns that control assembly.

Recommended MTSPi Review Workflow

MTSPi should review hole features separately from general part geometry. Hole diameter, depth, position, thread, finish, and inspection method often decide the correct machining route.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send drawings with hole callouts, tolerances, thread standards, depth notes, datum references, and mating hardware information where possible.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Example: Choosing the Right Hole Process

A simple bolt clearance hole may only need drilling and deburring. A dowel pin hole may need drilling, reaming, and position inspection. A bearing bore may need boring, controlled surface finish, and diameter verification. A threaded blind hole may need drilling, tapping or thread milling, depth control, and a go/no-go gauge check.

These examples show why hole machining should be specified by function. If a drawing treats every hole the same way, the supplier may over-machine simple holes or under-control critical ones.

Conclusion

Hole machining looks simple, but holes often decide whether a part assembles correctly. Choosing the right method and defining tolerances, threads, and inspection requirements clearly can prevent delays and reduce CNC machining cost.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

Hole Machining in CNC: Drilling, Boring, Reaming, Tapping, and Design Rules

We'll Send You Back with Price Immediately!