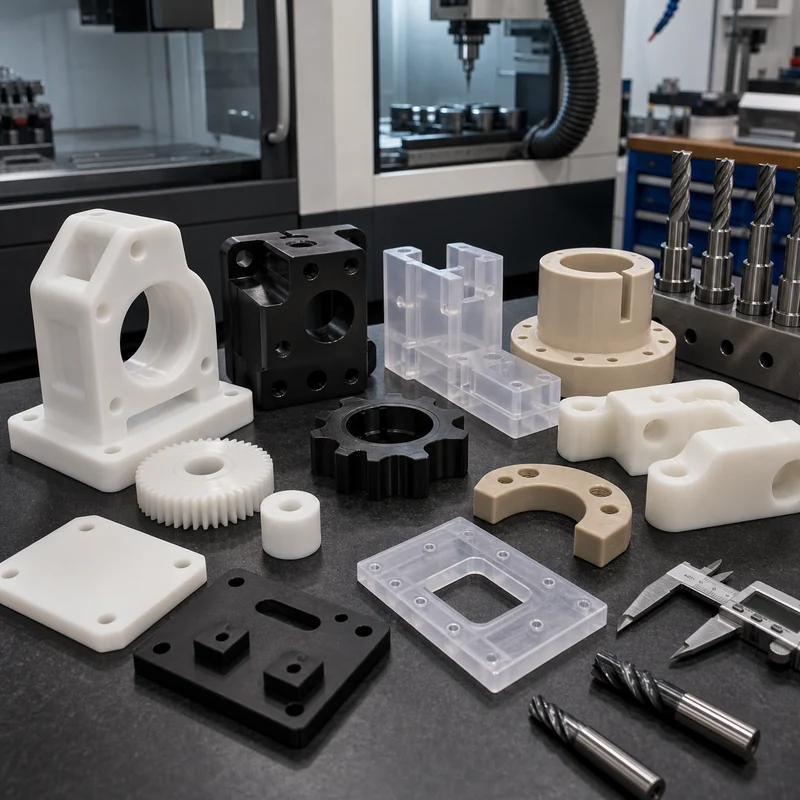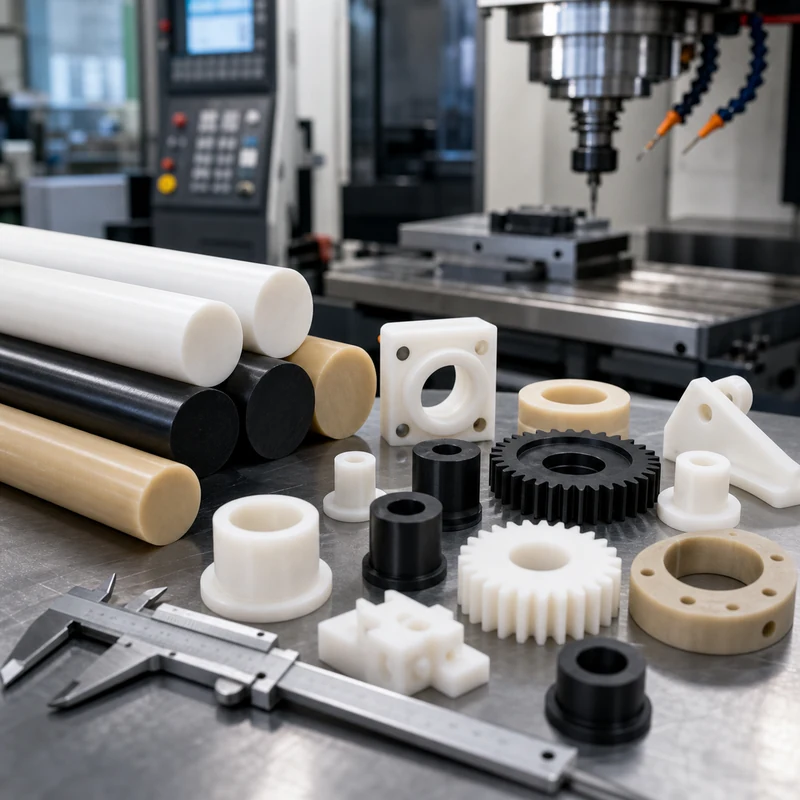
Nylon is one of the most widely used engineering plastics, but the word “nylon” does not describe one single material. PA6, PA66, PA12, PA11, PA6/12, glass-filled nylon, mineral-filled nylon, and impact-modified nylon can behave very differently in machining, assembly, moisture exposure, heat, and long-term wear. Choosing the wrong type can lead to swelling, loose tolerances, tool wear, cracked thin walls, or parts that work in the prototype stage but fail in production.
This guide explains the main types of nylon from a CNC machining and product-design point of view. It is written for engineers, sourcing teams, and product developers who need practical material selection help before ordering machined plastic parts. For project-specific material review, MTSPi can also evaluate drawings through our nylon CNC machining and broader CNC plastic machining capabilities.
Quick Answer: Which Type of Nylon Should You Choose?
| Nylon Type | Best For | Main Strength | Main Caution |
|---|---|---|---|
| PA6 / Nylon 6 | General machined parts, gears, rollers, wear pads, prototypes | Tough, economical, good wear resistance | Absorbs moisture and may move dimensionally |
| PA66 / Nylon 6/6 | Higher strength parts, wear components, electrical and mechanical parts | Higher stiffness, wear resistance, and heat performance than PA6 | Still absorbs moisture; can be harder to machine cleanly |
| PA6/12 | Moisture-sensitive applications, molded parts, cable and fluid-system components | Lower moisture absorption than PA6 or PA66 | Usually less strong than PA66 |
| PA11 | Flexible, impact-resistant, lower-moisture parts, often 3D printed | Bio-based source, good low-temperature impact performance | Lower heat resistance than some nylon grades |
| PA12 | SLS/MJF printed parts, lightweight housings, ducts, fixtures, flexible functional prototypes | Low moisture absorption and good chemical resistance | Lower stiffness unless filled |
| Glass-filled nylon | Stiff brackets, structural parts, heat-resistant components | Higher stiffness, strength, and thermal stability | More abrasive; can wear tools and expose rougher edges |
| Mineral-filled nylon | Dimensionally stable parts, heat-resistant molded components | Lower shrinkage and better stability | Can be more brittle depending on formulation |
What Is Nylon?
Nylon is a family of polyamide materials. The “PA” abbreviation means polyamide, and the number in a grade name describes the chemistry of the polymer chain. That chemistry affects melting point, moisture absorption, stiffness, toughness, fatigue behavior, and chemical resistance. This is why two nylon grades may look similar but behave differently after machining.
Most nylon materials offer good wear resistance, low friction, toughness, and chemical resistance compared with commodity plastics. They are often used for gears, bushings, rollers, guides, electrical insulators, spacers, housings, and mechanical components that need to be lighter than metal. The tradeoff is moisture absorption. Many nylons absorb water from the environment, which can change part dimensions and mechanical properties.
Why Nylon Type Matters for CNC Machining
CNC machining removes material from nylon stock such as sheet, plate, rod, or tube. Nylon machines well compared with many plastics, but it is not as rigid as metal. It can deflect under cutting force, soften if heat builds up, and expand or shrink with moisture and temperature. Grade selection therefore affects more than material strength; it affects how accurately the part can be held after machining.
- PA6 and PA66 are common for machined mechanical components, but moisture control should be considered.
- PA12 and PA11 are often more stable in humid applications, especially in additive manufacturing contexts.
- Filled nylons improve stiffness and heat resistance but can create tool wear and edge-quality challenges.
- Thin walls, deep slots, small holes, and tight press fits should be reviewed before production.
Nylon 6 (PA6): Tough and Economical, but Moisture Sensitive
PA6 is one of the most common nylon grades for machined plastic parts. It offers a strong balance of toughness, wear resistance, machinability, and cost. It is frequently selected for rollers, gears, wear pads, bushings, guide blocks, spacers, and general mechanical components.
The main caution with PA6 is moisture absorption. In a dry shop environment, a PA6 part may measure correctly after machining, but it can change size after absorbing moisture in service. For loose-clearance parts this may be acceptable. For close-fit holes, sliding features, bearing seats, or assembly-critical dimensions, the design should allow for environmental movement.
Nylon 6/6 (PA66): Stronger, Stiffer, and More Heat Resistant
PA66, also called Nylon 6/6, usually offers higher stiffness, tensile strength, wear resistance, and heat resistance than PA6. This makes it a good candidate for more demanding mechanical parts, especially when a component needs improved load capacity or better dimensional performance under moderate heat.
PA66 is widely used for gears, electrical components, bushings, housings, fastener-related parts, and structural plastic components. For CNC machining, it generally cuts well, but the same moisture warning applies. If a drawing calls for tight tolerance after conditioning or after exposure to humidity, that should be stated clearly.
Nylon 6/12 (PA6/12): Better Moisture Resistance
PA6/12 is often selected when lower moisture absorption is more important than maximum strength. It is common in applications such as tubing, cable protection, fuel-related components, bristles, and molded parts that must remain more stable in humid or fluid-contact environments.
For machined parts, PA6/12 can be useful when PA6 or PA66 swelling is a concern. It may not match the strength of PA66, so the choice should be based on the real service condition: load, humidity, chemical exposure, operating temperature, and assembly clearance.
Nylon 11 (PA11): Flexible, Impact Resistant, and Bio-Based
PA11 is known for toughness, flexibility, low-temperature impact performance, and lower moisture absorption than PA6 and PA66. It is also often discussed because its raw material source can be bio-based. In manufacturing, PA11 appears frequently in 3D printing and flexible functional components rather than as the first default for CNC machining from stock.
Choose PA11 when impact resistance, flexibility, and moisture stability matter more than maximum stiffness. For rigid precision-machined parts, compare it with PA12, Delrin/POM, or reinforced nylon depending on the application.
Nylon 12 (PA12): Stable, Chemical Resistant, and Common in 3D Printing
PA12 is a popular material for SLS and Multi Jet Fusion 3D printed parts, but it is also useful as a reference point when comparing nylon types. It generally absorbs less moisture than PA6 and PA66, offers good chemical resistance, and can produce functional prototypes, ducts, clips, housings, and fixtures.
Unfilled PA12 is not always as stiff as filled nylon or PA66, so designers should check wall thickness and load conditions. Glass-filled or mineral-filled PA12 can improve mechanical and thermal performance, but filled formulations may change surface finish and part toughness.
Filled Nylon: Glass, Mineral, Carbon, and Impact-Modified Grades
Fillers are added to nylon to change its mechanical behavior. Glass-filled nylon is common because it increases stiffness, strength, and heat resistance. Mineral-filled nylon can improve dimensional stability and reduce shrinkage. Impact-modified nylon improves toughness. Carbon-filled nylon can improve stiffness, conductivity, or static-control behavior depending on the formulation.
| Filled Nylon Type | What It Improves | Design / Machining Note |
|---|---|---|
| Glass-filled nylon | Stiffness, strength, creep resistance, heat performance | More abrasive on tools; edges may feel sharper or rougher |
| Mineral-filled nylon | Dimensional stability, lower shrinkage, heat stability | May reduce impact strength depending on grade |
| Impact-modified nylon | Toughness and resistance to cracking | May reduce stiffness compared with reinforced grades |
| Carbon-filled nylon | Stiffness, wear, or electrical/static behavior | Confirm conductivity and surface requirements before selection |
Filled nylon is not automatically better. If a part needs snap-fit flexibility, impact toughness, or smooth bearing contact, an unfilled or differently modified grade may perform better. If a part needs stiffness, heat resistance, and low creep, filled nylon may be the better choice.
Nylon vs Delrin, PEEK, and Polycarbonate
Nylon is not always the best plastic. Delrin/POM is often selected when low moisture absorption and dimensional stability are more important than nylon-like toughness. PEEK is far more expensive but performs well under heat, chemicals, and demanding environments. Polycarbonate is selected for impact-resistant transparent parts. Acrylic is selected for optical clarity but is more brittle.
| Material | Use Instead of Nylon When You Need | Related MTSPi Page |
|---|---|---|
| Delrin / POM | Better dimensional stability, low friction, crisp machining | Delrin CNC machining |
| PEEK | High temperature, chemical resistance, medical or aerospace-grade performance | PEEK CNC machining |
| Polycarbonate | Impact-resistant transparent parts | PC CNC machining |
| Acrylic | Clear cosmetic panels and polished optical surfaces | Acrylic CNC machining |
Design Tips for CNC Machined Nylon Parts
- Avoid specifying metal-like tolerances on non-critical nylon features.
- Use generous radii and avoid sharp internal corners where stress can concentrate.
- Support thin walls with ribs or additional thickness when possible.
- Leave realistic clearance for holes, bushings, sliding parts, and moisture exposure.
- Specify whether final dimensions should be checked dry, conditioned, or after finishing.
- Plan deburring carefully; nylon can leave stringy burrs around drilled holes and edges.
Surface Finish and Inspection
Nylon parts are usually machined to a functional finish rather than polished like cosmetic metals. Tool sharpness, feed rate, chip evacuation, and heat control all affect the final surface. If a part has sealing areas, sliding contact, or visible surfaces, call those areas out on the drawing. For related finishing options across CNC parts, see surface treatment planning.
Inspection should match the way the part functions. Simple parts may only need caliper and gauge checks. Precision assemblies may require bore gauges, pin gauges, thread gauges, optical checks, or CMM measurement. For projects with tight tolerances or production documentation, connect the drawing requirements with quality assurance before machining begins.
How MTSPi Helps With Nylon Material Selection
MTSPi supports CNC machining for nylon and other engineering plastics, including prototypes, low-volume production, and repeat orders. We can review material options, machining strategy, wall thickness, hole design, thread feasibility, finish expectations, and inspection requirements before quoting. If the nylon type is not fixed yet, we can compare PA6, PA66, PA12, Delrin, PEEK, PC, and other plastics against the actual application.
To move forward, send your 3D model, 2D drawing, material preference, annual or batch quantity, target tolerance, and operating environment through our contact page. You can also browse the broader CNC machining materials library for other material choices.
FAQ
What is the strongest type of nylon?
For many machined-part applications, PA66 and glass-filled nylon are stronger and stiffer than general PA6. However, the best choice depends on load, moisture, temperature, impact, and whether the part needs flexibility.
Which nylon absorbs the least moisture?
PA11 and PA12 generally absorb less moisture than PA6 and PA66. PA6/12 is also selected when better moisture resistance is needed compared with PA6 or PA66.
Is nylon good for CNC machining?
Yes. Nylon is commonly CNC machined for gears, bushings, rollers, spacers, guides, and wear parts. The main concerns are moisture movement, burr control, heat buildup, and realistic tolerances.
Is glass-filled nylon better than standard nylon?
Glass-filled nylon is better when stiffness, strength, creep resistance, and heat performance are priorities. It is not always better for impact, flexibility, tool wear, edge finish, or sliding contact.
What is the best nylon for gears and bushings?
PA6, PA66, and some filled nylon grades can work for gears and bushings. The final choice depends on load, speed, lubrication, temperature, moisture, and required dimensional stability.
Can MTSPi machine nylon prototypes and production parts?
Yes. MTSPi can machine nylon parts from drawings for prototypes, low-volume production, and batch supply, with material and inspection planning matched to the application.