Choosing between titanium and steel for your CNC project? It’s more than just picking a strong metal. This guide breaks down the five key differences in machining these materials, from cutting speeds to tool wear, helping you make an informed decision for better results and fewer headaches in the shop.
Material Properties and Machinability
When you first compare titanium machining to steel CNC machining, the physical properties tell the whole story. Think of it like cooking: you wouldn’t use the same heat and technique for a delicate fish as you would for a tough steak. The same logic applies here. Titanium’s unique characteristics, like its low thermal conductivity and high chemical reactivity, make it behave very differently under the tool compared to most steels. Understanding this “machinability rating” is your first step to success.
Strength-to-Weight Ratio
This is where titanium truly shines and why it’s a favorite in aerospace and medical implants. Titanium offers a phenomenal strength-to-weight ratio; it’s as strong as many steels but about 45% lighter. However, this very strength is a double-edged sword in machining. That impressive tensile strength means cutting forces are high, demanding rigid machine setups and sharp tools. When you’re working on a part where every gram counts, this property makes the extra effort in machining titanium alloys worthwhile.
Thermal Conductivity
Here’s a critical difference that trips up many machinists. Steel is a pretty good conductor of heat. When you cut it, a significant amount of the heat generated travels up into the chip and away from the cutting edge. Titanium, on the other hand, is a poor thermal conductor. Almost all the heat from the cutting process stays right at the tool-workpiece interface. This creates a localized “hot spot” that can rapidly degrade your cutting tool. It’s one of the main reasons why machining Ti-6Al-4V requires such careful attention to speeds and cooling.
Cutting Tools and Parameters
You can’t use the same tooling strategy for both materials. For steel, you have a wide range of options, including high-speed steel (HSS) for some jobs. But for titanium, you’re almost always looking at premium, uncoated or specially coated carbide tools. The cutting speeds tell a clear story: you might run many steels at several hundred surface feet per minute (SFM), but for titanium, you often need to slow way down, sometimes below 100 SFM. It’s not about being fast; it’s about being smart and preserving your tool. Using the correct parameters is the key to CNC machining titanium efficiently.
Chip Formation and Evacuation
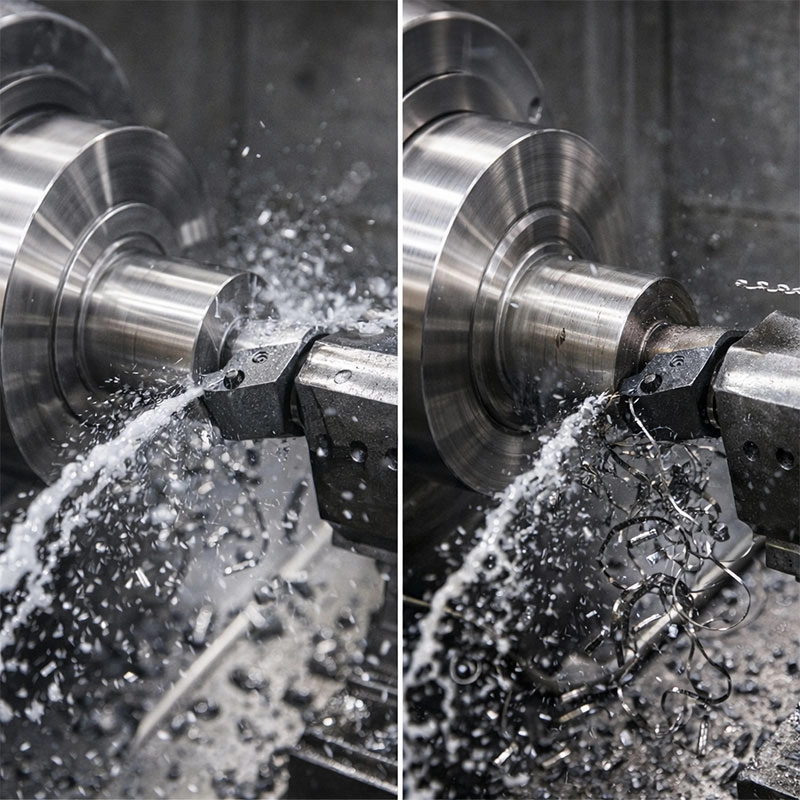
Watch the chips, and they’ll tell you how the cut is going. Steel typically produces a nice, curled chip that breaks easily. Titanium is notorious for producing long, stringy, continuous chips. These “birds’ nests” are not just a nuisance; they’re dangerous. They can wrap around the tool or workpiece, causing scratches, tool breakage, or even machine damage. Effective chip control through proper tool geometry (sharp cutting edges, positive rakes) and high-pressure coolant to break and flush chips is non-negotiable in titanium metal machining.
Coolant and Lubrication Strategy
Given the heat issue we talked about, coolant isn’t just helpful for titanium—it’s essential. But it’s not just any coolant. We recommend using a high-quality, heavy-duty synthetic or semi-synthetic fluid with excellent lubricity. More importantly, the delivery method is crucial. A flood coolant might work for steel, but for titanium, high-pressure through-tool coolant is a game-changer. It penetrates the cutting zone, reduces the heat, and helps with chip evacuation. For some operations, like tapping, using a dedicated tapping fluid can prevent galling, a common problem where titanium welds itself to the tool. You can find excellent guidelines on metalworking fluids from authoritative sources like Machinery Lubrication.
Cost and Application Considerations
Let’s talk about the bottom line. The raw material cost for titanium is significantly higher than for steel. Add to that the slower machining speeds, more expensive tooling, and need for possibly more powerful/rigid CNC machines, and the cost per part skyrockets. So, when do you choose it? When the application demands its unique benefits: unparalleled corrosion resistance, that fantastic strength-to-weight ratio, and biocompatibility. For high-stress, weight-sensitive, or corrosive environments, titanium is worth the investment. For most general-purpose, high-strength applications, machining stainless steel or alloy steel is the more economical and practical choice. It’s all about matching the material to the part’s real-world job.