

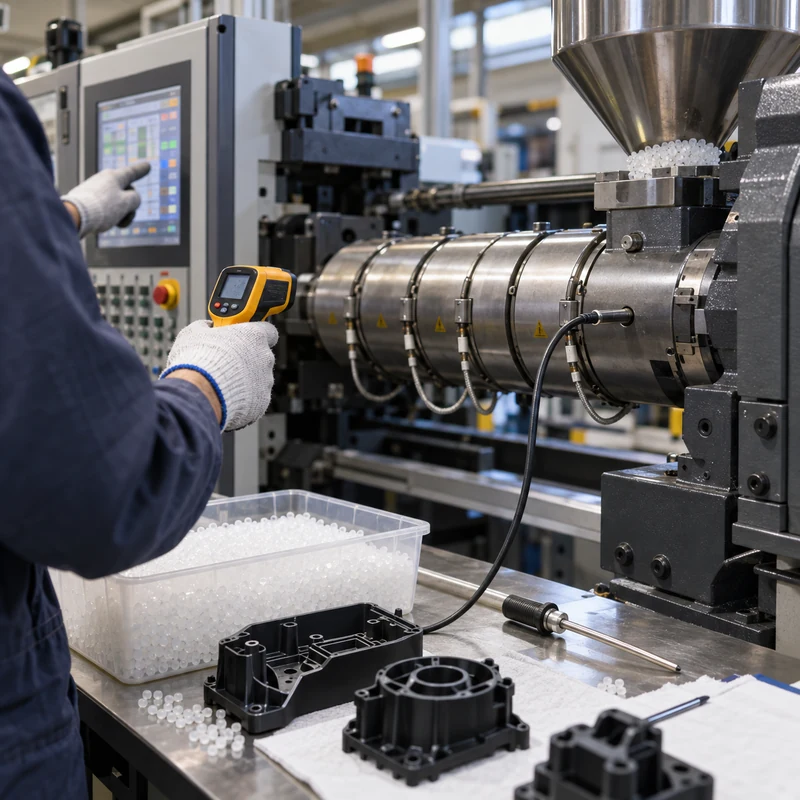
Injection molding melt temperature controls viscosity, cavity filling, weld lines, surface replication, shrinkage, molecular orientation, and degradation. It is related to barrel-zone settings but is not identical to the displayed heater temperatures.
The correct range depends on polymer grade, additives, moisture, residence time, shear, screw design, machine size, part geometry, and mold temperature. Material supplier data is the starting point, followed by an approved process window.
Quick Answer
Use the resin manufacturer’s grade-specific range, dry the material correctly, measure actual melt when needed, and establish a stable window rather than one nominal number. Change temperature only after considering speed, pressure, back pressure, residence time, and mold conditions.
Comparison at a Glance
| Factor | Option A | Option B |
|---|---|---|
| Low melt temperature | High viscosity, short shots, weak weld lines | Increase within approved window and verify drying |
| High melt temperature | Degradation, gas, discoloration, flash | Reduce heat or residence and check shear |
| Barrel display | Shows zone control, not actual melt | Verify with purge measurement or validated method |
| Shear heating | Raises polymer temperature during plasticizing and fill | Control screw speed and injection speed |
| Residence time | Long exposure can damage resin | Match shot size and cycle to machine capacity |
Melt Temperature vs Barrel Temperature
Heater bands control barrel zones while the rotating screw generates shear heat. The polymer experiences a thermal history, so actual melt can differ from setpoints. Measure consistently and safely when troubleshooting.
Material Families
Amorphous and semi-crystalline polymers respond differently. ABS, PC, PMMA, PA, POM, PP, PE, PBT, and PEEK each need grade-specific conditions. Filled, flame-retardant, recycled, colored, and medical grades may use different limits.
Drying and Moisture
Hygroscopic materials can hydrolyze at processing temperature, reducing molecular weight and strength even if the part looks acceptable. Confirm dryer temperature, dew point, time, airflow, and material handling.
Defects Linked to Temperature
Low temperature can cause short shots, hesitation, poor knit lines, dull surfaces, and high pressure. Excessive temperature can cause splay, gas, odor, discoloration, flash, sticking, or brittleness. Similar defects can also come from moisture, venting, speed, or mold temperature.
- Avoid changing several variables at once
- Record actual conditions and lot
- Check purge appearance and odor
- Review residence time and shot utilization
- Use a structured process study
Building a Process Window
Establish acceptable low and high boundaries for melt, fill speed, pack, cooling, and mold temperature. Validate critical dimensions and appearance across normal variation.
Design and Tooling Interaction
Thin walls, long flow paths, small gates, abrupt thickness changes, weak venting, and poor cooling may force an unnecessarily narrow thermal window. Improve part and mold design instead of relying on hotter material to solve every fill problem.
Quality Documentation
Record resin grade, lot, regrind policy, drying, machine, screw, zone settings, cycle, measured melt, mold temperature, pressure, and inspection results for controlled production.
Frequently Asked Questions
Is melt temperature the same as nozzle temperature?
No. Nozzle temperature is one setpoint; actual melt reflects barrel heating, shear, residence, and heat loss.
Should I use a universal temperature chart?
Charts provide orientation only. Use the exact resin supplier data and validate the process on the actual machine, mold, and part.
What happens if nylon is wet?
Moisture can create splay and hydrolytic degradation during melting, reducing strength. Proper drying and handling are essential.