Categories
Blog Design, Cost & Sourcing Machine Tools & Programming

How CNC Machining Software Improves Production Efficiency

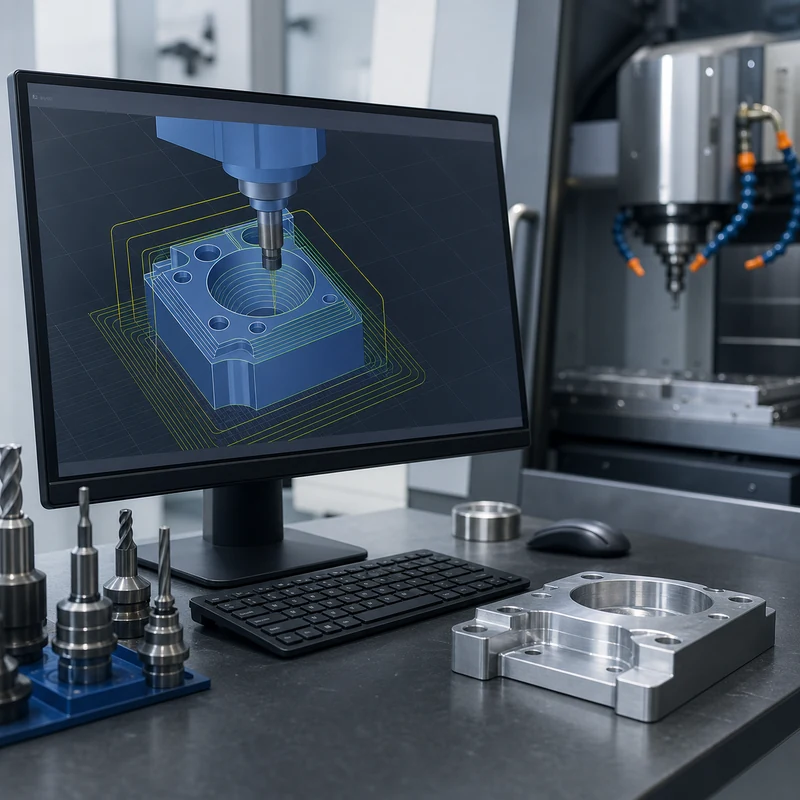
CNC machining software improves production efficiency by turning a CAD model into controlled toolpaths, repeatable setup instructions, reliable simulations, and measurable process data. Good software does not replace skilled machinists, but it gives programmers and production teams better ways to reduce waste, avoid collisions, shorten setup time, and standardize repeat jobs.

For custom parts, the software workflow matters as much as the machine itself. MTSPi uses digital review, programming, process planning, and quality assurance methods to connect design intent with real machining results.

Where CNC Software Fits in Production

Stage Software Role Efficiency Benefit
Design review Checks geometry, manufacturability, access, and missing drawing details Reduces quoting surprises and redesign loops
CAM programming Creates roughing, finishing, drilling, tapping, and contouring toolpaths Shortens programming time and standardizes best practices
Simulation Tests tool reach, holder clearance, stock removal, and machine motion Prevents crashes and wasted setups
Setup planning Defines fixtures, work offsets, tools, and operation sequence Reduces spindle idle time and operator confusion
Inspection feedback Connects measured results to process adjustments Improves repeatability across batches

Key Ways Software Improves Efficiency

Faster programming

Modern CAM systems let programmers reuse templates, tool libraries, feeds, speeds, machining strategies, and post-processors. This is especially useful when similar materials, hole patterns, pockets, or part families appear across multiple projects.

Better toolpath quality

Adaptive roughing, rest machining, high-speed finishing, and optimized entry moves can reduce cycle time while protecting cutters and workpieces. The goal is not simply to move faster; it is to keep tool engagement predictable and finish quality consistent.

Fewer setup errors

Digital setup sheets help operators understand stock size, vise orientation, fixture location, work offsets, tool numbers, inspection checks, and special notes. Clear setup information reduces avoidable mistakes during first article and repeat production.

Safer complex machining

For 5-axis machining, simulation is essential. Software helps verify rotary motion, toolholder clearance, machine limits, and approach angles before material is cut.

Software Does Not Eliminate Process Judgment

Efficient CNC production still depends on material behavior, tool condition, coolant, workholding rigidity, machine capability, inspection planning, and operator feedback. Software can suggest a path, but experienced manufacturing teams decide whether that path is stable, economical, and measurable.

Common Software Capabilities

  • CAD model import and geometry repair for machining preparation.
  • Tool library management with cutter length, diameter, holder, and material-specific data.
  • Automatic and manual toolpath generation for milling, turning, drilling, tapping, and finishing.
  • Collision checking between tool, holder, fixture, stock, and machine components.
  • Post-processing that outputs machine-specific CNC code.
  • Setup sheets and inspection plans for repeatable shop-floor execution.

Benefits for Buyers

Buyers may not see the CAM file, but they feel the result through quoting clarity, shorter lead times, consistent repeat orders, fewer part revisions, and better communication about difficult features. If a part has deep pockets, thin walls, tight bores, complex curves, or multiple setups, software-backed planning can make the difference between an unstable process and a controlled one.

Design Data That Helps Software Work Better

  • Send native 3D CAD when available, plus STEP files for neutral exchange.
  • Include a 2D drawing for threads, tolerances, surface finish, critical datums, and inspection notes.
  • Define material grade, quantity, finish, and application requirements.
  • Flag cosmetic surfaces and assembly interfaces before programming starts.
  • Tell the manufacturer whether prototype speed or production repeatability is the priority.

Related MTSPi Resources

FAQ

Is CAD the same as CAM?

No. CAD is used to create or modify the part model. CAM uses that model to generate machining toolpaths and CNC programs.

Can software reduce CNC machining cost?

Often, yes. Better toolpaths, fewer setups, reduced scrap, reusable templates, and clearer setup sheets can lower the total manufacturing effort.

Categories
Blog Machine Tools & Programming

Computer Numerical Control (CNC): Meaning, Process, Machines, and Uses

Quick answer: Computer numerical control, or CNC, means using a computer program to control machine movement. In machining, CNC controls tool position, spindle speed, feed rate, and cutting paths so metal or plastic parts can be produced accurately and repeatedly.

What Is Computer Numerical Control?

CNC is used because programmed movement is more repeatable than manual control. It helps manufacturers cut complex shapes, hold dimensions, repeat batches, and document the process more consistently.

Key Points for Buyers and Engineers

Topic What to know Practical impact
CNC meaning Computer numerical control Computer-controlled motion for manufacturing.
Machine axes X, Y, Z plus possible rotary axes Defines how tools and workpieces move.
Common machines Mills, lathes, routers, grinders, EDM equipment Different machines fit different part shapes.
Main outputs Holes, pockets, threads, slots, contours, faces Creates usable features from raw material.

How This Affects CNC Machined Parts

CNC is the control method behind many CNC machining services. It can support milling, turning, drilling, tapping, boring, engraving, and finishing preparation for custom parts.

Design and Purchasing Checklist

  • Use CNC when repeatability matters.
  • Choose milling for prismatic features and turning for round parts.
  • Give the supplier CAD files and clear tolerances.
  • Confirm material and finish before quoting.
  • Avoid over-tight tolerances on non-critical features.

Related MTSPi Resources

FAQ

What does CNC stand for?

CNC stands for computer numerical control.

Is CNC the same as machining?

No. CNC is the control method. Machining is the material-removal process.

What materials can CNC cut?

CNC machines can cut aluminum, steel, brass, copper, titanium, ABS, POM, nylon, PEEK, acrylic, and many other materials.

Need help with CNC process selection?

Send drawings, material, quantity, finish, tolerance notes, and application requirements. MTSPi can review manufacturability before quoting.

Contact MTSPi for engineering and quote support

Practical Buyer Notes

Computer numerical control is a broad term, so the page needs to connect the definition to real CNC machine behavior. Users should learn what the controller does, what axes mean, and how code becomes cutting movement.

For SEO, this page should also answer related beginner questions: what CNC stands for, whether CNC is automatic, how CNC differs from manual machining, and what CNC machines can make.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Controller Reads programmed instructions and coordinates movement Turns digital toolpaths into machine action
Axes Control movement in X, Y, Z and sometimes rotary directions Determines which geometry can be machined efficiently
Tooling Uses cutters, drills, taps, inserts, boring tools, and holders Tool choice affects quality and cost
Operator role Sets up workholding, tools, offsets, and inspection checks CNC still requires skilled manufacturing control

Common Mistakes to Avoid

  • Explaining CNC only as automation without discussing machining operations.
  • Ignoring the role of CAM programming and setup.
  • Suggesting CNC removes all human skill from manufacturing.
  • Not linking CNC meaning to real part examples.

Recommended MTSPi Review Workflow

MTSPi should use this page to move readers from definition to application. Once users understand CNC, they should be guided toward milling, turning, materials, tolerances, and RFQ preparation.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

For a CNC quote, send the part model, drawing, material, quantity, finish, tolerance expectations, and notes about how the part will be used.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Deeper Engineering Notes

For computer numerical control, the strongest page is not just a definition. It should help a buyer decide what information belongs on the drawing, what questions to ask a supplier, and which details affect cost, quality, and delivery. In real RFQ work, the important details are usually machine axes, controller instructions, CAM programs, work offsets, tool offsets, and operator setup. These details decide whether the supplier can quote confidently or has to return with repeated questions.

The common risk is thinking CNC is fully automatic without skilled setup, programming, and measurement. That risk can make the content look complete on the surface but weak in a real manufacturing situation. A stronger specification connects the topic to material behavior, machine access, tolerance control, finishing, and inspection before the order is released.

Example Specification Review

Review area Question to answer Good specification practice
Function What does this feature or part need to do? Describe the load, fit, motion, appearance, sealing, or assembly requirement.
Material Is the selected material suitable for the environment? Confirm strength, heat, corrosion, wear, chemical exposure, and cosmetic needs.
Geometry Can the feature be reached by standard tools? Review depth, corner radius, wall thickness, tool clearance, and setup direction.
Tolerance Which dimensions are truly critical? Use tight tolerances only where function requires them and keep general dimensions practical.
Verification How will acceptance be checked? Define gauges, CMM checks, roughness measurement, thread inspection, or visual standards when needed.

How This Page Should Support Ranking

This topic can attract both beginner searches and buyer searches. The beginner wants a clear answer; the buyer wants enough detail to make a manufacturing decision. A page has a better chance to rank when it answers the simple question first, then adds examples, process limits, design notes, comparison tables, and practical next steps.

That is also why internal links should be helpful rather than forced. A reader should naturally move from this page to a process page, material page, surface finish page, inspection page, or quote page only when that next step solves a real question.

Conclusion

Computer numerical control is the foundation of modern precision machining. It helps turn digital part data into consistent metal and plastic components.

Categories
Machine Tools & Programming

Drilling Machine Operation: Setup, Tools, Speeds, and Hole Quality

Drilling machine operation is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Drilling machine operation refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Drilling machine operation should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain drilling machine operation with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of drilling machine operation. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Drilling Machine Operation: Setup, Tools, Speeds, and Hole Quality

For the topic drilling machine operation, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for drilling machine operation because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Drilling Machine Operation: Setup, Tools, Speeds, and Hole Quality should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does drilling machine operation mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.


Categories
Machine Tools & Programming

Tapping vs Threading: Differences, Tools, Design Notes, and Inspection

Tapping vs threading is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Tapping vs threading refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Tapping vs threading should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain tapping vs threading with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of tapping vs threading. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Tapping vs Threading: Differences, Tools, Design Notes, and Inspection

For the topic tapping vs threading, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for tapping vs threading because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Tapping vs Threading: Differences, Tools, Design Notes, and Inspection should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does tapping vs threading mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Machine Tools & Programming

Drilling vs Milling: Difference, Tools, Holes, Slots, and Part Features

Drilling vs milling is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Drilling vs milling refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Drilling vs milling should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain drilling vs milling with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of drilling vs milling. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Drilling vs Milling: Difference, Tools, Holes, Slots, and Part Features

For the topic drilling vs milling, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for drilling vs milling because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Drilling vs Milling: Difference, Tools, Holes, Slots, and Part Features should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does drilling vs milling mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Machine Tools & Programming

Boring vs Drilling: Difference, Accuracy, Tools, and Use Cases

Boring vs drilling is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Boring vs drilling refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Boring vs drilling should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain boring vs drilling with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of boring vs drilling. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Boring vs Drilling: Difference, Accuracy, Tools, and Use Cases

For the topic boring vs drilling, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for boring vs drilling because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Boring vs Drilling: Difference, Accuracy, Tools, and Use Cases should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does boring vs drilling mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Machine Tools & Programming

Tapping Process: Internal Threads, Tools, Design Rules, and Checks

Tapping process is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Tapping process refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Tapping process should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain tapping process with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of tapping process. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Tapping Process: Internal Threads, Tools, Design Rules, and Checks

For the topic tapping process, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for tapping process because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Tapping Process: Internal Threads, Tools, Design Rules, and Checks should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does tapping process mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Machine Tools & Programming

Hole Making Process: Drilling, Boring, Reaming, Tapping, and Inspection

Hole making process is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Hole making process refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Hole making process should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain hole making process with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of hole making process. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Hole Making Process: Drilling, Boring, Reaming, Tapping, and Inspection

For the topic hole making process, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for hole making process because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Hole Making Process: Drilling, Boring, Reaming, Tapping, and Inspection should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does hole making process mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Machine Tools & Programming

Types of Drilling Machines: Bench, Pillar, Radial, and CNC

Types of drilling machines is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Types of drilling machines refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Types of drilling machines should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain types of drilling machines with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of types of drilling machines. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Types of Drilling Machines: Bench, Pillar, Radial, and CNC

For the topic types of drilling machines, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for types of drilling machines because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Types of Drilling Machines: Bench, Pillar, Radial, and CNC should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does types of drilling machines mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
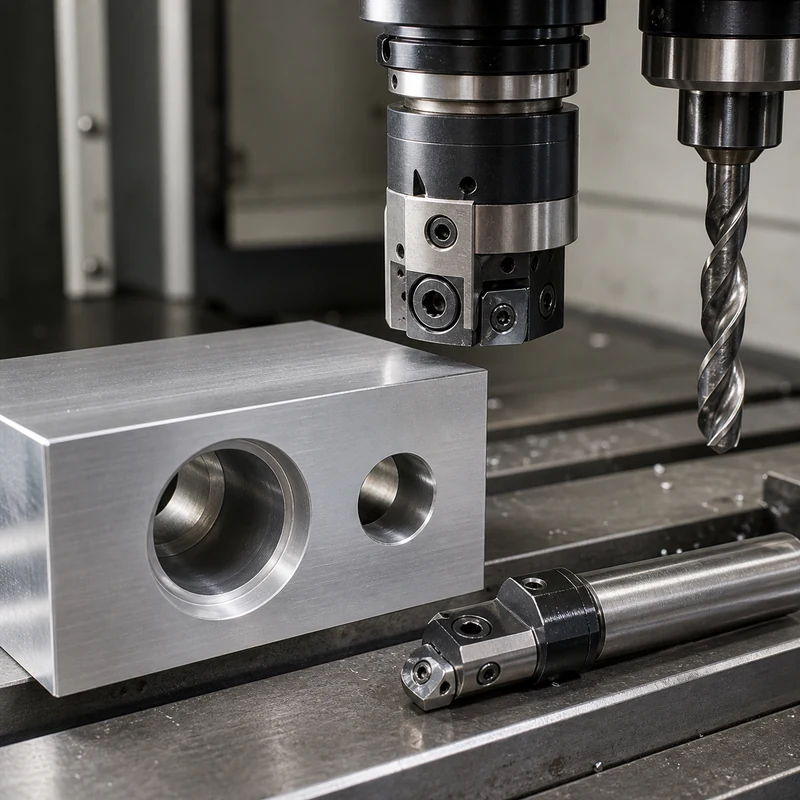
Categories
Machine Tools & Programming

What Is Drilling? Process, Tools, Hole Types, and Manufacturing Uses

What is drilling is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

What is drilling refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • What is drilling should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain what is drilling with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of what is drilling. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for What Is Drilling? Process, Tools, Hole Types, and Manufacturing Uses

For the topic what is drilling, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for what is drilling because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

What Is Drilling? Process, Tools, Hole Types, and Manufacturing Uses should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does what is drilling mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
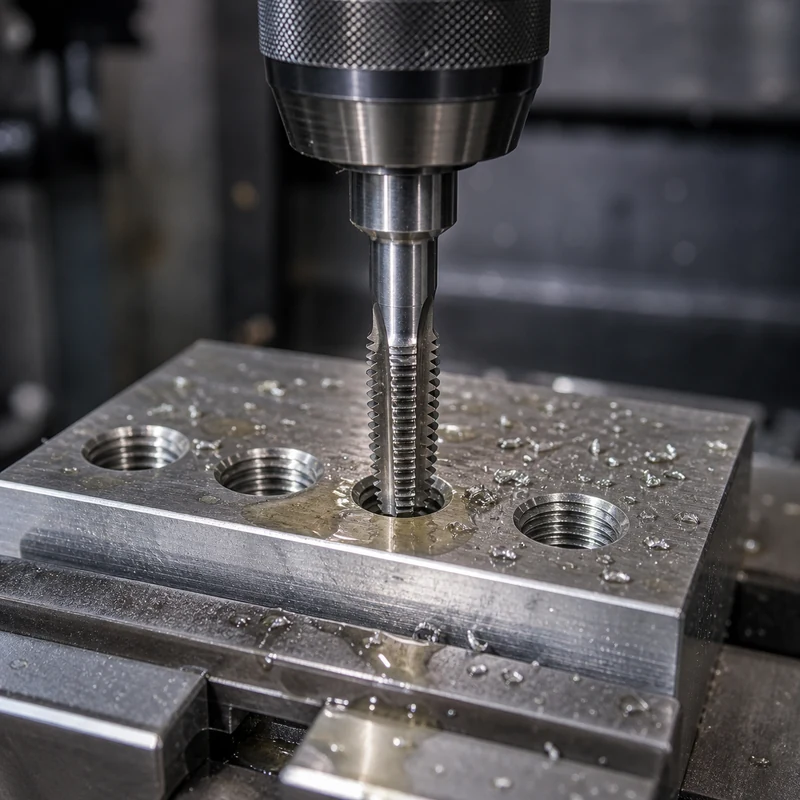
Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

What Is Drilling? Process, Tools, Hole Types, and Manufacturing Uses

We'll Send You Back with Price Immediately!