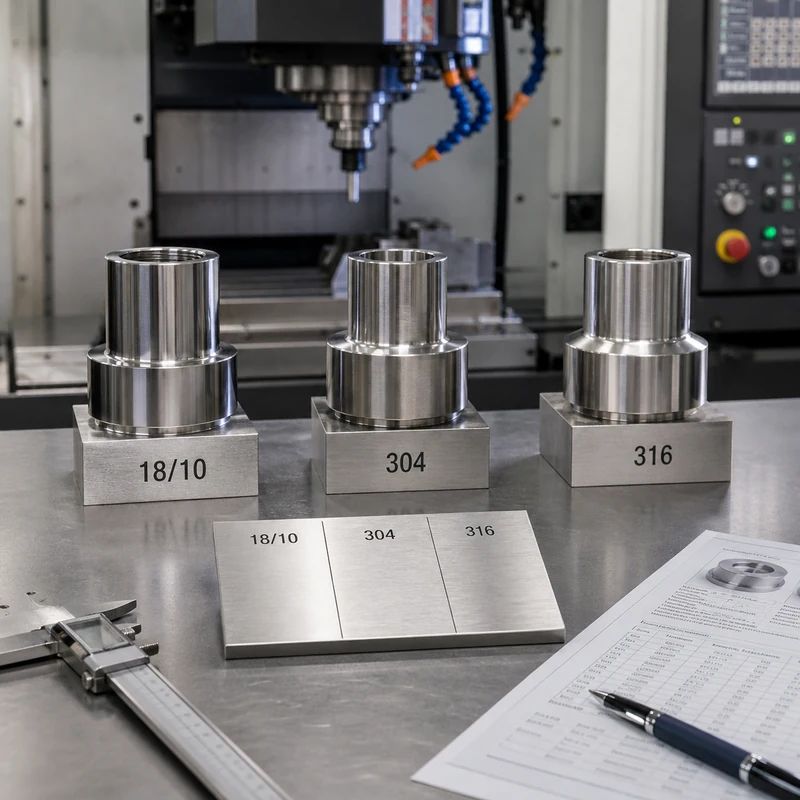
18/10, 304, and 316 stainless steel are often grouped together because all three are austenitic stainless options with useful corrosion resistance. For CNC machined parts, the practical question is not just which grade sounds better. The right choice depends on corrosion exposure, machining difficulty, material cost, surface finish, passivation needs, and inspection requirements. MTSPi supports stainless steel CNC machining for prototypes and production components where grade selection affects both performance and total cost.
Quick Answer: 18/10 vs 304 vs 316
18/10 stainless steel usually describes about 18 percent chromium and 10 percent nickel. It is close to the 304 stainless family and is common in food-contact and consumer applications. 304 is the common general-purpose stainless grade for industrial parts. 316 adds molybdenum, which improves resistance to chlorides, salt exposure, and pitting corrosion, but it normally costs more and requires more careful machining control.
| Material | Best Use | Main CNC Note |
|---|---|---|
| 18/10 stainless steel | Decorative, food-related, and consumer stainless parts | Confirm the actual certified grade if the drawing requires traceability |
| 304 stainless steel | General industrial brackets, shafts, housings, fittings, and food equipment | Usually easier and more economical to machine than 316 |
| 316 stainless steel | Marine, chemical, medical-style, pharmaceutical, and coastal components | Better corrosion resistance, with higher cost and tool-wear risk |
What 18/10 Stainless Steel Means
18/10 is a composition description. Chromium helps form the passive oxide film that protects stainless steel, while nickel stabilizes the austenitic structure and improves toughness and surface appearance. The term is useful for consumer goods, but it is not always precise enough for engineered CNC parts. If a component needs material certificates, regulated traceability, or a controlled standard, the drawing should call out the recognized stainless grade rather than only saying 18/10.
Why 304 Stainless Steel Is Common in CNC Parts
304 stainless steel is widely available and offers a strong balance of corrosion resistance, availability, formability, weldability, and cost. It is often the starting point for CNC metal machining when the part needs stainless performance but will not face heavy salt, chloride, or chemical exposure. It can still work harden and create stringy chips, so sharp tooling, coolant, and stable cutting parameters matter.
Where 316 Stainless Steel Performs Better
316 stainless steel is selected when corrosion risk is the leading concern. Its molybdenum content improves resistance to pitting and crevice corrosion in chloride-rich environments. That makes 316 a better candidate for marine hardware, washdown equipment, chemical processing components, medical-style instruments, outdoor assemblies, and parts that must tolerate aggressive cleaning. It is not automatically stronger or better for every part; its main advantage is corrosion resistance.
| Factor | 18/10 | 304 | 316 |
|---|---|---|---|
| Typical role | Commercial composition description | General-purpose stainless grade | Harsh-environment stainless grade |
| Chromium | About 18 percent | About 18 to 20 percent | About 16 to 18 percent |
| Nickel | About 10 percent | About 8 to 10.5 percent | About 10 to 14 percent |
| Molybdenum | Usually none | Usually none | About 2 to 3 percent |
| Corrosion resistance | Good in mild service | Good for general service | Best in chloride exposure |
| Machinability | Similar to 304-family grades | Usually better than 316 | More demanding |
| Cost | Often close to 304 | Usually lower | Usually higher |
Corrosion Resistance and Service Environment
The largest difference appears around chlorides. 304 can perform well indoors, in clean freshwater exposure, and in many general industrial assemblies. If the part sees salt water, coastal air, aggressive washdown, chemical cleaning, or trapped moisture, 316 is often safer. Geometry still matters: crevices, blind pockets, poor drainage, and scratches can reduce corrosion performance even when the alloy is well chosen.
| Environment | Likely Starting Grade | Reason |
|---|---|---|
| Dry indoor machinery | 304 | Severe corrosion resistance is usually unnecessary |
| Food-contact parts | 304 or 316 | Cleaning chemistry decides the better option |
| Coastal outdoor hardware | 316 | Chloride exposure increases pitting risk |
| Marine components | 316 | Salt exposure favors molybdenum-bearing stainless |
| Decorative consumer parts | 18/10 or 304-family stainless | Appearance and polish may matter more than extreme corrosion resistance |
CNC Machining Differences
Both 304 and 316 can be machined accurately, but neither should be treated like free-machining steel. Austenitic stainless generates heat, can work harden, and may form burrs around holes, threads, slots, and thin edges. 316 is generally more difficult because it is tougher and can increase tool wear. For tight-tolerance parts, the RFQ should define critical dimensions, surface roughness, edge requirements, and whether inspection is needed before or after finishing.
Surface Finish and Passivation
Stainless performance depends on the finished surface, not only the alloy. Machining marks, embedded contamination, sharp burrs, and poor cleaning can reduce corrosion resistance. Depending on the application, stainless parts may need passivation, electropolishing, brushing, polishing, bead blasting, or another surface treatment. Post-finish dimensions should be specified when polishing or electropolishing could affect a critical tolerance.
How to Choose for a CNC Machined Part
| Choose | When It Makes Sense | Check First |
|---|---|---|
| 18/10 | The part is cosmetic, consumer-facing, or food-related and certification is not critical | Whether a recognized 304-family grade will actually be supplied |
| 304 | The part needs general corrosion resistance, good availability, and reasonable cost | Exposure to chlorides, cleaning chemicals, and outdoor weather |
| 316 | The part faces salt, chemicals, medical-style cleaning, or corrosion-sensitive service | Higher material cost, machining time, and finish requirements |
RFQ Details That Prevent Material Mistakes
A complete RFQ helps the supplier quote the real requirement. Include the 3D model, 2D drawing, grade and standard, material certificate requirement, production quantity, finish, inspection level, and packaging needs. MTSPi’s CNC machining materials resources can help compare stainless steel with aluminum, brass, copper, titanium, and engineering plastics before the grade is locked.
Quality Checks for Stainless Parts
Material choice should connect directly to inspection. MTSPi can support dimensional checks, thread gauges, surface roughness review, visual inspection, and documentation through its quality assurance process. For corrosion-critical parts, finish certificates or passivation records may be just as important as dimensional results.
FAQ
Is 18/10 stainless steel the same as 304?
It is usually close to 304 in composition, but 18/10 is a composition description. Use a recognized grade callout when certification or traceability matters.
Is 316 always better than 304?
No. 316 is better for chloride, marine, chemical, and harsh cleaning exposure. For mild indoor or general industrial use, 304 may be more economical.
Which grade is easier to machine?
304 is generally easier to machine than 316. Both require sharp tools, coolant control, and appropriate cutting parameters to reduce work hardening and burrs.
Can MTSPi machine 304 and 316 stainless steel?
Yes. MTSPi can quote CNC milling, CNC turning, and multi-axis machining for stainless parts based on drawings, CAD files, quantity, finish, and inspection requirements.