Categories
Manufacturing Process Comparisons

Welding vs Machining: Differences, Tolerances, Costs, and Part Design

Welding vs machining is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Welding vs machining refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Welding vs machining should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain welding vs machining with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

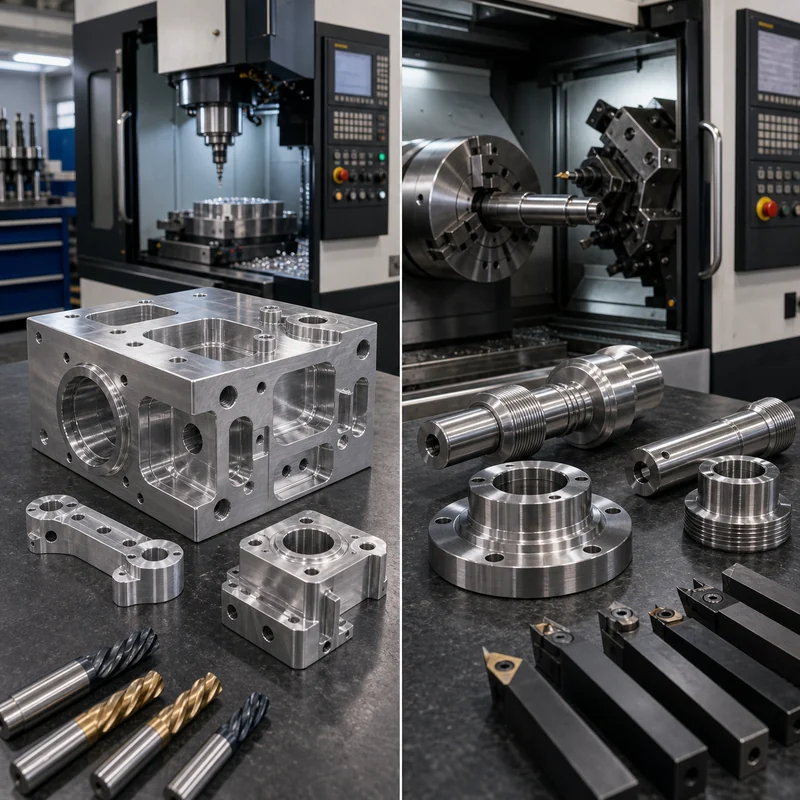
Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of welding vs machining. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Welding vs Machining: Differences, Tolerances, Costs, and Part Design

For the topic welding vs machining, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for welding vs machining because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Welding vs Machining: Differences, Tolerances, Costs, and Part Design should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does welding vs machining mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Manufacturing Process Comparisons

Sheet Metal vs Machined Parts: Design, Cost, Strength, and Tolerance

Sheet metal vs machined parts is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Sheet metal vs machined parts refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Sheet metal vs machined parts should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain sheet metal vs machined parts with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of sheet metal vs machined parts. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Sheet Metal vs Machined Parts: Design, Cost, Strength, and Tolerance

For the topic sheet metal vs machined parts, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for sheet metal vs machined parts because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Sheet Metal vs Machined Parts: Design, Cost, Strength, and Tolerance should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does sheet metal vs machined parts mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Manufacturing Process Comparisons

Die Casting vs CNC Machining: Cost, Tooling, Tolerance, and Quantity

Die casting vs cnc machining is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

Die casting vs cnc machining refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • Die casting vs cnc machining should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain die casting vs CNC machining with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of die casting vs CNC machining. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for Die Casting vs CNC Machining: Cost, Tooling, Tolerance, and Quantity

For the topic die casting vs CNC machining, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for die casting vs CNC machining because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

Die Casting vs CNC Machining: Cost, Tooling, Tolerance, and Quantity should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does die casting vs CNC machining mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Manufacturing Process Comparisons

3D Printing vs CNC Machining: Strength, Accuracy, Cost, and Prototypes

3d printing vs cnc machining is a practical question because the word is used in design reviews, RFQs, supplier audits, cost discussions, and quality reports. In manufacturing, it usually describes controlled material removal from metal or plastic stock to create a part with defined shape, dimensions, surface condition, and functional features. For buyers, the useful answer is not only the dictionary definition; it is how the process affects material choice, tolerance, lead time, finish, inspection, and supplier communication.

This guide combines common top-page coverage with CNC buyer details that are often missing: drawing requirements, process selection, cost drivers, inspection evidence, and realistic questions to ask before placing an order with MTSPi CNC / MEITESI.

Quick Answer

3d printing vs cnc machining refers to a manufacturing subject connected to cutting, shaping, or removing material with controlled tools. In CNC work, the main decision is how to turn a drawing or model into a repeatable part without overpaying for unnecessary tolerance, finish, or setup complexity. A buyer should start with the part function, then define material, quantity, critical dimensions, finish, and inspection requirements.

When a part needs milled faces, pockets, slots, holes, or 3D profiles, a process-specific review can help match the geometry to a practical route. When the part includes round features, shafts, threads, bushings, or sleeves, turning may be more efficient than forcing the work into a milling setup.

Key Takeaways

  • 3d printing vs cnc machining should be understood through part function, not only a short definition.
  • The same term can mean different things in engineering, purchasing, shop-floor planning, and inspection.
  • Material grade, tolerance, surface finish, and batch quantity often matter more than the process name.
  • A clear 2D drawing is still important even when a 3D model is available.
  • The best supplier questions focus on risk: workholding, tool access, burrs, finish, measurement, and repeatability.

Definition and Core Meaning

Most leading educational pages explain 3D printing vs CNC machining with a simple idea: controlled shaping of material into a desired part. That definition is useful, but it is incomplete for real sourcing work. A buyer also needs to know what will be held, where the cutting forces go, which surfaces are cosmetic, which dimensions control assembly, and what evidence proves the finished part is acceptable.

In a CNC project, the definition becomes more concrete. The process starts with a drawing, model, material, stock size, tools, fixtures, and inspection plan. If any of these are unclear, the quote may look fast but the project can still run into rework. MTSPi CNC reviews those details through drawing and model preparation before the machining route is finalized.

A useful way to think about the term is this: machining is not just cutting material away. It is a chain of decisions that includes programming, setup, tool selection, clamping, roughing, finishing, deburring, surface treatment, inspection, packaging, and communication. Each step can change cost and quality.

Question Simple answer Buyer detail that matters
What is being made? A part from raw material. The drawing should identify datums, threads, finish, tolerances, and critical surfaces.
How is material removed? By cutting tools or controlled energy. Tool access, chip control, heat, and workholding decide whether the process is stable.
What affects price? Machine time and material. Setup count, tolerance, finish, inspection, burr control, and quantity are often just as important.
How is quality confirmed? By inspection. Inspection should match the drawing risk with the right gauge, report, or sampling plan.

Main Process Categories

The most common process categories include milling, turning, drilling, boring, tapping, reaming, grinding, EDM, and finishing operations. Educational pages often list these as separate processes, but real parts often use several of them. A housing may need milling, drilling, tapping, deburring, bead blasting, and anodizing. A shaft may need turning, threading, grooving, polishing, and runout inspection.

Milling removes material with rotating cutters and is common for flat faces, pockets, slots, holes, and complex surfaces. Buyers can review CNC milling support when a part has prismatic geometry or multiple machined faces. Turning rotates the workpiece and is usually efficient for round parts, shafts, bushings, threaded pins, sleeves, and spacers; for these parts, CNC turning support may be the better starting point.

Drilling, boring, tapping, and reaming are hole-making or hole-finishing operations. They look simple on a drawing, but hole depth, thread engagement, position tolerance, burr direction, and access from one side or both sides can affect machining risk. Deep holes and small threaded holes deserve special attention before quoting.

A strong process choice also considers the order of operations. A hole drilled before milling may move slightly after material is removed around it. A thin wall roughed too aggressively may release stress and lose flatness. A cosmetic surface finished too early may be damaged during later clamping. These sequencing details are rarely visible in a simple definition, yet they are often the difference between a clean first batch and repeated correction.

Process Best suited for Common risk
Milling Flat faces, slots, pockets, 3D contours, hole patterns Long tool reach, vibration, internal corner radius, thin wall movement
Turning Shafts, bushings, sleeves, pins, threaded round parts Runout, concentricity, surface finish, slender-part deflection
Drilling and tapping Holes, threads, fastener locations Broken taps, wrong thread depth, burrs, poor position control
Grinding or fine finishing Tight surfaces and improved roughness Extra cost, measurement demand, and possible lead time increase

Materials and Manufacturing Considerations

Material choice changes nearly every part of 3D printing vs CNC machining. Aluminum usually machines quickly and accepts many finishes, but thin walls may deform and cosmetic surfaces need protection. Stainless steel is strong and corrosion resistant, but it can work harden and increase tool wear. Brass cuts cleanly, copper needs careful burr and heat control, titanium demands conservative cutting and cooling, and engineering plastics need heat management and gentle workholding.

For metal projects, metal machining choices gives a useful way to compare alloy behavior before the RFQ is finalized. For projects where aluminum is likely, buyers should think about 6061, 7075, anodizing, flatness, and cost. Stainless steel buyers should pay attention to 304 versus 316, burr behavior, passivation, and the cost impact of tight tolerances.

Material is not only a performance choice. It is also a supply-chain choice. Availability, stock shape, minimum order size, certificate requirements, and substitute-grade permission can all affect quote speed. Buyers should state whether equivalent materials are allowed or whether the listed grade is mandatory.

Material Why buyers choose it Machining note
Aluminum Light weight, good machinability, many finish options Thin walls and cosmetic faces need careful sequence and handling.
Stainless steel Corrosion resistance, strength, clean appearance Tool wear, burrs, and work hardening can raise cost.
Brass or copper Conductivity, appearance, thread quality, fittings Copper can be gummy; brass is easier but alloy choice still matters.
Engineering plastics Weight reduction, insulation, wear behavior Heat, clamping, and burr control are important.

Cost, Tolerance, and Surface Finish Factors

Cost is often misunderstood because buyers compare only the unit price. A quote also reflects programming, setup, material preparation, fixture design, tool life, cutting time, deburring, finish, inspection, packaging, and delivery risk. A low quote may hide missing assumptions, while a high quote may include inspection or finish work that another supplier ignored.

Tolerances should protect function rather than decorate every feature. Tight dimensions on noncritical surfaces add cost without improving performance. A better approach is to mark critical features clearly and allow standard tolerances elsewhere. MTSPi CNC can review machining cost reduction checks when buyers want to reduce price without weakening the part.

Surface finish also changes the process. A visible aluminum panel may need careful tool paths, deburring, polishing, bead blasting, or anodizing. A hidden bracket may only need safe edges and functional holes. Surface expectations should be discussed before machining, especially when a post-machining finish will be applied after cutting.

Tolerance and finish should also be separated by purpose. A sealing face, bearing seat, threaded hole, and decorative cover do not fail in the same way. A sealing face may need flatness and surface roughness control. A bearing seat may need diameter, roundness, and runout. A visible cover may need consistent texture and protected edges. A hidden mounting plate may only need hole position and deburred edges. This distinction helps buyers spend money where it protects function.

Factor Why it changes the quote How to control it
Tight tolerance Requires slower cutting, stable setup, and more inspection Apply it only to functional features.
Small batch Setup cost is spread over fewer parts Combine parts or request quantity breaks.
Complex finish Adds handling, protection, and rework risk Define visible and hidden surfaces separately.
Incomplete drawing Supplier must guess or ask repeated questions Send drawing, model, material, finish, and quantity together.

Design and Drawing Notes for Better Results

Good design makes the important features reliable. Internal corners should allow realistic cutter radius. Deep pockets should allow tool access. Thin walls need enough stiffness for cutting and finishing. Threads should have clear depth and class. Holes should show whether they are blind, through, tapped, reamed, or counterbored.

A 3D model gives geometry, but the 2D drawing gives manufacturing intent. It should identify datums, tolerances, surface roughness, thread callouts, finish requirements, revision level, and inspection notes. Without this, the supplier may produce the shape correctly but miss the real acceptance standard.

For prototype work, prototype machining review helps confirm fit and function before the design moves to a production order. For repeated small batches, fixture notes, approved samples, and inspection records should be kept with the job so later orders do not restart the learning process.

Common Mistakes to Avoid

  • Using a broad term without explaining the part’s function or assembly risk.
  • Sending only a model when threads, finish, tolerances, and critical features are needed.
  • Specifying tight tolerances on every dimension instead of only where fit or performance requires them.
  • Leaving surface finish until after the machining process is already fixed.
  • Comparing supplier quotes without checking whether material, finish, inspection, and packing assumptions match.
  • Approving a prototype without recording what changed before low-volume production.

Supplier and Quotation Checklist

A good RFQ package helps suppliers answer quickly and accurately. It should include the model, drawing, material, quantity, finish, target lead time, inspection requirement, and any special packaging need. If the part is used with another component, include a short note about the mating feature or failure concern.

A capable supplier should explain the process route, not only state that the part can be made. Ask about workholding, tool access, burr control, inspection, and finish sequence. The answer should be specific enough that an engineer can see how the part will be controlled before shipment.

RFQ item What to provide Why it helps
3D model STEP or other usable CAD format Supports programming and geometry review.
2D drawing Tolerances, datums, threads, finish, revision Shows manufacturing intent and acceptance rules.
Material Grade, temper, certificate need, substitute permission Controls performance, cost, and availability.
Quantity Prototype and production breaks Helps choose fixture and process strategy.
Inspection Critical dimensions and report needs Prevents disputes after delivery.

How to Use This Information in a Real RFQ

After reading a definition or comparison, buyers should turn the information into a short RFQ note. The note can be simple: part function, material preference, expected quantity, important mating features, visible surfaces, and delivery target. This small addition helps the supplier understand why certain features matter and where standard manufacturing variation is acceptable.

For example, instead of asking only for a price, a buyer can write that two bores locate bearings, the top face is visible after assembly, the threaded holes need repeated installation, and the first order is for functional testing. That kind of note guides process planning, inspection priority, and packaging protection without making the project more complicated.

Specific Notes for 3D Printing vs CNC Machining: Strength, Accuracy, Cost, and Prototypes

For the topic 3D printing vs CNC machining, the most useful article is one that begins with the general definition but quickly moves into practical manufacturing choices. The front-page results commonly explain the concept well, yet they often leave buyers without enough detail about drawings, tolerance, cost, finishing, inspection, and supplier communication.

The better approach is to connect the concept to part features. If the part has milled pockets, use milling logic. If it has round geometry, evaluate turning. If it needs a smooth visible finish, plan surface treatment early. If it has tight functional dimensions, decide the inspection method before accepting the quote.

This is why MTSPi CNC / MEITESI treats every request as a connected manufacturing problem rather than a single-word process label. A clear drawing, suitable material, realistic tolerance, and measurable quality standard make the finished part easier to quote, easier to produce, and easier to approve.

Practical Buyer Scenario

Consider a buyer who searches for 3D printing vs CNC machining because a new project has moved from concept to sourcing. The drawing shows a metal housing with two bearing bores, four mounting holes, a visible top surface, and a note calling for black finish. A basic educational explanation may help the buyer understand the term, but it will not answer the real purchasing questions: which faces are datums, whether the bores need inspection reports, whether the finish changes dimensions, and how the supplier will protect the visible surface during shipping.

In that situation, the buyer should not ask only whether the supplier can machine the part. A better request is to ask for a review of stock material, setup count, bore measurement, edge break, surface finish route, and packaging. If the housing is still being tested, prototype machining review can help confirm geometry before repeat orders. If the order will move into small batches, the buyer should ask which setup details can be reused and which dimensions need routine reporting.

This scenario shows why information articles should lead into real manufacturing decisions. The reader may begin with a broad question, but the project succeeds only when the definition becomes a drawing, a process route, a material order, a controlled finish, and an inspection method. That is the bridge between learning a term and buying usable parts.

Conclusion

3D Printing vs CNC Machining: Strength, Accuracy, Cost, and Prototypes should be understood as a practical manufacturing topic, not just a short definition. Buyers should use the concept to make better decisions about process selection, materials, tolerances, finish, cost, inspection, and supplier communication. With a clear RFQ package and a supplier that explains the route before production, MTSPi CNC / MEITESI can help turn general manufacturing knowledge into reliable machined parts.

FAQ

What does 3D printing vs CNC machining mean in manufacturing?

It generally refers to a controlled way of shaping material, often by removing material with tools or machine processes. In CNC work, the meaning also includes programming, setup, workholding, finishing, and inspection.

What information should I send for a CNC quote?

Send a 3D model, 2D drawing, material grade, quantity, finish requirement, critical dimensions, thread notes, and any assembly concerns.

Is CNC machining always the best process?

No. It is excellent for precision parts, prototypes, low-volume production, metal components, and many plastic parts, but casting, forming, molding, or fabrication may suit some designs better.

Why do machining costs vary so much?

Costs vary because material, setup count, tolerance, finish, inspection, tooling, batch size, and lead time can change the real work behind the same-looking part.

How can buyers reduce machining risk?

Clarify drawings, mark critical features, choose suitable materials, avoid unnecessary tight tolerances, define finish expectations, and request inspection evidence that matches the part function.
Categories
Manufacturing Process Comparisons

Machining vs Manufacturing: Difference, Examples, and How to Choose a Process

Quick answer: Machining is a manufacturing process, but manufacturing is the broader term. Manufacturing includes machining, casting, molding, stamping, forming, welding, 3D printing, finishing, inspection, and assembly. Machining specifically means removing material to create a required shape or feature.

The Simple Difference

Manufacturing is the complete activity of making products or parts. Machining is one way to manufacture parts. A company may manufacture a product using machined components, sheet metal, molded plastic, purchased hardware, surface finishing, and final assembly.

Machining vs Manufacturing Comparison

Topic Machining Manufacturing
Scope One production method All methods used to make a product
Main action Removes material from a workpiece May remove, form, join, mold, cast, print, finish, or assemble
Examples Milling, turning, drilling, tapping Machining, molding, casting, welding, forming, assembly
Best for Precise parts, prototypes, low-volume runs, functional features Complete product creation from design to delivery

Where CNC Machining Fits

CNC machining is often used inside a larger manufacturing plan. For example, a machine may require milled aluminum plates, turned shafts, sheet metal guards, purchased bearings, surface-treated parts, and final assembly. MTSPi focuses on the machined component side through CNC machining services.

When Machining Is the Right Manufacturing Choice

  • The part needs tight dimensions or controlled mating surfaces.
  • The quantity is too low for mold tooling.
  • The prototype must use real engineering material.
  • The design includes holes, pockets, threads, bores, or precise faces.
  • The part needs inspection documentation before assembly.

When Another Manufacturing Process May Be Better

Casting, molding, stamping, forming, extrusion, or 3D printing may be better when the part has very high production volume, thin formed geometry, complex internal channels, or a shape that would waste too much material if machined from billet.

How Buyers Should Choose

Start with part function, quantity, material, tolerance, finish, lead time, and budget. If the part needs real material strength and accurate features, machining is often a strong route. If surface appearance or corrosion resistance matters, review finishing options at the same time.

FAQ

Is machining part of manufacturing?

Yes. Machining is one category within manufacturing.

Is CNC machining only for prototypes?

No. CNC machining is used for prototypes, bridge production, custom parts, replacement parts, and production runs.

Is 3D printing manufacturing or machining?

3D printing is manufacturing, but it is not machining because it adds material instead of removing it.

Which process is cheaper?

It depends on quantity, geometry, material, tooling, tolerance, and finish. CNC is often cost-effective for prototypes and low-volume precision parts.

Need help choosing a machining route?

Send MTSPi your drawing, material, quantity, finish, and inspection requirements. We will review the part for manufacturability before quoting.

Contact MTSPi for a CNC machining quote

Practical Buyer Notes

This page should help users understand scope. Manufacturing is the full activity of making products, while machining is one method inside manufacturing. That difference matters when a buyer is trying to choose a supplier.

A CNC machining supplier may be ideal for precision components, but a complete product may also require sheet metal, molding, casting, finishing, assembly, purchased hardware, and packaging. The page should explain where MTSPi fits in that larger chain.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
User intent Clarify terminology first Satisfies informational search quickly
Process scope Show machining as a subset of manufacturing Avoids confusion between broad and narrow terms
Supplier fit Explain when CNC suppliers are the right partner Improves conversion quality
Next step Link to services, materials, and contact Moves readers toward project review naturally

Common Mistakes to Avoid

  • Making the article a generic business definition with no manufacturing examples.
  • Failing to explain CNC machining as one practical manufacturing route.
  • Not comparing machining with molding, casting, forming, welding, and 3D printing.
  • Leaving out cost and volume considerations.

Recommended MTSPi Review Workflow

MTSPi should treat this page as a bridge from education to supplier selection. The page should answer the difference, then guide readers to choose a manufacturing route by material, quantity, tolerance, and part geometry.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

A useful RFQ should explain whether the buyer needs only machined parts or a broader manufacturing package including finishing, assembly, or inspection documentation.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Real-World Example: One Product Can Use Many Manufacturing Methods

A small industrial device may include a CNC milled aluminum housing, CNC turned stainless steel shafts, sheet metal covers, injection molded plastic buttons, purchased bearings, laser-marked labels, and final assembly. In that case, machining is only one part of the manufacturing plan, but it may be the most important part for accuracy and fit.

This is why buyers should describe the full product context even when they only need a machined component. Knowing how the part will be assembled helps the supplier understand which faces, holes, threads, and surfaces are truly critical.

Conclusion

Machining and manufacturing are related but not identical. Manufacturing is the whole production picture; machining is a precise material-removal method inside that picture. Understanding the difference helps buyers choose the right supplier and process for each part.

Categories
Manufacturing Process Comparisons

CNC Milling vs CNC Turning: Which Process Do You Need?

CNC milling vs CNC turning is a key search topic for buyers who need reliable custom parts, accurate dimensions, practical material advice, and clear supplier communication. Before sending a drawing or placing an order, buyers should understand the process, cost drivers, tolerance requirements, material options, lead time, inspection needs, and the questions that separate a capable machine shop from a weak supplier.

How CNC Milling Works

CNC milling uses rotating cutting tools to remove material from a stationary or moving workpiece. It is ideal for slots, pockets, holes, flat surfaces, contours, and complex shapes.

Buyer Notes

For a smoother quote, prepare a 3D model, 2D drawing, target material, order quantity, surface finish, tolerance requirements, and any critical assembly information. Clear specifications reduce delays and help the supplier identify manufacturability risks early.

How CNC Turning Works

CNC turning rotates the workpiece while cutting tools shape the outside or inside diameter. It is best for shafts, pins, bushings, rings, spacers, and other round parts.

Buyer Notes

For a smoother quote, prepare a 3D model, 2D drawing, target material, order quantity, surface finish, tolerance requirements, and any critical assembly information. Clear specifications reduce delays and help the supplier identify manufacturability risks early.

Parts That Need Both

Many precision parts need turning first and milling second. Examples include shafts with flats, threaded parts with cross holes, and round parts with keyways.

Buyer Notes

For a smoother quote, prepare a 3D model, 2D drawing, target material, order quantity, surface finish, tolerance requirements, and any critical assembly information. Clear specifications reduce delays and help the supplier identify manufacturability risks early.

How to Choose

Choose based on geometry first. Round symmetrical parts usually start with turning. Boxy, flat, or multi-feature parts usually need milling.

Buyer Notes

For a smoother quote, prepare a 3D model, 2D drawing, target material, order quantity, surface finish, tolerance requirements, and any critical assembly information. Clear specifications reduce delays and help the supplier identify manufacturability risks early.

FAQ

What is the difference between CNC milling and CNC turning?

For CNC milling vs CNC turning, the right answer depends on part geometry, material, tolerance, surface finish, quantity, and end-use requirements. A complete RFQ helps the supplier give a useful recommendation.

When should I use CNC milling?

For CNC milling vs CNC turning, the right answer depends on part geometry, material, tolerance, surface finish, quantity, and end-use requirements. A complete RFQ helps the supplier give a useful recommendation.

When should I use CNC turning?

For CNC milling vs CNC turning, the right answer depends on part geometry, material, tolerance, surface finish, quantity, and end-use requirements. A complete RFQ helps the supplier give a useful recommendation.

Can one part require both milling and turning?

For CNC milling vs CNC turning, the right answer depends on part geometry, material, tolerance, surface finish, quantity, and end-use requirements. A complete RFQ helps the supplier give a useful recommendation.

Practical Checklist Before Ordering

  • Confirm material grade, dimensions, tolerance, and surface finish.
  • Share both 3D files and 2D drawings when possible.
  • Identify critical features that affect fit, sealing, strength, or assembly.
  • Ask about sample lead time, MOQ, inspection reports, and packaging.
  • Compare quotes by specification, not only by unit price.

Conclusion

A good CNC machining decision balances design, material, tolerance, cost, lead time, and supplier capability. Buyers who prepare complete files and ask the right technical questions usually receive more accurate quotes, better parts, and fewer production surprises.

Categories
Manufacturing Process Comparisons

CNC Machining vs. Extrusion: Which Process Is Right for Your Project?

Choosing between CNC machining and extrusion can be tricky. Both are fantastic for creating metal and plastic parts, but they work in very different ways. This guide will walk you through the basics of each process, their strengths, and typical uses to help you decide which one fits your project best.

Comparing Manufacturing Methods: CNC Machining and Aluminum Extrusion

When you’re looking into CNC machining vs extrusion, it’s like comparing a sculptor to a pastry chef. One carves away from a solid block, while the other pushes material through a shaped die. Both methods, including subtractive manufacturing (CNC) and profile extrusion, are pillars of modern fabrication. Let’s break down how each one operates.

What is CNC Machining?

CNC machining is a subtractive manufacturing process. Imagine you have a solid block of metal or plastic (we call this a “blank” or “workpiece”). A computer-controlled machine uses cutting tools to precisely remove material, layer by layer, until the final part is revealed. It’s incredibly versatile, allowing for complex 3D shapes, tight tolerances, and excellent surface finishes. Common searches like how does CNC milling work or precision machining services often lead people to discover this method’s capabilities for prototypes and end-use parts.

What is Extrusion?

Extrusion, particularly aluminum extrusion, is a forming process. Here, a material (usually aluminum) is heated and forced through a shaped opening called a die. Think of it like squeezing playdough through a mold—the material takes on the continuous cross-sectional profile of that die. This process is fantastic for creating long, consistent shapes like rails, frames, and tracks. If you’ve ever wondered what is aluminum extrusion used for, look at window frames or structural components—they’re classic examples.

Key Differences Compared

Now that we know how they work, let’s put them side-by-side. The choice often boils down to your project’s specific needs in terms of material, design, and budget.

Material and Starting Form

CNC machining typically starts with a solid block, billet, or bar stock. You can machine a wide range of materials, from metals like aluminum and steel to various plastics. Extrusion, on the other hand, primarily works with materials that can be pushed through a die when heated—aluminum is the superstar here, but plastics like PVC are also common. The starting point for extrusion is usually cylindrical billets of these softer, more malleable materials.

Design Complexity and Geometry

This is a major differentiator. CNC is your go-to for complex, intricate, and fully three-dimensional parts. Need internal channels, undercuts, or highly detailed features? CNC milling and turning can handle it. Extrusion is ideal for parts with a constant 2D cross-section that runs along a length. It’s perfect for linear shapes. While you can do some secondary CNC machining on extruded profiles to add holes or features, the core geometry comes from that die.

Cost and Lead Time Considerations

For low to medium volumes of complex parts, CNC can be cost-effective because there’s no expensive tooling—just digital instructions. However, material waste (chips from cutting) can add cost. Extrusion requires a custom die, which is an upfront investment. But once that’s made, producing long runs of the profile becomes very economical per part. So, for a one-off prototype, CNC often wins on speed and cost. For a long production run of a simple shape, extrusion is usually the better cost-effective manufacturing choice.

Which Process is Right for Your Project?

So, how do you choose? Let’s make it practical. I often advise clients to start by sketching their part and asking a few key questions about its use and volume.

When to Choose CNC Machining

Opt for computer numerical control machining when your part has complex geometries, requires very tight tolerances (±0.001 inches or better), or needs to be made from a specific, hard-to-extrude material. It’s perfect for prototypes, custom fixtures, low-volume production, and parts that are fully 3D. If you’re searching for rapid prototyping services, you’ll likely be looking at CNC or 3D printing. For instance, a client of mine needed a custom sensor housing with intricate internal mounts—CNC was the only way to go.

When to Choose Extrusion

Choose metal extrusion or plastic extrusion when you need a long, linear part with a uniform cross-section. It’s ideal for structural components, frames, enclosures, and heat sinks. If you plan to produce thousands of feet of the same profile, the low per-part cost after the initial die is made is unbeatable. A great resource to understand standardized profiles is the Aluminum Association’s design standards. For example, if you’re building a modular frame system, extrusion allows for easy integration and consistent parts.

Clearing Up Common Misconceptions

Let’s tackle a couple of myths I hear often. First, some think extrusion is only for simple shapes and can’t be precise. While the initial profile is limited, you can achieve high precision through careful die design and secondary machining. Second, people sometimes believe CNC is always more expensive. For one-off parts, it’s often cheaper! The real cost in extrusion is the die. Finally, these processes aren’t always rivals. Many successful projects use both: an extruded aluminum profile for the main structure, with precision CNC machined brackets and connectors attached. The best choice depends on your specific design, material, and production goals.

Categories
Manufacturing Process Comparisons

CNC Machining vs Sheet Metal: Which Process Wins for Your Project?

Choosing between CNC machining and sheet metal fabrication can be tricky. This friendly guide breaks down each process, from material removal to metal bending, to help you decide which manufacturing method is the winner for your specific part’s needs, budget, and timeline.

Understanding the Basics: Two Different Philosophies

Let’s start with a simple analogy. Imagine you’re a sculptor. CNC machining is like starting with a solid block of marble and carefully carving away everything that isn’t your statue. Sheet metal fabrication, on the other hand, is more like working with clay—you start with a flat, pliable sheet and bend, cut, and join it to form your final shape. Both are fantastic for creating metal parts, but they follow completely different rules from the get-go.

What is CNC Machining?

CNC (Computer Numerical Control) machining is a subtractive manufacturing process. You begin with a solid block of material—like aluminum, steel, or plastic—and a computer-controlled machine uses cutting tools to remove material until the desired part is created. It’s incredibly precise and can produce parts with complex geometries, tight tolerances, and excellent surface finishes. Think of engine components, intricate brackets, or custom gears. The American Society of Mechanical Engineers (ASME) provides extensive standards for the precision involved in these processes, which you can explore here.

What is Sheet Metal Fabrication?

Sheet metal forming, or simply sheet metal work, is a family of additive and formative processes. It involves transforming thin, flat sheets of metal (the “sheet metal”) into parts through cutting (like laser or punch), bending, stamping, and assembling (often with welding or rivets). This method is fantastic for creating enclosures, chassis, brackets, and ductwork—essentially, parts that are often hollow or box-like. It’s typically faster and more cost-effective for thin-walled structures.

Head-to-Head Comparison: Where Each Process Shins

So, in the debate of CNC milling vs sheet metal fabrication, how do you pick a side? It really comes down to your project’s specific needs. Let’s put them side-by-side on key factors.

Strengths of CNC Machining

Complexity & Precision: If your part has intricate 3D contours, deep pockets, or requires ultra-tight tolerances (think within thousandths of an inch), CNC is your champion. It excels at creating solid, highly detailed components from a single block.

Material Versatility: While both work with metals, CNC machining can also handle a wider range of solid materials, including various plastics and composites, right from the same machine.

Strength & Solid Parts: Because the part is milled from a solid block, it has consistent material strength throughout, with no seams or welds that could be potential weak points.

Strengths of Sheet Metal Work

Speed & Cost for Thin Parts: Need a prototype enclosure by next week? For thin, relatively simple shapes, sheet metal processes like laser cutting and bending are often much faster and cheaper than machining a hollow part from a solid block. The Fabricators & Manufacturers Association, Intl. discusses the efficiencies of modern fabrication here.

Weight Efficiency: By its nature, sheet metal creates lightweight, hollow structures—perfect for applications where saving every ounce matters, like in aerospace or portable electronics.

Scalability: Once the tools (like dies for stamping) are made, churning out thousands of identical sheet metal parts becomes very efficient and cost-effective, making it ideal for high-volume production.

Making the Right Choice for Your Project

Okay, let’s get practical. How do you, as someone looking for the best manufacturing method, make the call? I always suggest asking these questions:

What does the part look like? Is it a dense, solid component with complex curves (leaning toward CNC)? Or is it a housing, panel, or bracket made from thin metal (leaning toward fabrication)?

What’s the budget and timeline? For one-off prototypes or very complex parts, CNC might be more straightforward. For simpler, flat or bent parts in higher quantities, sheet metal fabrication often wins on cost and speed.

What are the strength requirements? Does the part need to be a solid chunk of metal, or is a formed and welded structure strong enough?

Sometimes, the winner isn’t one or the other! It’s common to see hybrid parts where a critical mounting feature is precision machined onto a larger, cost-effective sheet metal frame.

Clearing Up Common Misconceptions

I’ve chatted with many engineers and product developers, and a few myths always pop up. Let’s clear the air.

Myth 1: “CNC is always more expensive. Not true for complex, one-off parts! Machining that part from solid might be more economical than paying for multiple sheet metal setups, custom tooling, and assembly labor.

Myth 2: “Sheet metal parts aren’t precise. Modern laser cutters and press brakes are extremely accurate. While tolerances might differ from machining, they are more than sufficient for countless applications.

Myth 3: “You have to choose only one. As mentioned, combining processes is a smart strategy. Use sheet metal for the main body and CNC for critical interfacing features. This is a key consideration in mechanical design for manufacturing.

Final Thoughts: It’s About the Right Tool for the Job

So, which process wins in the battle of subtractive vs formative manufacturing? The real answer is that there’s no single winner—it depends entirely on your project’s goals. Think of CNC machining and sheet metal fabrication as two powerful tools in your manufacturing toolbox. One is a precision scalpel for solid, complex shapes; the other is a versatile set of shears and pliers for efficient, lightweight forms.

My best advice? Don’t get stuck on choosing just one. Sketch your part, define your requirements for strength, quantity, and budget, and then have a conversation with a knowledgeable manufacturing partner. Often, the best solution comes from understanding the strengths of both worlds. Good luck with your project!

Categories
Manufacturing Process Comparisons

CNC Machining vs Die Casting: Which is Best for Your Project?

Choosing between CNC machining and die casting can be a pivotal decision for your manufacturing project. This guide breaks down the key differences in process, materials, cost, and applications to help you select the best method for your specific needs, whether you need a few precise prototypes or thousands of identical parts.

Understanding the Core Processes

Let’s start by getting a clear picture of what each manufacturing technique actually involves. Think of it like choosing between carving a sculpture from a block of wood versus pouring molten metal into a mold. They achieve similar ends but through completely different means.

What is CNC Machining?

CNC machining, or Computer Numerical Control machining, is a subtractive manufacturing process. It starts with a solid block of material—like aluminum, steel, or plastic—and uses cutting tools to remove material, carving out the final part. It’s incredibly precise, controlled by computer programs (G-code), which is why it’s also referred to as CNC milling or precision machining. I often tell people it’s like a highly skilled, robotic sculptor that can create incredibly complex geometries with tight tolerances directly from a digital file.

What is Die Casting?

Die casting, on the other hand, is a formative process. It involves forcing molten metal—typically zinc, magnesium, or aluminum alloys—under high pressure into a reusable steel mold called a die. Once the metal cools and solidifies, the die opens to eject the part. This method is fantastic for producing high volumes of parts with excellent surface finish and consistent detail. You might also hear it called pressure die casting or metal injection molding when discussing similar high-pressure molding techniques for metals.

Key Differences: A Side-by-Side Look

Now that we know how they work, let’s compare them directly across some of the most important factors you’ll consider for your project. This comparison between subtractive and additive manufacturing (though die casting isn’t additive in the 3D printing sense) really highlights their unique strengths.

Materials and Tolerances

This is a major differentiator. CNC machining services offer incredible material flexibility. You can work with virtually any machinable metal, plastic, and even some composites. This makes it perfect for functional prototypes that need to match the final material’s properties. More importantly, CNC is the king of precision. It can hold tolerances within ±0.001 inches or even tighter, which is crucial for aerospace or medical components.

Die casting is primarily for non-ferrous metals. While it can produce parts with good dimensional accuracy, it generally can’t match the ultra-tight tolerances of CNC due to factors like metal shrinkage during cooling. Its strength lies in replicating complex shapes and fine surface details consistently across thousands of parts.

Cost and Production Volume

Here’s where the choice often becomes clear. The cost structure is opposite. CNC machining has low upfront costs—you just need the material and machine time. However, the cost per part remains relatively high and constant. It’s ideal for low-volume production and prototypes.

Die casting has very high initial costs because designing and manufacturing the hardened steel dies is complex and expensive. But once that die is made, the cost per part plummets. This makes it exceptionally economical for high-volume manufacturing. So, if you’re asking “should I use machining or casting for mass production?”, die casting usually wins on cost after a certain quantity threshold.

Lead Time and Design Flexibility

Need a part next week? CNC is your friend. Since there’s no tooling to make, lead times are short, often just a few days. It also offers maximum design flexibility; you can change the CAD file and machine a new version almost immediately.

Die casting requires several weeks to months for die design, fabrication, and testing. Making changes to the part design later usually means modifying or replacing the expensive die, which is a big deal. A common question is about die casting vs machining for complex parts. While dies can create complex shapes, undercuts and internal features are more challenging and costly than with CNC.

Choosing the Right Method for Your Project

So, how do you decide? It boils down to your project’s specific needs. Let’s walk through some typical scenarios to point you in the right direction.

When to Choose CNC Machining

Choose CNC machining if:

  • You need prototypes or a small batch of parts (1 to 100s of units).
  • Your design is still evolving, or you need the flexibility for custom one-offs.
  • You require extremely tight tolerances and superior surface finishes from the get-go.
  • Your part is made from an engineering plastic or a metal not suitable for casting.
  • Lead time is critical, and you need parts fast for testing or a pilot run.

In short, for rapid prototyping and low to medium volume needs, CNC is often the most practical and cost-effective route.

When to Choose Die Casting

Choose die casting if:

  • Your production volume is high (1,000s to millions of units).
  • The part design is finalized and unlikely to change.
  • You need thin walls, complex shapes with good detail, and a smooth surface finish “as-cast.
  • The part is suitable for metals like aluminum, zinc, or magnesium.
  • Reducing secondary operations (like extensive machining) is a priority for the final unit cost.

It’s the go-to for mass production of metal components like automotive housings, gearbox cases, or consumer electronics frames.

Clearing Up Common Misconceptions

I’ve seen a few myths pop up over the years. One big one is that die casting is always cheaper. It’s only cheaper *per part* at high volumes; for a few pieces, the die cost makes it prohibitively expensive. Another is that CNC parts are weaker. Not true! A machined part from a solid billet often has superior mechanical properties compared to a cast part, which can have internal porosity. Finally, some think you must choose one or the other. In reality, many projects use both! A part might be die cast to get the basic shape efficiently and then have critical features finished with CNC milling to achieve the required precision—a perfect hybrid approach.

Final Thoughts and Next Steps

There’s no single “best” process, only the best one for your specific project. Ask yourself about volume, budget, timeline, material, and required precision. For prototypes and complex, low-volume parts, CNC machining offers unbeatable flexibility and speed. For high-volume runs of metal parts, die casting provides unbeatable economy and consistency.

My advice? If you’re working on a prototype or small batch, start with a CNC machining service to validate your design. If mass production is the goal, use CNC for your prototypes and pre-production runs, then invest in die casting tooling for the full-scale manufacturing. For deeper technical details on materials and processes, reputable sources like the ASM International handbook or the Engineer’s Edge manufacturing guides are fantastic resources. Good luck with your project

Categories
Manufacturing Process Comparisons

CNC Machining vs Laser Cutting: Which Is Best for Your Project?

Choosing between CNC machining and laser cutting can be tricky. This guide breaks down their core differences, strengths, and ideal applications in a friendly, easy-to-understand way, helping you pick the perfect process for your next project.

Understanding the Basics

Let’s start by getting to know our two contenders. Think of it like choosing between a master sculptor and a master calligrapher—both are incredibly skilled, but they create in fundamentally different ways. Understanding these subtractive manufacturing methods is the first step to making a great choice.

What is CNC Machining?

CNC machining, short for Computer Numerical Control machining, is like a super-precise, automated carving tool. A computer program guides cutting tools (like drills and end mills) to selectively remove material from a solid block, known as a workpiece or blank. This CNC milling and turning process is fantastic for creating complex 3D shapes, threads, and parts with tight tolerances. It’s the go-to method for functional prototypes, engine components, and intricate enclosures.

What is Laser Cutting?

Laser cutting, on the other hand, is a form of sheet metal fabrication that uses a highly focused beam of light to melt, burn, or vaporize material along a defined path. It’s exceptionally good at cutting flat, 2D shapes from sheet materials with incredible speed and a clean edge. When people search for laser cutting services near me, they’re often looking to create precise panels, brackets, decorative art, or architectural models from materials like steel, acrylic, or wood.

Key Differences Explained

Now that we know what they are, let’s dive into the nitty-gritty. The core differences between these precision manufacturing techniques come down to how they interact with material, what shapes they can make, and what they can cut. This is where your project’s needs really start to point you in one direction.

Material Removal vs. Material Separation

This is the most fundamental difference. CNC machining is a subtractive process; it carves away material to reveal the final part, which can mean more waste (chips and shavings). Laser cutting is a thermal separation process; it slices through material with a thin kerf (the width of the cut), generally creating less waste from the sheet itself. It’s the difference between sculpting a statue from marble versus using a cookie cutter on dough.

Dimensional Capabilities

Here’s a big one: dimensionality. CNC milling services excel at true 3D fabrication. They can create pockets, holes, curved surfaces, and complex geometries on multiple axes. Laser cutters primarily work in 2D, creating flat parts. While some systems can etch or mark on a surface, they don’t typically create significant 3D relief like a CNC machine can. For a great visual comparison of capabilities, you can check out this resource from Engineering.com.

Material Compatibility

Both processes handle a wide range, but with caveats. CNC machines are incredibly versatile, working with metals (aluminum, steel, brass), plastics, and wood. Laser cutters are champions with metals, wood, acrylic, and fabric, but struggle with materials that melt or release toxic fumes, like PVC. Also, reflective materials like bare copper or aluminum can sometimes be tricky for standard CO2 lasers. The American Welding Society provides detailed guidelines on material interactions with thermal processes here.

Choosing the Right Process for Your Project

So, how do you decide? It often boils down to your part’s geometry, material, and required precision. Let’s walk through some common scenarios. I always tell my clients to sketch their part and ask: “Is this mostly a flat shape, or does it have depth and complex contours?

When to Choose CNC Machining

Opt for computer numerical control machining when your project needs:
– Complex 3D Geometry: Parts with curves, slopes, pockets, or undercuts (think a custom gear or a sculpted handle).
– Exceptional Strength & Precision: Parts requiring very tight tolerances (±0.001″ or better) and excellent structural integrity from a solid block.
– Threads and Detailed Features: Creating internal or external threads, precise holes for bearings, or intricate engravings on a curved surface.
In short, if you’re asking how to make a prototype for a mechanical part that needs to bear load or fit with other components, CNC is usually your best bet.

When to Choose Laser Cutting

A laser cutting service is likely your winner for projects that involve:
– Flat or 2D Parts: Signage, machine panels, brackets, intricate stencils, or architectural models.
– Speed for Thin Materials: Cutting through sheet metal or acrylic under 1/2″ thick is often significantly faster with a laser.
– Intricate, Clean Edges: Projects requiring very fine details and a smooth, sealed cut edge with minimal post-processing.
For example, if you need fifty identical flat brackets with complex cutouts by next week, laser cutting will get you there efficiently.

Practical Considerations and Common Questions

Beyond the technical specs, there are everyday factors to weigh. Let’s talk about setup, cost, and finish. A friend recently asked me about making custom aluminum nameplates. For a simple, flat plate with etched text, laser was cheaper and faster. But for a plate with a raised border and recessed text, CNC was the only way to go.

Setup and Cost: For one-off parts, laser cutting often has a simpler setup, making it more cost-effective for small batches. CNC machining might have a higher initial setup cost (programming, fixturing) but can become more economical for complex parts in larger quantities because the per-part time decreases.

Edge and Surface Finish: A laser-cut edge can have a characteristic slight taper and, on metals, a hardened layer. A machined edge is typically square and can have a variety of finishes (milled, turned, polished) directly from the machine. Sometimes, the best solution is a combination of both processes!

In the end, the “best” choice isn’t about which technology is superior, but which is superior *for your specific project*. By understanding the core strengths of CNC vs laser cutting, you can confidently choose the path that will bring your design to life most effectively. When in doubt, don’t hesitate to consult with a reputable machine shop—they can offer invaluable guidance based on your drawings and goals.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

CNC Machining vs Laser Cutting: Which Is Best for Your Project?

We'll Send You Back with Price Immediately!