Categories
Blog CNC Materials Guides Quality & Tolerances

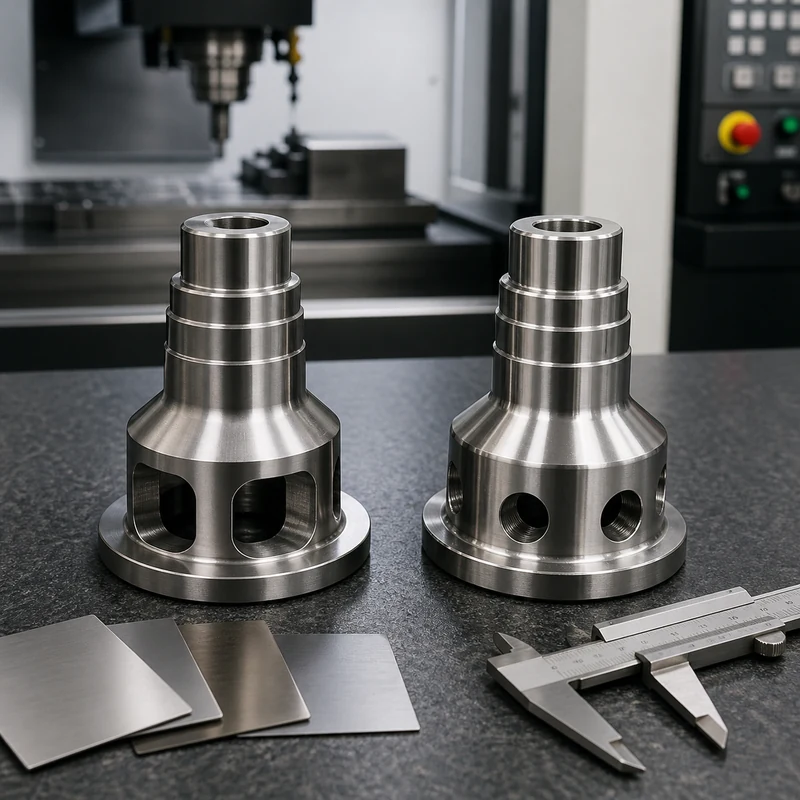
420 vs 316 Stainless Steel for CNC Machined Parts

420 and 316 stainless steel are both useful CNC materials, but they solve different engineering problems. One is normally chosen for hardness and wear resistance. The other is chosen when corrosion resistance, toughness, and long service life in wet or chemical environments matter more.

For a machined part, the right choice depends on load, exposure, surface finish, heat treatment, tolerance, and inspection requirements. MTSPi reviews these tradeoffs together with stainless steel CNC machining and the full part drawing before recommending a material route.

Quick Comparison

Requirement 420 stainless steel 316 stainless steel CNC buyer note
Stainless family Martensitic Austenitic Different structures create different machining and performance behavior.
Main advantage Hardness and wear resistance Corrosion resistance and toughness Start with the part’s failure risk, not just the alloy name.
Heat treatment Can be hardened Usually not hardened by heat treatment Specify target hardness if 420 is selected for wear.
Corrosion behavior Moderate Strong, especially around chlorides 316 is usually better for marine, medical, food, and chemical exposure.
Typical CNC use Shafts, tools, wear pads, molds, blades Housings, fittings, medical parts, marine parts Geometry and environment decide the final choice.

What 420 Stainless Steel Does Well

420 stainless steel contains enough carbon to be hardened by heat treatment. After hardening, it can provide higher surface hardness and better wear resistance than many common austenitic stainless grades. That makes it useful for parts that rub, slide, cut, or need to hold a working edge.

Common examples include shafts, valve parts, mold components, wear blocks, tooling features, and mechanical parts where corrosion exposure is limited. When the part includes milled pockets, turned diameters, slots, or threaded features, MTSPi may compare CNC milling service and CNC turning service routes to control distortion and finish.

Where 316 Stainless Steel Is Stronger

316 stainless steel is usually selected when the part must survive moisture, cleaning chemicals, salt exposure, or biological and food-contact environments. Its molybdenum content improves resistance to chloride attack, which is why buyers often consider it for marine, medical, chemical, and food-processing components.

316 is not the best choice when maximum hardness is the primary requirement, but it is often a better long-term material for parts exposed to corrosive service. It also pairs well with finishing and cleaning requirements planned through surface treatment.

Machinability and Production Planning

Manufacturing factor 420 stainless steel 316 stainless steel
Tool wear Depends heavily on hardness condition Can work harden if cutting is not controlled
Heat control Important after hardening or near tight features Important because heat and rubbing can worsen work hardening
Burr risk Varies with heat treatment and feature size Can be noticeable on small holes, slots, and thin edges
Inspection focus Hardness, wear surfaces, critical diameters Corrosion-critical surfaces, finish, dimensions, passivation notes

A material that looks cheaper on paper can become expensive if it needs extra passes, slower cutting, special inspection, or post-machining treatment. The RFQ should include material condition, quantity, finish, hardness if needed, and which dimensions are critical.

How to Choose Between 420 and 316

Choose this priority Better starting point Reason
High hardness after heat treatment 420 stainless steel It can be hardened for wear and edge retention.
Marine or chloride exposure 316 stainless steel It offers stronger corrosion resistance.
Medical or cleaning-heavy environment 316 stainless steel It is commonly used where corrosion resistance and cleanliness matter.
Wear part in a mostly dry environment 420 stainless steel Hardness may matter more than corrosion resistance.
General corrosion-resistant CNC component 316 stainless steel It is often the safer choice when exposure is uncertain.

Drawing and Quality Notes

If 420 is chosen for hardness, state the target hardness range and whether heat treatment occurs before or after machining. If 316 is chosen for corrosion resistance, state any passivation, polishing, cleaning, or surface roughness requirements. These details should appear in CNC machining drawings so quoting, machining, and inspection use the same assumptions.

For higher-risk parts, combine material certificates, dimensional reports, hardness checks, and surface finish checks through CNC machining quality inspection. This reduces the chance that a material choice looks correct but fails at receiving inspection or in service.

Conclusion

Choose 420 stainless steel when hardness, wear resistance, and heat-treatable strength are the main design goals. Choose 316 stainless steel when corrosion resistance, toughness, and long-term stability in wet or chemical environments are more important. For CNC machined parts, the best decision comes from matching material behavior to the real operating environment, not from treating all stainless steels as interchangeable.

Categories
Blog CNC Materials Quality & Tolerances

Is Nickel Magnetic? What CNC Buyers Should Know

Pure nickel is one of the common engineering metals that can respond to a magnet. That simple answer is useful, but it is not enough for machined-part purchasing because most real projects use nickel alloys, plated surfaces, or stainless and high-temperature alloys that contain nickel in different amounts.

For CNC buyers, magnetic behavior should be treated as a material requirement in the same way as hardness, corrosion resistance, surface finish, and tolerance. MTSPi reviews these details together with CNC material options and the intended application before selecting a practical machining route.

Short Answer: Pure Nickel Is Magnetic

Pure nickel is ferromagnetic at normal room temperature. It can be attracted by a magnet because its internal magnetic domains can align under a magnetic field. Its response is usually weaker than iron, and it changes when nickel is alloyed with other elements.

Material or alloy family Typical magnetic response CNC buyer note
Pure nickel Magnetic Confirm whether magnetic response is acceptable near sensors or electronic assemblies.
Nickel-copper alloys Usually low to moderate Composition and processing history matter.
Nickel-chromium alloys Often weak or nearly non-magnetic Useful where corrosion and heat resistance are more important than magnetism.
Austenitic stainless steel Usually non-magnetic or weakly magnetic Cold working or machining can increase local response.

Why Nickel Alloy Magnetism Varies

A material name alone rarely tells the whole story. Alloying additions, crystal structure, cold work, heat treatment, and service temperature all affect magnetic behavior. Two parts with similar nickel content can react differently if one has been heavily worked or heat treated.

This is why the drawing should state any magnetic requirement directly. If the part will sit near magnetic sensors, motors, instruments, or sensitive electronics, include that condition in the RFQ along with dimensions and finish. MTSPi can review it during drawing review before machining starts.

Temperature and the Curie Point

Nickel loses its ferromagnetic behavior when heated above its Curie temperature, about 358 C. Below that point, pure nickel can remain magnetic. Above it, the magnetic domains no longer align in the same way. For high-temperature equipment, this property should be checked against the real operating temperature rather than assumed from room-temperature behavior.

Machining Considerations for Nickel Materials

Nickel and many nickel alloys can be demanding to machine because they may work harden, retain heat, and wear tools quickly. Good process planning matters as much as material selection. Depending on the geometry, MTSPi may compare CNC milling service with CNC turning service or use a mixed process for features that need stable datums.

Practical controls include sharp tooling, correct cutting parameters, rigid workholding, suitable coolant, and inspection after critical operations. Surface damage, burrs, and residual stress can affect both function and cosmetic finish, so deburring and finishing should not be left until the last minute.

When Magnetic Behavior Should Be Specified

Application condition Why it matters What to tell the supplier
Sensor housings Magnetic response can affect readings State allowable magnetic behavior and test method.
Medical or laboratory tools Equipment may operate near magnets or instruments Confirm material grade and inspection expectations.
Aerospace or electronics fixtures Magnetic attraction may interfere with assembly or service Share operating environment and certification needs.
General mechanical parts Magnetism may not affect function Do not over-specify if it adds cost without benefit.

Inspection and Documentation

If magnetism is a functional requirement, define how it will be verified. A casual magnet check is not the same as a controlled inspection plan. Buyers can combine material certificates, dimensional reports, and special checks through CNC machining quality inspection when the application requires traceability.

The best specification is clear enough for quoting, machining, and receiving inspection. It should name the material grade, finish, tolerance, operating temperature, and any magnetic limits that affect the assembly.

Conclusion

Nickel is magnetic in pure form, but CNC projects usually require a more specific answer. Alloy composition, manufacturing route, temperature, and inspection requirements determine whether magnetic behavior matters. Treat it as an engineering requirement, not a trivia fact, and include it in the drawing package when it can affect performance.

Categories
Blog CNC Materials Quality & Tolerances

Does Stainless Steel Rust? Corrosion and CNC Machining Guide

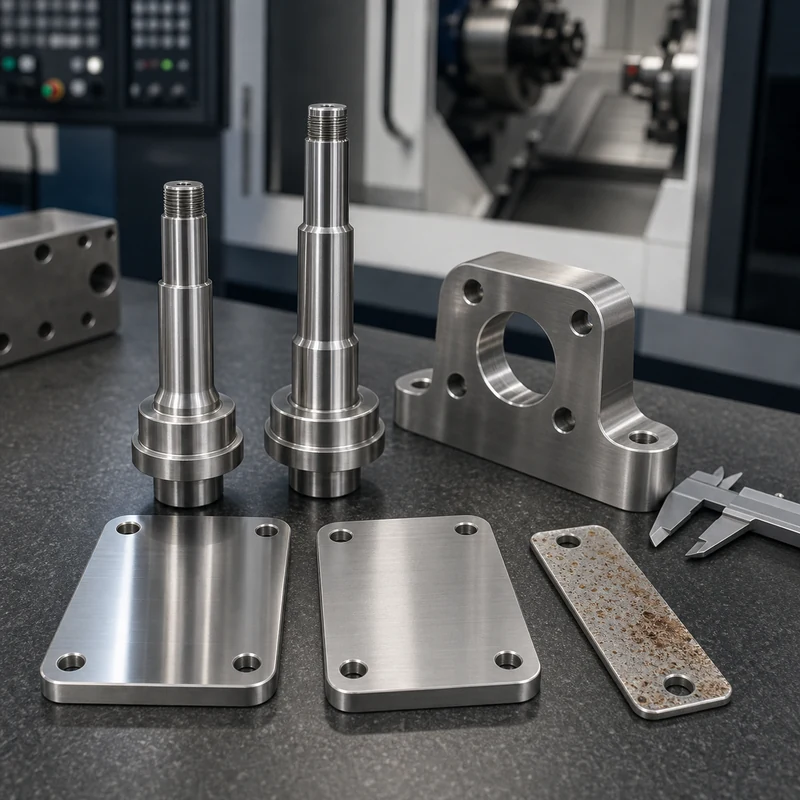
Stainless steel can rust, but it is far more corrosion resistant than ordinary carbon steel. The word stainless should be read as stain-resistant, not rust-proof. Its protection comes from chromium, which forms a thin passive chromium oxide layer on the surface. When the grade, finish, cleaning process, and service environment are chosen correctly, stainless steel is one of the most reliable materials for precision CNC parts. MTSPi supports stainless steel CNC machining for components that need strength, durability, corrosion resistance, and controlled inspection.

Does Stainless Steel Rust?

Yes, stainless steel can rust under the wrong conditions. It contains iron, so corrosion is possible. The reason it resists rust better than plain steel is its chromium content. Most stainless steels contain at least about 10.5 percent chromium. In the presence of oxygen, chromium forms a stable surface film that slows the reaction between the metal below and the surrounding environment.

That passive layer is extremely thin, but it is also self-renewing in many normal environments. If a light scratch exposes fresh stainless steel, chromium can react with oxygen again and rebuild protection. Problems begin when the passive layer is contaminated, mechanically damaged, starved of oxygen, or attacked by chlorides, strong chemicals, or heat.

Stainless Steel vs Carbon Steel Rust

Question Stainless Steel Carbon Steel
Base protection Chromium oxide passive film No comparable passive chromium layer
Rust tendency Low in suitable environments, but not zero High when moisture and oxygen are present
Common corrosion mode Pitting, crevice corrosion, tea staining, surface contamination Red-brown rust, scaling, section loss
Maintenance need Cleaning and grade/finish selection matter Coating, oiling, plating, or paint often required
Typical use Medical, food, marine, industrial, aerospace, precision hardware Structural, general fabrication, tooling, machinery

Why Stainless Steel Rusts

Most stainless rust problems come from a mismatch between environment and material preparation. A part that works perfectly indoors may show staining near salt spray. A polished stainless part can rust if carbon steel particles are embedded during grinding. A tightly assembled joint can corrode in a crevice where oxygen cannot reach the surface easily.

  • Chlorides from seawater, road salt, cleaning chemicals, or coastal air can attack the passive layer.
  • Carbon steel contamination from tools, fixtures, abrasive media, or handling can create rust spots.
  • Deep scratches, rough surfaces, and embedded debris can make local corrosion easier.
  • Crevices, blind holes, and trapped moisture reduce oxygen access and encourage localized attack.
  • The wrong grade can fail even if the part was machined and cleaned correctly.

304 vs 316 Stainless Steel

304 stainless steel is widely used for general corrosion resistance, food equipment, housings, brackets, and industrial components. 316 stainless steel includes molybdenum, which improves resistance to chloride attack. That is why 316 is often preferred for marine, coastal, chemical, and medical-adjacent applications where corrosion risk is higher.

Grade Best Fit Corrosion Note CNC Machining Note
304 stainless steel General industrial, indoor, food equipment, covers, brackets Good all-purpose corrosion resistance Tougher to machine than aluminum or brass; stable process planning matters
316 stainless steel Marine, coastal, chemical, medical, wet-service components Better chloride and pitting resistance than 304 Often selected when corrosion risk outweighs extra cost
316L stainless steel Welded parts and corrosion-sensitive assemblies Lower carbon helps after welding Useful when machining is followed by welding or passivation
17-4 PH stainless Higher-strength precision parts Good corrosion resistance with heat-treatable strength Requires planning around heat treatment and final dimensions

Does Stainless Steel Corrode in Salt Water?

It can. Salt water is one of the most important corrosion risks for stainless steel because chloride ions can break down the passive film and create pitting. A small pit can become a stress riser or a cleaning problem even when the rest of the surface looks acceptable. For continuous seawater exposure, grade selection, surface finish, crevice control, and maintenance requirements should be reviewed carefully.

Environment Typical Recommendation Reason
Dry indoor use 304 often works well Low chloride exposure and easier cleaning
Outdoor general use 304 or 316 depending on pollution and cleaning Rain, dirt, and contaminants vary by location
Coastal air 316 is often preferred Chloride exposure raises pitting and tea-staining risk
Marine contact 316, 316L, duplex, or specialized stainless may be needed Continuous salt exposure is aggressive
Chemical service Confirm compatibility by chemical and temperature Stainless grades respond differently to acids, alkalis, and chlorides

Manufacturing Contamination: A Common Hidden Cause

A stainless part can appear to rust because iron contamination on its surface is rusting. This may come from shared grinding media, carbon steel wire brushes, clamps, tables, cutting tools, or airborne particles. For precision CNC components, clean process separation and post-machining cleaning are not cosmetic details; they directly affect corrosion performance.

For critical parts, MTSPi can align machining, deburring, cleaning, and quality assurance expectations before production. If the drawing requires passivation, electropolishing, special packaging, or post-finish inspection, those requirements should be included in the RFQ stage.

How to Improve Stainless Steel Corrosion Resistance

  • Choose the grade around the real environment, especially chloride exposure.
  • Use dedicated or properly cleaned tools and abrasives for stainless steel work.
  • Specify passivation when free iron removal and passive-layer restoration are important.
  • Use smoother finishes where cleanliness and corrosion resistance matter.
  • Avoid crevices, liquid traps, sharp untreated edges, and rough pockets when possible.
  • Clean parts before packaging and avoid storage materials that leave reactive residue.

Surface Finish and Passivation

Surface finish affects how stainless steel behaves over time. A smoother surface leaves fewer places for moisture, salt, and debris to sit. Brushing, polishing, bead blasting, passivation, electropolishing, and coating each solve different problems. Review surface treatment options early because finishing can affect appearance, final dimensions, inspection method, and cost.

Finish or Treatment What It Does When to Consider It
Mechanical polishing Smooths and brightens the surface Visible parts and easier cleaning
Brushing Creates a consistent directional texture Decorative panels, covers, and handled parts
Passivation Removes free iron and supports the passive layer Medical, food, aerospace, and corrosion-sensitive components
Electropolishing Smooths micro-peaks and improves cleanability Sanitary, medical, and high-cleanliness parts
Coating Adds a barrier or color layer Special environments, appearance, or isolation needs

Is Stainless Steel Good for CNC Machining?

Yes. Stainless steel is a strong choice for CNC machined parts that need durability, heat resistance, cleanability, and corrosion resistance. It is more difficult to machine than aluminum or brass, so tool selection, coolant, workholding, speeds, feeds, and inspection planning matter. The tradeoff is worthwhile when the part must survive demanding environments or repeated cleaning.

Common CNC machined stainless parts include shafts, fittings, manifolds, housings, brackets, instrument components, medical hardware, food processing parts, robotic end-effectors, and aerospace hardware. Compare stainless with other CNC machining materials when strength, corrosion, magnetic behavior, and cost are being balanced.

FAQ

Can 304 stainless steel rust?

Yes. 304 stainless steel can rust or stain in harsh chloride exposure, poor cleaning conditions, or contaminated manufacturing environments, although it performs well in many general applications.

Can 316 stainless steel rust?

Yes. 316 stainless steel can still corrode, but it usually resists chlorides better than 304 because it contains molybdenum.

Does stainless steel rust after machining?

It can if the surface is contaminated, roughly finished, exposed to harsh conditions, or not cleaned properly. Passivation and suitable finishing can reduce this risk.

Related MTSPi Resources

Categories
Blog CNC Materials Quality & Tolerances

Does Aluminum Rust? Corrosion, Oxidation, Anodizing, and CNC Part Protection

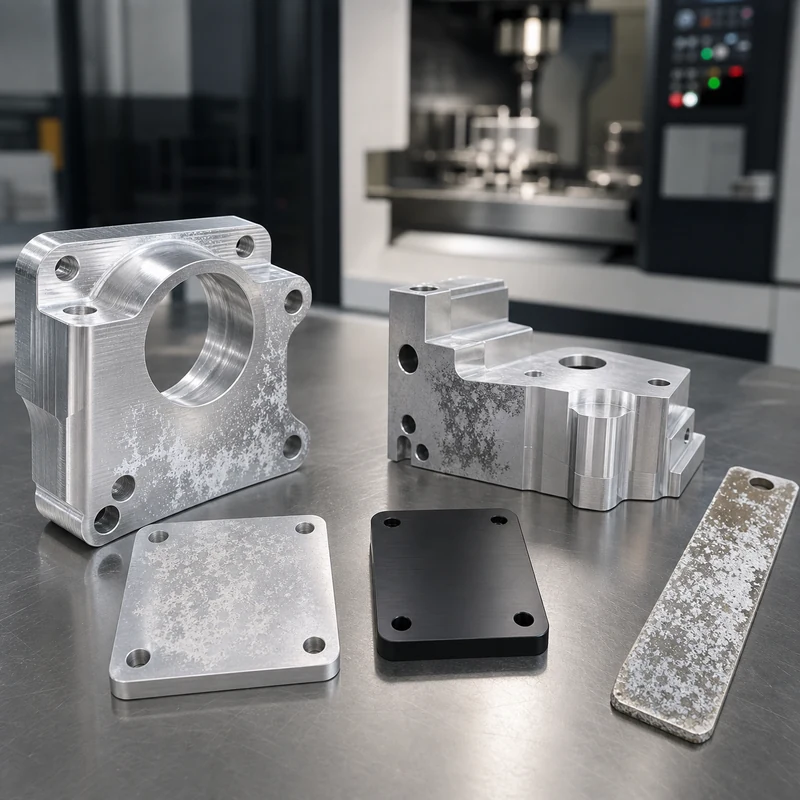
Quick answer: Aluminum does not rust because rust is iron oxide and aluminum contains no iron in normal use. However, aluminum can oxidize and corrode. Its natural oxide layer often protects the surface, but salt, chemicals, galvanic contact, and poor finishing can still damage aluminum parts.

Does Aluminum Rust?

Many buyers use the word rust to describe any metal surface damage. For aluminum, the more accurate terms are oxidation, corrosion, pitting, and galvanic corrosion. Understanding the difference helps choose the right alloy and finish.

Key Points for Buyers and Engineers

Topic What to know Practical impact
Rust Iron oxide on steel or iron Not the normal aluminum corrosion mode.
Oxidation Thin aluminum oxide layer Often protective in normal environments.
Pitting corrosion Localized attack Can occur with salts or harsh chemicals.
Galvanic corrosion Reaction between dissimilar metals Needs material pairing and isolation planning.

How This Affects CNC Machined Parts

Aluminum is widely used for CNC milled and turned parts. If corrosion or appearance matters, consider anodizing, chromate conversion, powder coating, painting, or plating from the surface treatment options.

Design and Purchasing Checklist

  • Choose the aluminum alloy by strength and environment.
  • Avoid direct contact with incompatible metals when corrosion matters.
  • Specify anodizing color, thickness, and masking needs.
  • Protect cosmetic parts during shipping.
  • Clean machined surfaces before finishing.

Related MTSPi Resources

FAQ

Does anodized aluminum rust?

No. Anodized aluminum does not rust like steel, but the anodized layer can be damaged or attacked in harsh conditions.

Why does aluminum turn white?

White powdery residue can be aluminum corrosion product from oxidation or environmental exposure.

Is aluminum good for outdoor parts?

Often yes, but alloy choice, anodizing, coating, drainage, and contact metals should be reviewed.

Need help with aluminum CNC part protection?

Send drawings, material, quantity, finish, tolerance notes, and application requirements. MTSPi can review manufacturability before quoting.

Contact MTSPi for engineering and quote support

Practical Buyer Notes

Aluminum corrosion pages should answer the simple rust question first, then explain oxidation, pitting, galvanic corrosion, anodizing, alloy choice, and surface protection.

This topic is valuable because many buyers use aluminum for CNC parts but do not understand when bare aluminum is enough and when anodizing, coating, or isolation from other metals is needed.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Indoor prototype Bare or as-machined aluminum may be enough Lowest cost and fastest lead time
Outdoor use Consider anodizing or coating Improves corrosion and appearance control
Salt exposure Review alloy and protective finish carefully Pitting risk increases
Dissimilar metals Use isolation or compatible design Reduces galvanic corrosion risk

Common Mistakes to Avoid

  • Saying aluminum cannot corrode because it does not rust.
  • Ignoring galvanic corrosion when aluminum touches stainless steel or other metals.
  • Choosing anodizing color without discussing thickness or masking.
  • Using the wrong alloy for outdoor or marine-like exposure.

Recommended MTSPi Review Workflow

MTSPi should review aluminum parts by alloy, environment, appearance, tolerance, and finishing. Corrosion protection should be planned before machining if masking or dimensional control is needed.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send alloy preference, operating environment, cosmetic expectation, anodizing or coating requirement, critical dimensions, and mating material information.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Deeper Engineering Notes

For aluminum corrosion and oxidation, the strongest page is not just a definition. It should help a buyer decide what information belongs on the drawing, what questions to ask a supplier, and which details affect cost, quality, and delivery. In real RFQ work, the important details are usually alloy choice, anodizing, galvanic contact, drainage, salt exposure, and cosmetic expectations. These details decide whether the supplier can quote confidently or has to return with repeated questions.

The common risk is assuming aluminum cannot fail outdoors because it does not form red rust. That risk can make the content look complete on the surface but weak in a real manufacturing situation. A stronger specification connects the topic to material behavior, machine access, tolerance control, finishing, and inspection before the order is released.

Example Specification Review

Review area Question to answer Good specification practice
Function What does this feature or part need to do? Describe the load, fit, motion, appearance, sealing, or assembly requirement.
Material Is the selected material suitable for the environment? Confirm strength, heat, corrosion, wear, chemical exposure, and cosmetic needs.
Geometry Can the feature be reached by standard tools? Review depth, corner radius, wall thickness, tool clearance, and setup direction.
Tolerance Which dimensions are truly critical? Use tight tolerances only where function requires them and keep general dimensions practical.
Verification How will acceptance be checked? Define gauges, CMM checks, roughness measurement, thread inspection, or visual standards when needed.

How This Page Should Support Ranking

This topic can attract both beginner searches and buyer searches. The beginner wants a clear answer; the buyer wants enough detail to make a manufacturing decision. A page has a better chance to rank when it answers the simple question first, then adds examples, process limits, design notes, comparison tables, and practical next steps.

That is also why internal links should be helpful rather than forced. A reader should naturally move from this page to a process page, material page, surface finish page, inspection page, or quote page only when that next step solves a real question.

Conclusion

Aluminum does not rust like steel, but corrosion planning still matters. The right alloy, finish, and assembly design can greatly improve aluminum CNC part durability.

Categories
Blog CNC Materials Quality & Tolerances

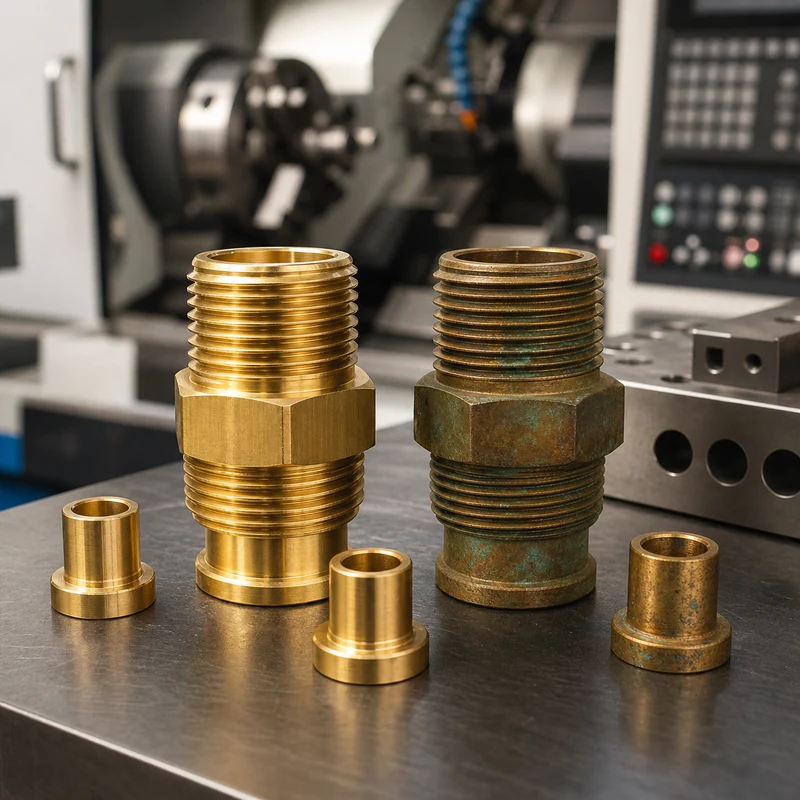
Does Brass Rust or Tarnish? Complete Guide to Brass Corrosion and CNC Brass Parts

Quick answer: Brass does not rust like steel because rust is iron oxide and brass is mainly copper and zinc. However, brass can tarnish, darken, form a green patina, corrode, or suffer dezincification in harsh environments. For CNC machined brass parts, alloy choice, surface finish, storage, cleaning, and operating conditions decide how the part ages.

Does Brass Rust?

Strictly speaking, brass does not rust. Rust is the red or orange iron oxide corrosion product that forms on iron and steel. Standard brass is a copper-zinc alloy, so it does not produce the same flaky red rust seen on carbon steel. This is one reason brass is widely used for fittings, electrical contacts, decorative hardware, bushings, valve parts, and turned components.

That does not mean brass is immune to surface change. Brass can tarnish in air, discolor from handling, develop patina outdoors, and corrode in aggressive water, salt, ammonia, acidic environments, or certain industrial chemicals. So the better question is not only “does brass rust?” but also “what type of corrosion or appearance change can happen to brass?”

Brass Rust vs Tarnish vs Corrosion vs Dezincification

Surface condition Typical appearance Cause Risk level
Rust Red or orange flaky oxide Iron oxidation Not typical for normal brass unless iron contamination is present
Tarnish Dull brown, yellow-brown, or darker surface Reaction with oxygen, sulfur compounds, oils, or handling Usually cosmetic
Patina Green or blue-green film Long-term copper reaction with moisture, salts, pollutants, or carbonates Often surface-level but may be undesirable
General corrosion Dull, stained, etched, or roughened surface Chemicals, water quality, salt, acids, or pollutants Can become functional if severe
Dezincification Pink or copper-rich surface, weakened structure Zinc is selectively removed from brass Potentially serious for pressure, water, and load-bearing parts

Why Brass Tarnishes

Brass tarnish is usually an oxidation or surface reaction. Air, moisture, skin oils, sulfur compounds, fingerprints, cleaners, and packaging materials can change the surface color. For decorative parts, tarnish may be unacceptable even if the part still works. For hidden mechanical parts, light tarnish is often harmless.

Freshly machined brass may look bright because the cutting tool exposes clean metal. Over time, that surface reacts with the environment. Polishing can restore brightness, but polished brass will still change again unless it is protected by clear coating, plating, controlled packaging, or regular maintenance.

What Is Dezincification?

Dezincification is a form of brass corrosion where zinc is removed from the alloy and a copper-rich structure remains. The surface may look pinkish or reddish. Mild cases can appear cosmetic, but severe dezincification can weaken the part and create leakage or failure in fluid-handling components.

This matters for valves, fittings, threaded brass parts, plumbing-related components, marine hardware, and parts exposed to aggressive water chemistry. If the application involves water, pressure, salt, heat, or chemicals, buyers should confirm the brass grade instead of simply requesting “brass.”

Where Brass Performs Well

  • Electrical contacts and conductive components
  • Precision turned fittings and threaded inserts
  • Bushings, sleeves, spacers, and small mechanical hardware
  • Decorative machined parts and visible metal trim
  • Valve components and fluid fittings when the correct grade is selected
  • Low-friction or wear-related applications with moderate loads

Brass Grades and CNC Machining Considerations

Brass is generally one of the easiest metals to machine. It cuts cleanly, forms chips well, and can achieve good surface finish. Free-cutting brass is especially efficient for high-volume turned parts, but some applications require lead-free or dezincification-resistant brass. A purchasing specification should identify the exact alloy when compliance, water exposure, or mechanical properties matter.

For machined brass parts, MTSPi can support CNC turning, milling, drilling, tapping, and finishing. Brass parts often include threads, bores, flats, grooves, knurls, slots, and sealing surfaces. Each feature should be reviewed for tool access and inspection method.

How to Protect CNC Machined Brass Parts

Protection method Best use Important note
Polishing Bright cosmetic appearance May need maintenance or additional coating
Clear coating Decorative brass surfaces Can reduce tarnish from handling and air exposure
Nickel plating Appearance, wear, and corrosion resistance Thread fit and thickness should be considered
Chrome plating Harder decorative surface Usually more process planning and cost
Controlled packaging Shipping and storage protection Useful for polished or cosmetic parts

Cleaning Brass: What to Avoid

Avoid aggressive ammonia-based cleaners on stressed brass parts because ammonia exposure can contribute to cracking risk in some brass conditions. Acidic cleaners can brighten brass but may also attack the surface if used incorrectly. For precision machined parts, cleaning should preserve dimensions, threads, sealing faces, and cosmetic requirements.

FAQ

Does brass rust in water?

No, brass does not form red iron rust in water. But water chemistry can cause tarnish, general corrosion, or dezincification depending on the alloy and exposure.

Why does brass turn green?

Green patina forms when copper in brass reacts with moisture, salts, carbon dioxide, or pollutants. It is common on copper-rich alloys exposed outdoors.

Is tarnished brass ruined?

Usually no. Light tarnish is often cosmetic and can be cleaned or polished. Severe dezincification or deep corrosion is more serious.

Is brass better than stainless steel?

It depends on the application. Brass machines easily and conducts electricity well. Stainless steel usually performs better in many corrosion and strength-critical environments.

Can brass CNC parts be plated?

Yes. Brass can be polished, nickel plated, chrome plated, brushed, or coated. Finishing should be planned before machining if dimensions or appearance are critical.

Need brass CNC machined parts?

Send your drawing, alloy requirement, quantity, finish, and working environment. MTSPi can review the right brass grade and surface treatment.

Request a brass machining quote

Conclusion

Brass does not rust like steel, but it can tarnish, patinate, corrode, or dezincify. For CNC machined brass parts, the safest approach is to match alloy, machining method, finish, and packaging to the actual working environment.

Categories
Blog CNC Materials

Is Aluminum a Metal? Properties, Alloy Types, and CNC Machining Uses

Yes, aluminum is a metal. More specifically, it is a lightweight, silvery, non-ferrous metal known for its low density, corrosion resistance, electrical conductivity, thermal conductivity, and strong usefulness in manufacturing. If you see the spelling aluminium, it refers to the same element. Aluminum is the common American spelling, while aluminium is common in British English and many international markets.

That quick answer is useful, but buyers and engineers usually need more than a dictionary definition. The practical question is not only whether aluminum is a metal, but why it behaves differently from steel, copper, titanium, or plastic, and why it is so widely used in CNC machined parts. This guide explains aluminum as a metal from a material selection and manufacturing perspective, with clear comparisons, alloy examples, CNC machining notes, finishing options, and design guidance.

For custom aluminum components, MTSPi supports aluminum CNC machining, CNC milling, finishing, and inspection for prototypes and production parts.

Is Aluminum a Metal?

Aluminum is a metal because it has the core characteristics associated with metallic elements: metallic bonding, good electrical and thermal conductivity, ductility, malleability, a metallic luster, and the ability to form useful alloys. On the periodic table, aluminum has the symbol Al and atomic number 13. It belongs to the boron group, but in practical engineering it is treated as one of the most important commercial metals.

Unlike iron and steel, aluminum is a non-ferrous metal. That means it does not use iron as its main base element. This distinction matters because non-ferrous metals generally behave differently in weight, corrosion resistance, magnetism, conductivity, and machining. Aluminum is also not magnetic under normal conditions, which makes it useful in electronic housings, instrument components, aircraft parts, and fixtures where magnetic interference must be avoided.

Aluminum vs Aluminium: Are They the Same?

Yes. Aluminum and aluminium mean the same material. The spelling difference is regional, not technical. In the United States and Canada, aluminum is the dominant spelling. In the United Kingdom, Europe, and many other markets, aluminium is more common. A drawing, RFQ, or datasheet using either spelling can refer to the same metal.

For international sourcing, the alloy designation matters more than the spelling. A request for aluminum 6061-T6 or aluminium 6061-T6 is much clearer than simply asking for aluminum. The grade, temper, surface finish, tolerance, and inspection requirements define the real manufacturing result.

Key Properties of Aluminum

Property Why It Matters in Real Parts Manufacturing Note
Low density Aluminum is much lighter than steel, which helps reduce part weight. Useful for aerospace, robotics, fixtures, handheld products, and moving assemblies.
Corrosion resistance A natural oxide layer helps protect the surface from many environments. Anodizing or coating can improve protection and appearance.
Good machinability Many aluminum alloys cut efficiently and hold fine details. Sharp tools, chip evacuation, and proper feeds help maintain finish and accuracy.
Thermal conductivity Aluminum transfers heat well. Useful for heat sinks, housings, brackets, and thermal management parts.
Electrical conductivity Aluminum conducts electricity, though not as well as copper. Useful in electrical housings, bus bars, connectors, and lightweight conductive components.
Ductility Aluminum can deform before fracture and can be extruded, rolled, bent, or machined. Formability depends heavily on alloy and temper.
Surface finish compatibility Aluminum accepts anodizing, bead blasting, polishing, plating, and coating. Finish requirements should be specified before quoting.

Is Aluminum a Pure Metal or an Alloy?

Pure aluminum exists as an element, but most industrial aluminum parts are not made from commercially pure aluminum. They are usually made from aluminum alloys. An alloy is a metal mixture designed to improve strength, hardness, machinability, heat treatment response, corrosion behavior, or formability.

Common alloying elements include magnesium, silicon, copper, zinc, manganese, and chromium. These small additions can change performance dramatically. For example, 6061 aluminum is valued for balanced machinability, corrosion resistance, and weldability, while 7075 aluminum is selected when higher strength is needed.

Common Aluminum Alloy Families

Series Main Alloying Element Typical Strengths Common Uses
1000 series Mostly pure aluminum Excellent conductivity and corrosion resistance, low strength Electrical, chemical, reflective, and formed parts
2000 series Copper High strength and good fatigue performance Aerospace and structural parts where corrosion protection is managed
3000 series Manganese Good formability and corrosion resistance Sheet metal, housings, tanks, and general formed products
5000 series Magnesium Good corrosion resistance, especially marine environments Marine, automotive, welded structures, and sheet applications
6000 series Magnesium and silicon Balanced strength, machinability, corrosion resistance, and anodizing response CNC machined parts, frames, brackets, fixtures, housings
7000 series Zinc Very high strength potential Aerospace, high-load parts, tooling, and performance components

6061 Aluminum: The Common CNC Machining Choice

6061 aluminum is one of the most common materials for CNC machined aluminum parts. It offers a practical balance of strength, corrosion resistance, cost, availability, and machinability. It is often used for brackets, plates, housings, fixtures, covers, adapters, frames, and prototype components.

For buyers who are unsure which aluminum grade to start with, 6061-T6 is often a sensible baseline. It is not the strongest aluminum alloy, but it is versatile and widely available. It also responds well to anodizing, which helps when both appearance and corrosion resistance matter.

7075 Aluminum: Higher Strength for Demanding Parts

7075 aluminum is often selected when higher strength is required. It is common in aerospace, robotics, tooling, cycling components, and performance parts where weight reduction matters but the part still needs strong mechanical properties. The tradeoff is that 7075 is generally more expensive than 6061 and can be less corrosion resistant unless properly protected.

For CNC machining, 7075 can produce excellent parts, but material sourcing, tool selection, and finishing expectations should be reviewed carefully. If anodizing, appearance, or corrosion exposure is important, the alloy and temper should be confirmed before production.

Aluminum vs Steel

Aluminum and steel are both metals, but they are not interchangeable. Steel is much denser and usually stronger and stiffer by volume. Aluminum is much lighter and often easier to machine quickly. The right choice depends on strength, weight, stiffness, corrosion, magnetic behavior, cost, surface finish, and operating environment.

Comparison Point Aluminum Steel
Weight Low density, excellent for lightweight parts Much heavier
Strength Good strength-to-weight ratio, alloy dependent Usually higher absolute strength and stiffness
Corrosion Naturally corrosion resistant; anodizing improves protection Can rust unless stainless, coated, plated, or treated
Machining Often faster cutting and good surface finish Can be slower, harder, and more tool-wearing depending on grade
Magnetism Non-magnetic in normal use Many steels are magnetic
Cost behavior Material may cost more per kg, but machining can be efficient Material can be cheaper, but machining and finishing vary

Why Aluminum Is Popular for CNC Machining

Aluminum is popular for CNC machining because it combines useful mechanical performance with efficient manufacturing. Many aluminum alloys cut cleanly, allow high spindle speeds, and produce accurate features with good surface finish. This can reduce machining time compared with harder metals.

  • It is light enough for moving assemblies, robotic systems, drones, aerospace brackets, and portable devices.
  • It can be machined into plates, housings, heat sinks, manifolds, brackets, covers, adapters, and fixtures.
  • It supports many surface finishes, including clear anodizing, color anodizing, hard anodizing, bead blasting, polishing, and plating.
  • It is widely stocked in plate, bar, extrusion, and billet forms, which helps control lead time.
  • It offers a strong balance between prototype speed and production reliability.

CNC Design Notes for Aluminum Parts

Aluminum is forgiving compared with many engineering metals, but design choices still affect cost, accuracy, and quality. Deep pockets, thin walls, tight internal radii, very small tapped holes, cosmetic surfaces, and tight flatness requirements should be reviewed before manufacturing.

Design Area Recommendation Why It Helps
Internal corners Use the largest practical corner radius. Larger tools cut faster and reduce tool chatter.
Thin walls Avoid overly thin unsupported walls when possible. Thin aluminum walls can vibrate or deform during machining.
Deep pockets Reduce depth or increase tool access where possible. Deep features increase cycle time and tool deflection risk.
Tapped holes Specify thread size, depth, and required engagement clearly. This avoids confusion during drilling and tapping.
Tolerances Apply tight tolerances only to functional features. Unnecessary tight tolerances increase cost and inspection time.
Cosmetic areas Mark visible surfaces on the drawing. The shop can protect or finish the correct faces.

Surface Finishes for Aluminum

One reason aluminum is so widely used is its compatibility with many finishing methods. Clear anodizing can protect the surface while keeping a natural metallic look. Color anodizing adds appearance and identification value. Hard anodizing improves wear and corrosion resistance for demanding parts. Polishing and bead blasting can change the texture and reflectivity.

Finish choice should be discussed early because it can affect dimensions, color consistency, masking, electrical conductivity, and final inspection. For more options, see MTSPi’s surface treatment resources.

Common Applications of Aluminum

Aluminum appears across many industries because it is light, machinable, corrosion resistant, and visually clean after finishing. It is common in aerospace parts, automotive components, automation fixtures, robotics frames, electronic housings, heat sinks, medical device prototypes, optical mounts, consumer hardware, and custom industrial components.

  • Aerospace: brackets, plates, housings, lightweight structural components, and test fixtures.
  • Automation and robotics: arms, mounts, grippers, frames, sensor brackets, and end-effectors.
  • Electronics: heat sinks, enclosures, covers, EMI-related housings, and connector parts.
  • Automotive: prototype brackets, battery-related housings, adapters, and performance components.
  • Medical and instruments: lightweight fixtures, housings, trays, and development prototypes.

How to Choose the Right Aluminum Grade

When reading a material callout, distinguish the Al element symbol from alloy and temper codes: the symbol alone does not specify the grade or its condition.

Do not choose aluminum only because it is light. Choose the grade based on the actual function of the part. If the part is a general machined bracket, 6061 may be enough. If the part is high-load and weight-sensitive, 7075 may be worth considering. If corrosion, welding, forming, conductivity, or cosmetic anodizing matters, the alloy choice may change.

Need Likely Starting Point Important Check
General CNC machined parts 6061-T6 Tolerance, finish, and cost target
Higher strength lightweight parts 7075-T6 Corrosion protection and material cost
Good forming or sheet applications 3000 or 5000 series Bend radius, temper, and surface finish
Marine or corrosion exposure 5000 series or protected 6000 series Environment and coating requirements
Electrical or thermal conductivity 1000 series or suitable conductive alloy Strength and conductivity balance

Is Aluminum Better Than Plastic for CNC Parts?

Aluminum is not always better than plastic. It is better when the part needs metallic strength, heat transfer, threaded features, stiffness, surface finish options, or electrical conductivity. Engineering plastics may be better when the part needs chemical resistance, electrical insulation, low friction, transparency, or lower weight without conductive behavior.

If you are comparing aluminum with plastic for CNC machining, review CNC plastic machining and CNC machining materials before locking the drawing. Material selection is one of the easiest ways to control part cost and performance before production begins.

Conclusion

Aluminum is definitely a metal, but its real value comes from the way it balances low weight, machinability, corrosion resistance, conductivity, surface finish options, and alloy flexibility. For many CNC machined parts, aluminum provides a practical middle ground between heavy structural metals and lower-strength plastics.

For a custom aluminum part, send MTSPi your 3D model, drawing, quantity, finish requirement, tolerance notes, and target application. Our team can help review material choice, manufacturability, surface treatment, and inspection through our quote and engineering support process.

Related MTSPi Resources

FAQ

Is aluminum a metal or nonmetal?

Aluminum is a metal. It has metallic luster, conductivity, ductility, and the ability to form useful engineering alloys.

Is aluminum a ferrous metal?

No. Aluminum is a non-ferrous metal because it is not based on iron. This is why it does not rust like ordinary carbon steel and is not magnetic in normal use.

Is aluminum naturally corrosion resistant?

Yes. Aluminum forms a thin oxide layer that helps protect the surface. In tougher environments, anodizing, coating, or plating can improve protection.

What aluminum grade is best for CNC machining?

6061-T6 is one of the most common starting choices because it is available, machinable, reasonably strong, and suitable for many finishes. 7075 is used when higher strength is needed.

Can aluminum be anodized after CNC machining?

Yes. Many CNC machined aluminum parts are anodized after machining. Clear, color, and hard anodizing are common options depending on appearance, corrosion resistance, and wear requirements.

Is aluminum lighter than steel?

Yes. Aluminum is much lighter than steel. This makes it valuable for aerospace, robotics, vehicles, fixtures, and any assembly where reduced moving mass matters.

Does aluminum rust?

Aluminum does not rust like iron or carbon steel because rust is iron oxide. Aluminum can corrode, but its oxide layer usually provides useful protection.


Categories
Blog CNC Materials Industries & Applications Quality & Tolerances

CNC Machining for Medical Devices: Materials, Applications, and Quality Checks

Quick answer: CNC machining is used for medical device prototypes, surgical tools, instrument parts, housings, fixtures, test components, and precision hardware. Medical parts often require careful material selection, clean machining, dimensional inspection, traceability, and clear documentation.

CNC Machining for Medical Devices

Medical machining is not only about tight tolerances. Buyers must consider biocompatible or application-appropriate materials, clean edges, surface finish, inspection records, and consistent communication about critical features.

Key Points for Buyers and Engineers

Topic What to know Practical impact
Materials Stainless steel, titanium, aluminum, PEEK, PC, PPSU Material must match use and regulatory expectations.
Features Small holes, slots, threads, mating surfaces Tool access and burr control are important.
Inspection CMM, gauges, visual checks, reports Confirms critical dimensions and drawing requirements.
Finish Polishing, passivation-like cleaning, anodizing, marking Affects appearance, corrosion behavior, and cleanliness.

How This Affects CNC Machined Parts

Medical prototypes may use both milling and turning. The process should be selected by geometry, material, tolerance, surface finish, and inspection requirements rather than by price alone.

Design and Purchasing Checklist

  • Mark critical dimensions and datums clearly.
  • Confirm material grade and certificate needs.
  • Define burr, edge break, and cleanliness expectations.
  • Request inspection reports when fit is critical.
  • Review finish compatibility before production.

Related MTSPi Resources

FAQ

What medical parts can be CNC machined?

Instrument components, housings, fixtures, prototype parts, surgical tool components, and precision hardware can be machined.

Is titanium used for medical CNC parts?

Yes, titanium is used in certain medical applications because of strength, corrosion resistance, and biocompatibility considerations.

Do medical CNC parts need CMM inspection?

Many precision medical parts benefit from CMM inspection, especially when GD&T or assembly-critical features are present.

Need help with medical CNC machining?

Send drawings, material, quantity, finish, tolerance notes, and application requirements. MTSPi can review manufacturability before quoting.

Contact MTSPi for engineering and quote support

Practical Buyer Notes

Medical machining pages need depth because the topic involves more than precision. Cleanliness, burr control, traceability, material documentation, surface finish, and inspection expectations can all be important.

The page should avoid making regulatory claims that are too broad. Instead, it should explain practical manufacturing controls for prototypes, test fixtures, instruments, housings, and precision medical hardware.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Material Confirm stainless steel, titanium, PEEK, PC, or other grade Material must match function and documentation needs
Burr control Define edge breaks and clean transitions Sharp edges can create safety and assembly issues
Inspection Use CMM, gauges, and reports for critical features Supports part verification
Cleanliness Plan cleaning and packaging expectations Protects parts during handling and shipment

Common Mistakes to Avoid

  • Using vague material names instead of exact grades.
  • Ignoring burrs on small holes, slots, and edges.
  • Treating surface finish as cosmetic only.
  • Failing to define inspection records before production.

Recommended MTSPi Review Workflow

MTSPi should review medical-related CNC parts with extra attention to material, edge condition, finish, and critical dimensions. The page should explain this clearly without overstating certification scope.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send CAD, drawing, material grade, finish, required reports, cleaning expectations, critical dimensions, and whether the part is for prototype, fixture, or production use.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Deeper Engineering Notes

For medical CNC machining, the strongest page is not just a definition. It should help a buyer decide what information belongs on the drawing, what questions to ask a supplier, and which details affect cost, quality, and delivery. In real RFQ work, the important details are usually material traceability, burr control, clean handling, inspection reports, and revision discipline. These details decide whether the supplier can quote confidently or has to return with repeated questions.

The common risk is making broad claims without defining the exact medical application and documentation needs. That risk can make the content look complete on the surface but weak in a real manufacturing situation. A stronger specification connects the topic to material behavior, machine access, tolerance control, finishing, and inspection before the order is released.

Example Specification Review

Review area Question to answer Good specification practice
Function What does this feature or part need to do? Describe the load, fit, motion, appearance, sealing, or assembly requirement.
Material Is the selected material suitable for the environment? Confirm strength, heat, corrosion, wear, chemical exposure, and cosmetic needs.
Geometry Can the feature be reached by standard tools? Review depth, corner radius, wall thickness, tool clearance, and setup direction.
Tolerance Which dimensions are truly critical? Use tight tolerances only where function requires them and keep general dimensions practical.
Verification How will acceptance be checked? Define gauges, CMM checks, roughness measurement, thread inspection, or visual standards when needed.

How This Page Should Support Ranking

This topic can attract both beginner searches and buyer searches. The beginner wants a clear answer; the buyer wants enough detail to make a manufacturing decision. A page has a better chance to rank when it answers the simple question first, then adds examples, process limits, design notes, comparison tables, and practical next steps.

That is also why internal links should be helpful rather than forced. A reader should naturally move from this page to a process page, material page, surface finish page, inspection page, or quote page only when that next step solves a real question.

Conclusion

CNC machining can support medical device development when material, cleanliness, tolerance, finish, and inspection expectations are defined clearly from the start.

Categories
Blog CNC Materials Design, Cost & Sourcing

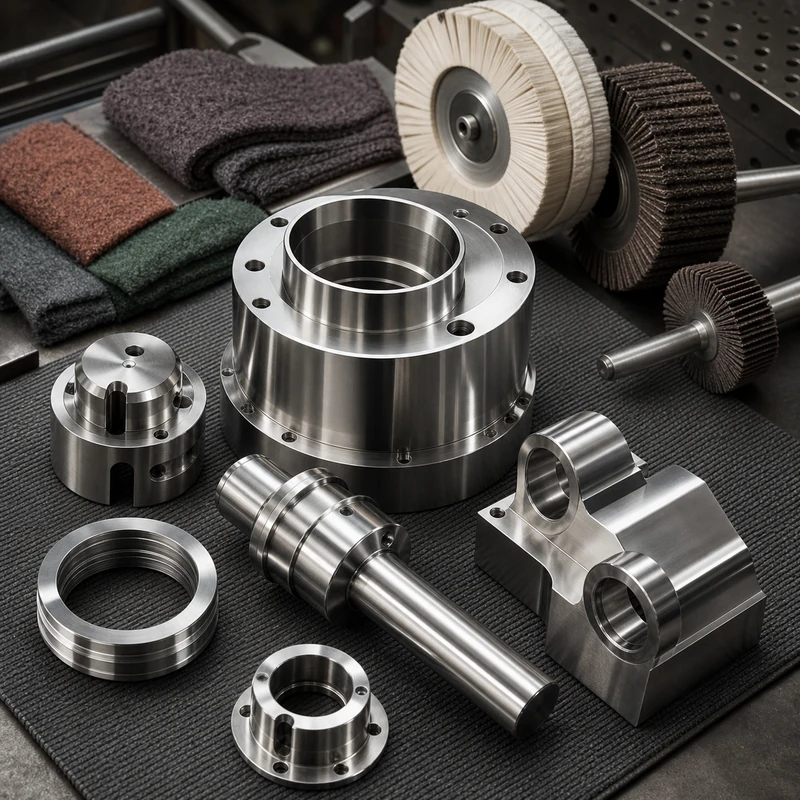
How to Polish Stainless Steel CNC Parts: Finishing Methods and Design Notes

Stainless steel CNC parts are polished to remove tool marks, improve appearance, reduce roughness, prepare for cleaning, or support corrosion-resistant service. The best method depends on the stainless grade, starting surface, part geometry, cosmetic expectations, and whether the finish is decorative, functional, or both.

Polishing should be planned before production rather than treated as a last-minute cosmetic step. MTSPi can combine stainless steel CNC machining, surface finish planning, and quality checks so machined features and finished surfaces match the drawing intent.

Why Polish Stainless Steel Parts?

  • Remove visible cutter marks, burr traces, scratches, or handling marks.
  • Create a brushed, satin, bright, or mirror-like appearance.
  • Reduce surface roughness where cleaning, sealing, or flow behavior matters.
  • Improve corrosion performance when polishing is paired with proper cleaning or passivation.
  • Prepare selected surfaces for assembly, inspection, or customer-facing use.

Common Polishing Methods

Method Typical Result Best Use
Deburring and edge blending Safer edges and cleaner transitions General machined parts before cosmetic finishing
Abrasive grinding Removes deeper tool marks and uneven areas Pre-polish correction or weld/stock cleanup
Brushing Uniform directional satin texture Panels, covers, brackets, visible housings
Buffing Bright reflective surface Decorative components and customer-facing hardware
Mirror polishing Very high reflectivity after staged abrasives Optical, medical, food, and premium cosmetic surfaces
Electropolishing Electrochemical smoothing and cleaning Complex stainless parts, hygienic surfaces, and corrosion-sensitive applications

A Practical Stainless Steel Polishing Workflow

1. Define the target finish

The finish should be described with a surface roughness value, visual standard, grain direction, sample photo, or approved reference part. Terms like “nice polish” or “shiny” are too vague for repeat production.

2. Machine with finishing allowance in mind

Polishing removes material. If a critical diameter, sealing surface, or flatness callout will be polished, the machining plan may need allowance and inspection after finishing. Tight features should not be polished aggressively unless the drawing accounts for it.

3. Remove defects gradually

Deep scratches, heavy cutter marks, and sharp edges should be reduced with controlled abrasives before fine polishing. Jumping directly to a fine compound can leave hidden waves, dull patches, or inconsistent reflections.

4. Clean and protect the part

After polishing, stainless steel parts should be cleaned to remove abrasive residue, compounds, oils, and loose particles. Depending on the application, passivation or electropolishing may be specified to improve surface cleanliness and corrosion behavior.

Stainless Steel Grades and Finish Behavior

Grade Family Polishing Notes Typical CNC Use
304 stainless steel Polishes well and is widely used for general corrosion resistance Housings, brackets, food equipment, covers
316 stainless steel Good corrosion resistance and common in harsher environments Medical, marine, chemical, and hygienic components
17-4 PH stainless steel Can be heat treated; finish planning should account for hardness condition High-strength shafts, fixtures, aerospace and industrial parts
303 stainless steel Machines well, but corrosion and finishing expectations should be checked Turned parts, fittings, fasteners, bushings

Design Notes Before Specifying a Polish

  • Avoid deep narrow pockets if the inside surfaces must be cosmetically polished.
  • Mark which faces are cosmetic and which are non-visible functional surfaces.
  • Specify grain direction for brushed finishes on panels or covers.
  • Confirm whether threaded holes, sharp edges, datums, and bores must be protected during finishing.
  • Define inspection after finishing when surface removal could affect tolerances.

Polishing vs Passivation vs Electropolishing

Mechanical polishing changes texture and appearance by physically smoothing the surface. Passivation chemically removes free iron and supports corrosion resistance. Electropolishing removes a thin surface layer electrochemically, which can smooth micro-peaks and improve cleanliness on suitable stainless parts. These processes can be combined, but they are not interchangeable.

Process Main Purpose Changes Dimensions?
Mechanical polishing Appearance and roughness control Yes, depending on abrasive stage and pressure
Passivation Surface chemistry and corrosion support Minimal dimensional change
Electropolishing Micro-smoothing, cleaning, and corrosion support Small controlled material removal

How MTSPi Supports Stainless Finishing

For stainless components, MTSPi reviews machining, polishing access, tolerance risk, edge requirements, cleaning, and inspection before production. Send your 3D model, drawing, stainless grade, target finish, cosmetic faces, and quantity through our RFQ channel.

Related MTSPi Resources

FAQ

Can all stainless steel CNC parts be mirror polished?

Not always. Mirror polishing depends on grade, geometry, access, starting surface, tolerance limits, and cost. Some internal features are impractical to polish uniformly.

Does polishing improve corrosion resistance?

A smoother and cleaner surface can help, but corrosion performance also depends on stainless grade, contamination control, passivation, environment, and maintenance.

Categories
Blog CNC Materials Quality & Tolerances

What Is Mechanical Testing? Methods, Data, and CNC Part Applications

Mechanical testing evaluates how a material, coupon, or finished component behaves under controlled load, impact, temperature, wear, or repeated stress. For CNC machined parts, it helps engineering teams confirm whether a selected metal or plastic can meet strength, durability, and safety requirements in real service.

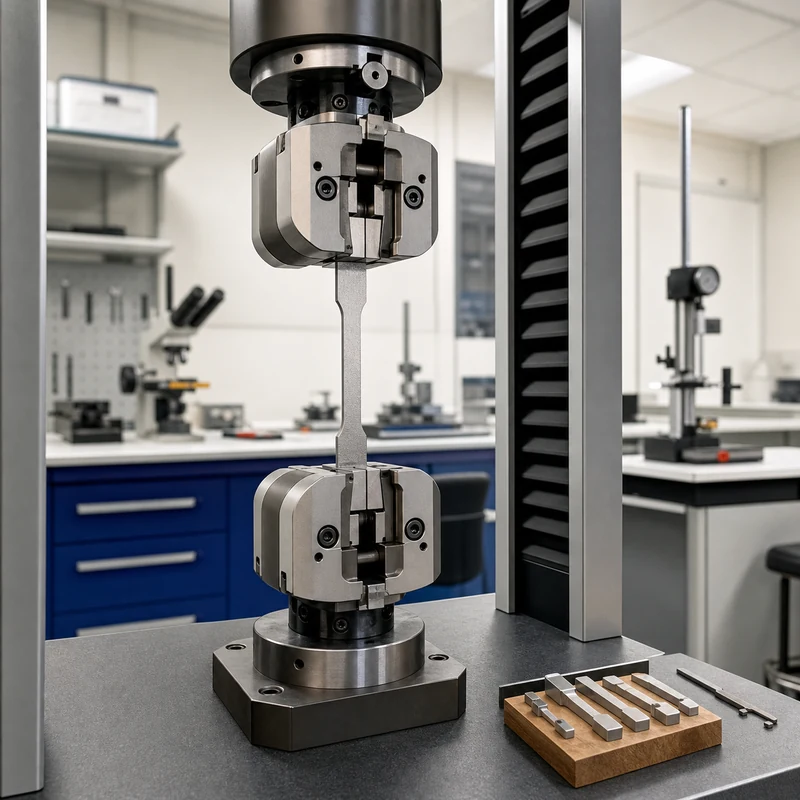
Mechanical testing is different from routine dimensional inspection. A caliper, micrometer, or CMM checks size and geometry; a mechanical test checks performance. MTSPi supports precision projects with quality assurance, material review, dimensional inspection, and documentation planning for custom machined parts.

What Mechanical Testing Measures

Property What It Shows Why It Matters for CNC Parts
Tensile strength Resistance to pulling force before fracture Useful for brackets, shafts, housings, fastened joints, and load-bearing parts
Yield strength Stress level where permanent deformation begins Helps prevent bent, distorted, or misaligned components
Hardness Resistance to indentation and local wear Important for sliding surfaces, tooling interfaces, pins, bushings, and wear parts
Impact toughness Ability to absorb sudden energy Relevant for parts exposed to shock, handling damage, or low-temperature service
Fatigue behavior Resistance to repeated cyclic loading Critical for moving assemblies, robotics, aerospace hardware, and vibration-prone parts

Common Mechanical Test Methods

Tensile testing

A prepared sample is pulled until it yields and eventually breaks. The resulting stress-strain curve can show elastic behavior, yield point, tensile strength, elongation, and fracture response. For production parts, tensile data is often supplied through material certificates rather than testing every machined component.

Compression and bending tests

Compression testing checks how a material behaves under squeezing load, while bend testing evaluates ductility and resistance to cracking. These methods are useful when parts see clamp loads, forming forces, press fits, or structural bending in service.

Hardness testing

Rockwell, Brinell, Vickers, and microhardness methods estimate resistance to indentation. Hardness checks are common after heat treatment, surface hardening, or material substitution, especially for steels, tool steels, stainless steels, and wear-focused components.

Impact and fracture tests

Impact testing measures how much energy a material absorbs during a fast strike. Fracture-related testing is useful when brittle failure, low-temperature exposure, or safety-critical loading must be understood before a design is released.

Fatigue testing

Fatigue testing repeats load cycles until cracks initiate or failure occurs. It is important for parts that rotate, vibrate, flex, or see repeated assembly loads. Fatigue risk is affected by material, surface finish, corners, threads, inclusions, and machining marks.

Mechanical Testing vs Dimensional Inspection

Check Type Primary Question Typical Tools
Dimensional inspection Does the part match the drawing size and geometry? CMM, micrometers, calipers, height gauges, pins, optical measurement
Mechanical testing Will the material or part perform under load or use conditions? Tensile frames, hardness testers, impact testers, fatigue rigs, environmental chambers
Surface and finish checks Is the surface suitable for wear, sealing, adhesion, or appearance? Profilometers, visual standards, coating-thickness gauges

When Buyers Should Request Mechanical Testing

  • The part is load-bearing, safety-related, or used in aerospace, medical, robotics, energy, or industrial machinery.
  • The drawing requires a material standard, heat treatment condition, hardness range, or certified test report.
  • A new material grade is being substituted for cost, supply, weight, or corrosion reasons.
  • The part has thin sections, stress concentrations, threads, press fits, or surfaces exposed to repeated load.
  • A prototype failed during use and the team needs to separate material issues from design or machining issues.

How Machining Can Affect Test Results

CNC machining can influence part performance through surface finish, residual stress, sharp internal corners, burrs, tool marks, heat input, and grain direction in stock material. A strong material can still fail early if the design creates high local stress or if finishing leaves a poor surface at a critical location.

  • Use generous internal radii where loads change direction.
  • Avoid unnecessary sharp notches around highly stressed features.
  • Specify surface roughness where fatigue, sealing, or sliding behavior matters.
  • Confirm heat treatment and hardness requirements before machining begins.
  • Keep material certificates tied to the correct lot and drawing revision.

Material Families and Testing Priorities

Material Family Common Tests Design Note
Aluminum alloys Tensile, hardness, fatigue, corrosion checks Useful for lightweight parts, but thread and fatigue design need care
Stainless steel Tensile, hardness, corrosion, impact where needed Good corrosion resistance, with grade-specific machinability and finishing behavior
Titanium Tensile, fatigue, fracture, hardness Strong lightweight option where heat control and surface condition are important
Engineering plastics Tensile, flexural, impact, creep, temperature exposure Performance depends strongly on temperature, moisture, and load duration

How MTSPi Uses Test Requirements

When a drawing includes mechanical testing or certification requirements, MTSPi reviews them during quoting so material choice, machining sequence, finishing, and inspection records line up with the final use. Share your CAD model, 2D drawing, material standard, required report type, and quantity through the contact page.

Related MTSPi Resources

FAQ

Is mechanical testing required for every CNC part?

No. Many parts only need dimensional inspection. Mechanical testing is most useful when material performance, certification, safety, or high-load service matters.

Can finished CNC parts be mechanically tested?

Sometimes. Many tests use standardized coupons, but finished parts can be tested in fixtures when the goal is to validate real assembly behavior.

Categories
Blog CNC Materials

What Is Cobalt Used For? Applications, Alloys, Properties, and Machining Notes

Quick answer: Cobalt is used for high-temperature alloys, lithium-ion batteries, magnets, cutting tools, wear-resistant coatings, pigments, catalysts, medical alloys, and corrosion-resistant components. In manufacturing, cobalt is valued for heat resistance, hardness, wear behavior, and alloy performance.

Why Cobalt Is Valuable

Cobalt is a metallic element often used as an alloying ingredient rather than as a pure structural material. It can improve high-temperature strength, hardness, wear resistance, corrosion behavior, and magnetic properties. These characteristics make it important in aerospace, energy, tooling, electronics, and medical applications.

Common Uses of Cobalt

Application Why cobalt is used Manufacturing note
Superalloys High-temperature strength and oxidation resistance Used in demanding turbine and aerospace environments
Batteries Electrochemical performance in certain battery chemistries Often discussed with nickel, lithium, and manganese systems
Magnets Magnetic performance and temperature stability Used in specialized magnetic materials
Cutting tools Hot hardness and wear resistance Cobalt-bearing tool steels and carbides improve cutting durability
Medical alloys Wear and corrosion resistance Requires strict material and quality control

Cobalt in Machining and Tooling

Many machinists know cobalt through cobalt high-speed steel drills and cutting tools. These tools can hold hardness at higher temperatures than ordinary HSS, making them useful for tougher metals when cutting conditions are appropriate.

Is Cobalt Easy to Machine?

Pure cobalt and cobalt-based alloys are not usually selected for easy machining. Many cobalt alloys are tough, heat-resistant, and abrasive to tools. Machining strategy may require rigid workholding, suitable tooling, conservative cutting parameters, coolant control, and careful inspection.

Cobalt Compared with Other Metals

Cobalt is often compared with nickel, titanium, stainless steel, and tool steel in demanding applications. For general CNC components, buyers usually choose a more common machinable metal unless cobalt alloy performance is specifically required.

Buyer Notes for Cobalt-Related Parts

  • Confirm the exact alloy, not just the word cobalt.
  • Define heat treatment and certification requirements.
  • Expect higher tooling difficulty for cobalt-based superalloys.
  • Review surface finish and inspection needs early.
  • Use an experienced supplier for high-value precision parts.

FAQ

Is cobalt a metal?

Yes. Cobalt is a metal and is commonly used as an alloying element in high-performance materials.

What is cobalt mostly used for?

Major uses include batteries, superalloys, magnets, cutting tools, catalysts, pigments, and medical alloys.

Is cobalt used in CNC machining?

Cobalt appears in some machined alloys and in cobalt-containing cutting tools, but many cobalt alloys are challenging to machine.

Is cobalt the same as nickel?

No. Cobalt and nickel are different metals, though they are both used in high-performance alloys and battery-related materials.

Need help choosing a machining route?

Send MTSPi your drawing, material, quantity, finish, and inspection requirements. We will review the part for manufacturability before quoting.

Contact MTSPi for a CNC machining quote

Practical Buyer Notes

Cobalt pages can rank for general science-style searches, but for MTSPi they should connect the material to manufacturing uses. The best content explains cobalt in alloys, cutting tools, batteries, magnets, coatings, and high-temperature applications.

Pure cobalt is not usually the everyday CNC material buyers request. More often, cobalt appears in cobalt-bearing alloys, cobalt chrome, tool steels, carbide tooling, or superalloys. This distinction makes the page more useful and more trustworthy.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Application Explain batteries, magnets, superalloys, tools, and medical alloys Covers broad search intent
Material form Separate pure cobalt from cobalt-containing alloys Prevents misleading manufacturing advice
Machinability Mention toughness, heat resistance, and tool wear Connects the topic to CNC decisions
Buyer action Ask for exact alloy grade and certification needs Improves quote accuracy

Common Mistakes to Avoid

  • Talking about cobalt only as a battery material.
  • Suggesting all cobalt materials machine the same way.
  • Ignoring cobalt chrome, superalloys, and cobalt cutting tools.
  • Leaving out safety, certification, and exact alloy identification.

Recommended MTSPi Review Workflow

When a buyer mentions cobalt, MTSPi should first identify the exact alloy and application. Then the review should cover machinability, heat treatment, certification, surface finish, and inspection requirements.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send the exact alloy grade, drawing, operating temperature, certification requirement, quantity, finish, and whether the part is prototype or production.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Cobalt Alloy Buyer Considerations

When cobalt is part of a machining discussion, the exact alloy matters more than the word cobalt itself. Cobalt chrome, cobalt-bearing tool steel, cobalt-based superalloys, and battery-related cobalt compounds have very different properties and manufacturing requirements. A CNC supplier needs the actual material grade, not only a general material family.

Buyers should also clarify whether the part requires certification, heat treatment, special inspection, or controlled surface finish. Cobalt-related materials are often selected for demanding environments, so unclear specifications can create cost, tooling, and quality risks.

Conclusion

Cobalt is important because it improves performance in demanding environments. For CNC buyers, the key is to identify the exact cobalt alloy, understand machining difficulty, and define quality requirements before production begins.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

What Is Cobalt Used For? Applications, Alloys, Properties, and Machining Notes

We'll Send You Back with Price Immediately!