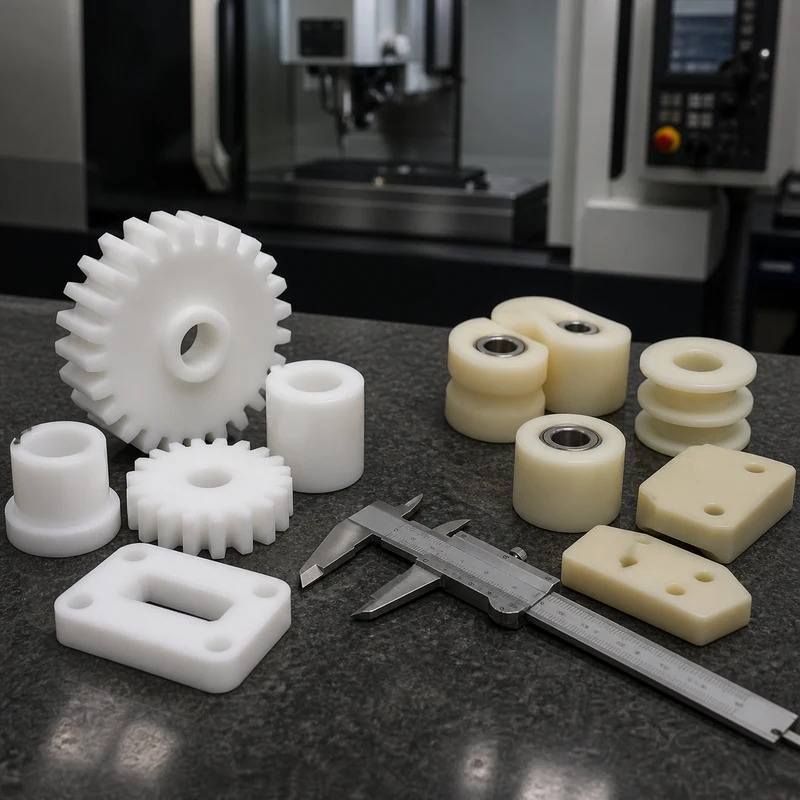
Acetal and nylon are two of the most useful engineering plastics for machined gears, rollers, bushings, guides, and structural components. They can look similar on a drawing, but they respond differently to humidity, impact, sustained load, friction, and tight tolerances. Acetal is usually the more predictable choice for dimensional stability and smooth precision motion. Nylon is often stronger when a component must absorb shock, tolerate abrasion, or flex without cracking.
This is not a simple good-versus-bad comparison. Both material families contain multiple grades, fillers, and stock forms. The right decision comes from the actual load case, environment, geometry, tolerance scheme, and inspection condition. This guide compares acetal (often specified as POM or by the Delrin trade name) with common machinable nylons from a design-for-manufacturing perspective.
Acetal vs Nylon: Quick Engineering Comparison
| Decision factor |
Acetal / POM |
Nylon |
| Typical design priority |
Stable dimensions and low-friction precision motion |
Toughness, impact absorption, and abrasion resistance |
| Moisture response |
Low absorption; comparatively stable in humidity |
Absorbs moisture; dimensions and properties can change |
| Stiffness |
Generally high and consistent |
Grade- and moisture-dependent; often more compliant |
| Impact behavior |
Good, but less forgiving at notches |
Generally tougher under shock and repeated loading |
| Wear and sliding |
Excellent for controlled sliding and gears |
Excellent for wear pads, guides, and rugged contact |
| Machining behavior |
Clean chips and good tolerance control |
Can produce stringy chips and move after unclamping |
| Creep under load |
Must be checked |
Must be checked; reinforced grades may help |
| Best starting point |
Close fits, valve parts, precision gears, spacers |
Wear pads, pulleys, rollers, impact-loaded components |
These are broad tendencies rather than certified values. Resin type, conditioning, reinforcement, stock-production method, temperature, test direction, and supplier all matter. Always approve the exact grade using its current technical data and any required compliance documentation.
What Is Acetal?
Acetal is the engineering-plastic family known chemically as polyoxymethylene, or POM. It is available as homopolymer and copolymer formulations. Delrin is a trade name associated with a particular acetal homopolymer, so a drawing that says only “Delrin” may not be equivalent to every generic acetal grade. Procurement documents should identify the exact resin or an approved-equivalent rule.
Machined acetal is valued for stiffness, low friction, fatigue performance, clean machinability, and low moisture absorption. These traits make it a practical choice for dimensional spacers, small gears, bearing cages, valve components, electrical insulators, and mechanisms that need repeatable motion. It also tends to produce a crisp machined surface when tools are sharp and heat is controlled.
Homopolymer vs Copolymer POM
Homopolymer POM often offers somewhat higher stiffness and strength, while copolymer grades may provide improved resistance to hot water, alkaline environments, and centerline porosity in larger cross-sections. The meaningful difference depends on grade and stock size. For a sealing bore, pressure component, or thick machined section, do not substitute between them without engineering review.
What Is Nylon?
Nylon refers to a broad polyamide family rather than one uniform material. Nylon 6, nylon 6/6, cast nylon, nylon 12, and reinforced or lubricant-filled grades can behave quite differently. Common nylons combine toughness, fatigue resistance, and excellent abrasion performance, making them useful for rollers, sprockets, wear strips, pulleys, guides, and mechanical components exposed to vibration or intermittent shock.
The defining design issue is moisture absorption. Nylon equilibrates with its surroundings, and absorbed water can change its size, stiffness, and toughness. That can be beneficial for impact behavior but problematic for a close sliding fit or a tightly located hole pattern. Engineering and inspection must agree on whether dimensions apply to dry-as-machined, conditioned, or service-equilibrated material.
The Differences That Matter in Real Parts
Dimensional Stability and Moisture
Acetal is normally easier to control when humidity changes or when the part has a close fit. Nylon can swell after machining as it absorbs moisture, and the amount is affected by grade, wall thickness, time, and exposure. A tolerance that is achievable at the machine may not represent the dimension after conditioning or field service.
For nylon, identify the conditioning state on the drawing or purchase specification. Allow clearance where function permits, avoid blanket tight tolerances, and inspect at a controlled temperature and moisture condition. For either plastic, thin walls and asymmetric stock removal can release internal stress and cause movement.
Stiffness, Toughness, and Impact
Acetal is often selected when rigidity preserves gear alignment, bearing clearance, or positional accuracy. Nylon is usually more forgiving under impact and repeated deflection. Yet geometry can outweigh the generic material trend: a sharp corner, thin snap arm, press fit, or molded-in stress raiser can fail even in a nominally tough resin.
Use generous transitions, remove sharp internal corners, distribute fastener loads, and verify short-term strength separately from long-term creep. Filled grades can increase stiffness but may reduce impact strength or create direction-dependent behavior.
Friction, Wear, and Counterface
Both families can work well in sliding mechanisms. Acetal commonly provides smooth low-friction motion and predictable gear or bearing geometry. Nylon is widely used where abrasive contact and shock occur together. Actual life depends on pressure, velocity, heat generation, lubrication, debris, shaft material, surface finish, alignment, and duty cycle—not the plastic name alone.
A wear pair should be tested as a system. A very rough metal shaft can rapidly abrade a polymer, while an excessively smooth or incompatible counterface may not retain lubricant. Filled or internally lubricated grades should be evaluated when dry running or high duty is expected.
Temperature, Creep, and Chemical Exposure
Neither material behaves like a metal under sustained heat and clamp load. Strength and modulus fall as temperature rises, and creep can relax a bolted joint or distort a bearing seat over time. Nylon grades may retain useful toughness at elevated temperature, while acetal may keep dimensions more predictably in ordinary humid service. Grade-specific curves are essential near any limit.
Both resist many oils, greases, and fuels, but neither is chemically universal. Check the exact fluid, concentration, temperature, stress level, and exposure duration. Cleaning agents, thread lockers, and assembly lubricants deserve the same review as the primary process chemical.
CNC Machining Acetal and Nylon
| Machining issue |
Acetal planning |
Nylon planning |
| Cutting edge |
Sharp polished carbide; maintain a real chip |
Sharp positive geometry; prevent rubbing and stringy recutting |
| Heat control |
Evacuate chips and avoid dwell |
Control heat carefully because local softening encourages movement |
| Workholding |
Broad support without crushing |
Support flexible walls and avoid clamp distortion |
| Finishing pass |
Allow the part to stabilize before final sizing |
Rough, relax, then finish when tight geometry warrants it |
| Threads |
Good detail, but avoid excessive interference |
Use adequate engagement; inserts or through-bolts may be safer |
| Inspection |
Control temperature and fixturing |
Define moisture condition as well as temperature |
Successful CNC plastic machining removes heat with the chip. Rubbing, dull tools, excessive spindle speed, or repeated chip recutting can smear an edge and build residual stress. Air or a verified compatible coolant can help, but the fluid must not attack the polymer or contaminate a regulated part.
Practical Acetal Machining Guidance
- Use stable, traceable stock and confirm homopolymer or copolymer before production.
- Keep cutting tools sharp and avoid dwell marks at finished surfaces.
- Support thin rings and long walls without creating ovality or clamp witness.
- Use realistic press-fit allowances; excessive interference can split a hub over time.
- Deburr by controlled cutting rather than melting or heavy edge rounding.
Practical Nylon Machining Guidance
- State the material grade and conditioning state explicitly.
- Use positive cutting geometry and evacuate continuous chips safely.
- For tight features, consider rough machining followed by stress relaxation and finish machining.
- Allow the part to stabilize before final measurement.
- Protect long, flexible features from tool pressure and workholding distortion.
How to Choose by Application
| Application condition |
Likely starting point |
What to verify |
| Precision gear or index component |
Acetal |
Tooth load, backlash, temperature, lubricant, and life |
| Close-fit bushing in changing humidity |
Acetal |
PV limit, shaft finish, clearance, and creep |
| Impact-loaded roller or pulley |
Nylon |
Shock load, moisture state, bearing retention, and wear |
| Wear pad or guide rail |
Nylon |
Counterface, debris, pressure, velocity, and lubrication |
| Valve or fluid-handling component |
Acetal grade selected for media |
Chemical compatibility, pressure, temperature, and porosity |
| Large structural plastic plate |
Cast nylon may be attractive |
Flatness, internal stress, conditioning, and creep |
| Food or medical contact part |
Certified grade only |
Applicable regulation, traceability, cleaning, and validation |
Design Rules That Reduce Failure Risk
- Specify the family and exact grade. “Plastic,” “nylon,” or “acetal” alone leaves too much room for substitution.
- Define the service environment. Include humidity, immersion, temperature range, chemicals, UV exposure, and duty cycle.
- Tolerance only the interfaces that matter. Plastic dimensions respond to temperature, moisture, stress, and fixturing.
- Avoid sharp stress concentrators. Add corner radii and smooth section changes.
- Design fasteners for creep. Use washers, shoulders, metal inserts, or through-bolts where appropriate.
- Account for thermal expansion. Do not trap a long plastic component between rigid metal boundaries without clearance.
- Separate cosmetic and functional surfaces. Deburring, polishing, and protective handling can affect critical edges.
Cost: Compare the Finished System, Not Stock Price
Standard nylon stock may appear less expensive than a specified acetal grade, but material price is only one input. Add machining time, stabilization steps, scrap risk, inspection, assembly method, lubrication, maintenance, and expected service life. A stable acetal part may be cheaper if it avoids post-machining movement; a tougher nylon component may be cheaper if it survives shock and abrasive duty longer.
RFQ Checklist
- Controlled 3D model and 2D drawing
- Exact resin, grade, color, filler, and approved equivalents
- Stock form and required material certification
- Quantity and prototype-to-production plan
- Critical datums, fits, tolerances, and inspection condition
- Load, speed, temperature, humidity, chemicals, and expected life
- Counterface material, finish, lubrication, and debris exposure
- Threads, inserts, press fits, assembly torque, and cosmetic requirements
MTSPi can review these inputs through its CNC machining services, dedicated acetal machining and nylon machining capabilities, and quality assurance workflow.
Frequently Asked Questions
Is Delrin the same as acetal?
Delrin is a trade name for a specific POM homopolymer. Acetal is the wider POM family, which also includes copolymers. Use the exact grade on production documents.
Which material holds a tighter tolerance?
Acetal is usually the easier starting point because it absorbs less moisture. Geometry, stock stress, temperature, fixturing, and measurement method still control the achievable result.
Which is better for gears?
Acetal suits precise, low-friction gears; nylon can suit tougher or shock-loaded gears. Tooth load, heat, lubrication, backlash, and life testing should decide.
Can nylon be machined accurately?
Yes. Accurate nylon parts require suitable stock, sharp tools, controlled heat and workholding, stabilization, and a defined moisture condition.
Can both materials use threaded inserts?
Yes, but insert style, installation method, wall thickness, torque, temperature, and creep must be validated for the exact grade.
Conclusion
Choose acetal when stable dimensions, stiffness, clean machinability, and smooth low-friction motion lead the requirements. Choose nylon when toughness, abrasion resistance, and impact absorption matter more. Then verify the decision against the exact grade, conditioning state, environment, tolerance plan, counterface, and lifetime load—not a generic property chart.
Related MTSPi Resources