Categories
Blog CNC Materials Quality & Tolerances

Datums in CNC Machining: A Practical GD&T and Inspection Guide

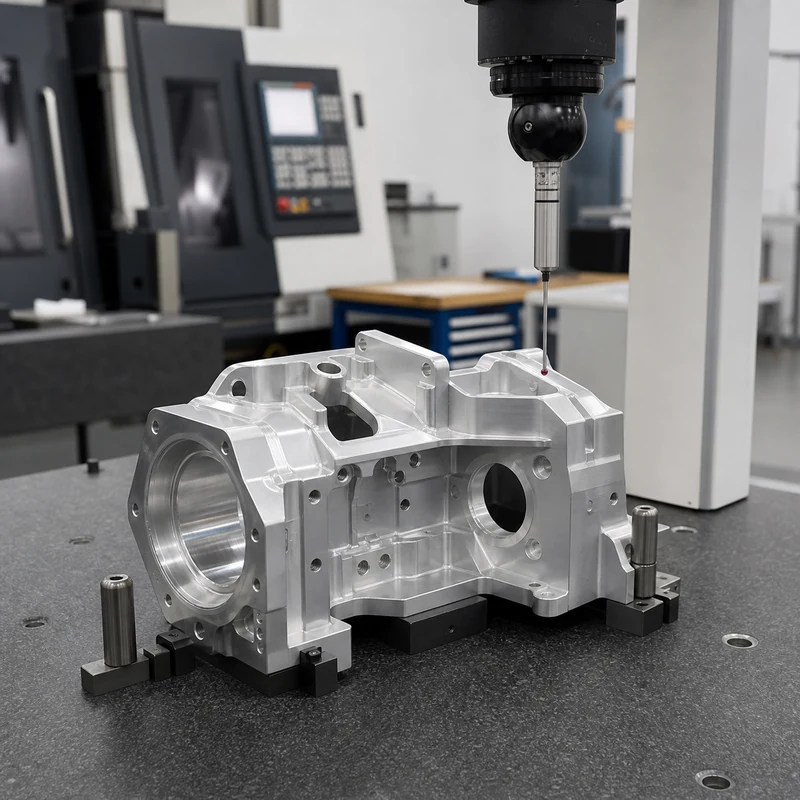
A datum is an exact theoretical point, axis, or plane used to establish a measurement reference. A physical surface, hole, slot, or other feature on the part is a datum feature; inspection equipment or fixture contacts simulate that feature to establish the datum. Keeping those terms distinct helps a drawing translate into repeatable machining, assembly, and inspection.

For precision parts, MTSPi connects drawing intent to setup planning, multi-operation transfer, and quality assurance so the same functional references guide production and measurement.

Datum, Datum Feature, and Datum Feature Simulator

Term Meaning Example
Datum Perfect theoretical reference A plane derived from a mounting face
Datum feature Real part feature identified on the drawing The actual mounting face or locating bore
Datum feature simulator Equipment that contacts or represents the feature Surface plate, fixture pad, pin, mandrel, or CMM alignment

The real feature contains manufacturing variation. The datum is ideal. The simulator creates a repeatable relationship between the real part and the ideal reference used for evaluation.

How a Datum Reference Frame Constrains a Part

A common primary-secondary-tertiary scheme follows the 3-2-1 principle. The primary datum feature typically contacts three points and removes three degrees of freedom. The secondary feature contacts two points and removes two more. The tertiary feature uses one point to remove the final degree of freedom. Together they establish the datum reference frame named in a feature-control frame.

Datum order Typical role Degrees of freedom constrained
Primary (A) Stable functional base or broad surface Three
Secondary (B) Side surface, bore, or slot establishing direction Two
Tertiary (C) Final stop or clocking feature One

Why Datum Order Matters

A-B-C is not interchangeable with B-A-C. The first reference dominates how the part is oriented, while later references finish its location. Changing the order can change the measured position or orientation of features. Datum precedence should therefore reflect assembly function, not simply whichever surface is easiest for the machinist to touch.

Datums Across Design, Machining, and Inspection

Stage How datums are used Failure if inconsistent
Design Express functional relationships through GD&T A drawing may control the wrong interface
Process planning Choose workholding and operation sequence Tolerance stack grows across re-clamping
Machining Set work coordinates and transfer references Features shift between setups
Inspection Align CMM or gaging to the specified frame Good parts fail or bad parts pass
Assembly Locate mating components Fit, sealing, motion, or alignment problems

Choosing Functional Datum Features

  • Start with the surfaces or axes that locate the part in its real assembly.
  • Choose a primary feature that is stable, accessible, and large enough to establish orientation.
  • Use secondary and tertiary features that control functional direction and clocking.
  • Avoid rough cast, flexible, interrupted, or easily damaged features unless they truly represent function.
  • Consider how the features can be simulated in both production fixtures and inspection equipment.
  • Keep the datum scheme compatible with service loads, mating parts, and maintenance needs.

Common Datum Feature Types

Planar surfaces

Mounting faces are common primary datum features because they can provide stable orientation. Flatness and contact distribution still matter.

Holes and cylindrical features

A bore can establish a datum axis, while a pin pattern can locate and clock a part. Clearance, material boundary modifiers, and simulator type affect how the frame is established.

Slots and tabs

Center planes derived from width features can locate a part while allowing controlled movement in another direction.

Datum targets

Targets define selected points, lines, or areas and are useful for castings, forgings, sheet structures, and irregular surfaces where full-surface contact would be unstable.

Datums Versus Machine Zero

The machine coordinate system and work offset are programming tools. A drawing datum is a design and inspection reference. A programmer may align a work offset with a datum for convenience, but they are not automatically the same. Setup documentation should explain the transformation so dimensions remain traceable through every operation.

Multi-Setup and 5-Axis Parts

Complex parts often cannot retain the functional datums in one clamping. Process planners may create temporary machining references, precision soft jaws, or qualified fixture features. The important point is to control the transfer back to the drawing reference frame. On 5-axis CNC machining projects, a strong datum plan can reduce re-clamping, but inspection still has to reconstruct the specified frame correctly.

Frequent Datum Mistakes

  • Labeling a theoretical plane as though it were the physical surface.
  • Selecting cosmetic or convenient faces instead of functional interfaces.
  • Using unstable features that rock or deform in a fixture.
  • Failing to preserve datum relationships across secondary operations.
  • Inspecting from shop-friendly references that differ from the drawing.
  • Over-constraining a part with incompatible fixture contacts.
  • Omitting datum order or material-boundary requirements where they matter.

Drawing Review Checklist

  • Do A, B, and C reflect how the part mates and carries load?
  • Can each datum feature be reached by the fixture and CMM probe?
  • Are flexible or unfinished surfaces controlled appropriately?
  • Does each positional or orientation tolerance reference the intended frame?
  • Are datum targets, basic dimensions, and feature-control frames unambiguous?
  • Can the machining sequence preserve or accurately re-establish the frame?

FAQ

Can a hole be a datum?

Yes. The hole is the datum feature, and its derived axis can establish the datum.

What do Datum A, B, and C mean?

They identify datum features in precedence order: primary, secondary, then tertiary.

Does every CNC part need three datums?

No. The reference structure should be only as complex as the functional geometry requires.

Can an inspection setup use different datums?

Intermediate checks may use process references, but final acceptance must evaluate requirements from the datum reference frame specified on the drawing.
Related MTSPi Resources

Categories
Blog CNC Materials Guides Quality & Tolerances

3/8-16 Tap Drill Size: CNC Threading and Design Guide

For a standard 3/8-16 UNC internal thread, the usual tap-drill recommendation is a 5/16-inch drill (0.3125 inch or 7.94 mm). That combination gives a practical balance between thread engagement, tapping torque, tool life, and assembly strength. It is a starting point, however—not a substitute for checking the material, thread class, hole depth, tap style, and joint load.

MTSPi reviews threaded features as part of its CNC machining services, including drill depth, tap clearance, edge distance, inspection access, and the risk of chip packing in blind holes.

What 3/8-16 UNC Means

The designation describes a Unified National Coarse thread. The nominal fastener diameter is 3/8 inch and there are 16 thread pitches per inch. Its pitch is 0.0625 inch (1.5875 mm). Coarse threads are commonly chosen for fixtures, machine frames, brackets, housings, and industrial assemblies because they assemble quickly and generally tolerate contamination and minor handling damage better than fine threads.

Item Nominal value Design significance
Major diameter 0.375 in (9.525 mm) Nominal screw size
Pitch 16 TPI / 0.0625 in Axial distance between threads
Common tap drill 5/16 in / 0.3125 in General-purpose cut-tap starting size
Thread family UNC Unified coarse series

Tap Drill Options and Tradeoffs

A smaller drilled hole produces greater theoretical thread engagement but also raises torque, heat, and breakage risk. A larger hole reduces cutting load but leaves less thread material. Actual results also depend on drill runout, material springback, tap geometry, coating, and whether the thread is cut or formed.

Drill Decimal diameter Typical effect
19/64 in 0.2969 in High engagement and substantially higher tapping load; use only with an engineered reason
5/16 in 0.3125 in Common general-purpose choice for a 3/8-16 cut thread
21/64 in 0.3281 in Lower engagement and lower torque; suitability must be verified against load and thread class

The simple shop approximation—nominal diameter minus pitch—also points to 0.3125 inch: 0.375 minus 0.0625. Final sizing should follow the applicable thread standard and the tap manufacturer’s data, especially for safety-critical parts.

Cut Taps, Form Taps, and Thread Milling

Method Best fit Important planning point
Cut tapping General metals and conventional threaded holes Choose spiral-point taps for many through holes and spiral-flute taps for blind-hole chip evacuation
Form tapping Ductile materials where chip-free production is useful Requires a different, larger pre-hole; never apply the cut-tap drill chart blindly
Thread milling Large, costly, difficult, or tolerance-sensitive parts Offers diameter adjustment and easier recovery if the tool fails

A Reliable CNC Process

  1. Confirm the specification. Check 3/8-16 UNC, thread class, minimum full-thread depth, through or blind condition, and any insert requirement.
  2. Spot and drill. Control drill runout and verify the actual hole rather than relying only on nominal tool size.
  3. Chamfer the entrance. A controlled lead-in helps the tap start squarely and protects the first thread.
  4. Tap or thread mill. Match speed, lubricant, and tool geometry to the work material.
  5. Deburr and clean. Remove chips without rolling burrs into the thread.
  6. Inspect. Use the specified GO/NO-GO gage and verify depth and location.

Material-Specific Notes

Material Main risk Useful control
Aluminum Built-up edge and chip adhesion Sharp geometry, suitable lubricant, and good blind-hole evacuation
Carbon/alloy steel Torque increases with hardness Rigid setup, appropriate coating, stable speed and feed
Stainless steel Work hardening and heat Avoid dwell, maintain feed, use effective lubrication
Titanium Heat concentration and seizure Conservative speed, strong lubrication, short engagement, consider thread milling

Thread Depth and Blind-Hole Allowance

The drawing should distinguish full usable thread from total drilled depth. A blind hole needs room for the drill point, tap lead, chips, and bottom clearance. Calling out an impossible full thread to the exact bottom drives unnecessary risk. As a broad design starting point, steel joints often use engagement near one nominal diameter, while lower-strength materials may need more; the joint calculation and insert strategy govern the final value.

Common Failure Modes

  • Using the form-tap pre-hole for a cut tap, or the reverse.
  • Programming feed that is not synchronized to 16 TPI during rigid tapping.
  • Ignoring tap lead length when specifying a blind thread.
  • Allowing chips to pack at the bottom of a hole.
  • Applying a tight thread requirement without defining class or gaging.
  • Placing the thread too close to an edge or thin wall.

Design and RFQ Checklist

  • State 3/8-16 UNC and the required class of fit.
  • Identify through versus blind holes and minimum full-thread depth.
  • Show counterbores, spotfaces, chamfers, inserts, and sealing functions.
  • Specify material and heat-treated condition.
  • Identify critical position tolerances and their datum references.
  • Define inspection documentation if a thread-gage record is required.

FAQ

What is the standard drill for a 3/8-16 tap?

For a conventional cut tap, 5/16 inch is the widely used starting recommendation.

Can 8 mm replace 5/16 inch?

Eight millimeters is about 0.3150 inch, slightly larger than 5/16. It may be workable in some noncritical applications, but the resulting engagement and thread requirements must be reviewed.

Is the same drill used for a form tap?

No. Form taps displace material and normally require a larger pre-hole specified by the tool maker.

How should a 3/8-16 thread be inspected?

A calibrated GO/NO-GO plug gage is common, supplemented by depth, location, and visual checks required by the drawing.

Related MTSPi Resources

Categories
Blog CNC Materials Guides Quality & Tolerances

14 Gauge Steel Thickness: Inch, mm, Weight, Uses, and Fabrication Notes

Quick answer: 14 gauge steel is commonly about 0.0747 in, or about 1.90 mm, for standard sheet steel. Exact thickness can vary by material type and gauge standard, so buyers should confirm the specification instead of relying only on the gauge number.

14 Gauge Steel Thickness Chart

Material / gauge reference Approx. thickness Notes
Standard steel, 14 gauge 0.0747 in / 1.90 mm Common reference for sheet steel
Galvanized steel, 14 gauge May differ slightly by standard Confirm coating and base metal requirements
Stainless steel, 14 gauge Often close but not always identical Check supplier chart and tolerance
Aluminum gauge Different from steel gauge Do not substitute steel gauge values for aluminum

Why Gauge Numbers Can Be Confusing

Gauge is a traditional sheet thickness system, and the same gauge number can mean different thicknesses for steel, stainless steel, aluminum, and nonferrous metals. A drawing should ideally show the actual thickness in inches or millimeters, especially when fit, weight, stiffness, or forming matters.

Common Uses for 14 Gauge Steel

  • Brackets, panels, guards, covers, and machine frames
  • Enclosures and equipment housings
  • Welded fabrication parts
  • Automotive and industrial sheet metal components
  • Fixtures, mounting plates, and support parts

Fabrication and CNC Machining Notes

14 gauge steel is thick enough for many structural sheet applications while still being practical for cutting, bending, welding, and finishing. For machined features, hole size, edge distance, bend radius, flatness, and finish requirements should be reviewed before production.

Design Checklist for 14 Gauge Parts

Design item Recommendation Reason
Hole edge distance Avoid holes too close to bends or edges Reduces tearing and distortion
Bend radius Match tooling and material condition Improves forming consistency
Tapped holes Use inserts or weld nuts when thread strength is limited Thin sheet does not provide much thread engagement
Surface finish Plan powder coating, plating, or brushing early Finishing affects appearance and protection

When to Use CNC Machined Parts Instead

If the part needs thick bosses, precise pockets, tight positional tolerances, machined sealing surfaces, or complex 3D geometry, a machined plate or billet part may be better than sheet metal. Compare options with CNC milling services and the metal material guide.

FAQ

How thick is 14 gauge steel in mm?

A common value is about 1.90 mm for standard sheet steel, but always confirm the exact standard and material.

Is 14 gauge steel strong?

It is stronger and stiffer than thinner sheet gauges, but strength depends on material grade, part shape, bends, supports, and load direction.

Can 14 gauge steel be bent?

Yes, but bend radius, tooling, grain direction, and material grade should be considered.

Is 14 gauge stainless the same thickness as 14 gauge steel?

Not always. Gauge charts can vary by material, so specify actual thickness when accuracy matters.

Need help choosing a machining route?

Send MTSPi your drawing, material, quantity, finish, and inspection requirements. We will review the part for manufacturability before quoting.

Contact MTSPi for a CNC machining quote

Practical Buyer Notes

Gauge pages can attract traffic because users often need a quick thickness answer, but they rank better when they go beyond a number. The page should explain why gauge varies by material, how thickness affects fabrication, and when CNC machining is a better option.

14 gauge steel is often used in panels, brackets, guards, housings, and fabricated assemblies. Buyers should confirm actual thickness in inches or millimeters because gauge standards are not universal across steel, stainless steel, galvanized steel, and aluminum.

How to Evaluate This Topic on a Real Drawing

Decision point Recommended approach Why it matters
Thickness callout Use exact inch or mm thickness on drawings Avoids confusion from gauge charts
Fabrication route Use sheet metal cutting and bending for thin formed parts Often cheaper than machining from billet
Machined features Use CNC when precise pockets, bores, or thick bosses are needed Sheet metal alone may not create complex 3D features
Finish Plan powder coating, plating, or brushing before quoting Finish affects edge quality and corrosion protection

Common Mistakes to Avoid

  • Assuming 14 gauge means the same thickness for every material.
  • Trying to tap strong threads directly into thin sheet without inserts or hardware.
  • Ignoring bend radius, hole-to-edge distance, and coating thickness.
  • Using gauge values instead of actual thickness on production drawings.

Recommended MTSPi Review Workflow

For gauge-related pages, MTSPi should answer the thickness first, then explain fabrication decisions, design constraints, material options, and whether CNC machining or sheet metal production fits better.

  1. Confirm the part function, operating environment, and assembly risk.
  2. Review material, process, tolerance, surface finish, and inspection requirements together.
  3. Separate critical features from general dimensions so cost is not wasted on non-functional details.
  4. Use related resources such as CNC materials, surface treatment, and quality assurance to complete the specification.
  5. Send the final drawing package to MTSPi for quote review before production.

What to Send for a Faster Quote

Send actual thickness, material grade, flat pattern or 3D model, bend notes, finish requirements, and any hardware or threaded feature expectations.

  • 3D CAD file and 2D drawing with revision number.
  • Material grade or acceptable alternatives.
  • Quantity, delivery target, and whether samples are required first.
  • Critical dimensions, thread callouts, finish notes, and inspection requirements.
  • Application notes when the part is used in heat, moisture, wear, vibration, or visible assemblies.

Conclusion

14 gauge steel is a useful thickness for durable sheet metal parts, but gauge alone is not enough for a precise manufacturing requirement. Use actual inch or millimeter thickness, define material grade, and review forming, finishing, and inspection needs before production.

Categories
Blog CNC Materials Guides Quality & Tolerances

Tungsten Metal for CNC Machined Parts: Properties, Uses, and Design Notes

Tungsten is one of the most demanding metals a CNC machining team can be asked to produce. It is dense, heat resistant, wear resistant, and useful in severe-duty applications, but those same strengths make it harder to cut, fixture, inspect, and finish than common aluminum or stainless steel parts. For engineered components, the practical question is not only what tungsten can withstand. The project also has to account for brittleness, tool wear, tolerance risk, material cost, and the right choice between pure tungsten, heavy alloy, and tungsten carbide.

MTSPi supports CNC metal machining for difficult materials and can help review tungsten part drawings before production so machining strategy, tolerances, finish, and inspection requirements are aligned early.

What Is Tungsten?

Tungsten, also called wolfram, is a metallic element with the symbol W and atomic number 74. It is best known for having the highest melting point of any pure metal. In machined-part design, it is usually selected for one of four reasons: high-temperature stability, compact mass, wear resistance, or shielding performance.

Property Typical Tungsten Value Why It Matters in CNC Parts
Chemical symbol W Useful shorthand for material specifications and alloy discussions
Density About 19.3 g/cm3 Creates high mass in compact parts such as counterweights and shielding
Melting point About 3422 C Supports high-temperature service where many metals soften
Appearance Silver-gray metallic Can be machined and finished for technical components
Hardness Very high Improves wear resistance but raises tool-wear and edge-chipping risk
Corrosion behavior Strong in many environments Still requires review against the actual chemicals and temperature

Why Engineers Choose Tungsten

Extreme Heat Resistance

Tungsten keeps useful mechanical stability at temperatures that would be unacceptable for many engineering metals. This makes it relevant for furnace hardware, high-temperature tooling, electrical contacts, aerospace systems, and other parts exposed to heat cycling.

High Density in a Small Volume

Because tungsten is much denser than steel, it can add mass without forcing a large part envelope. That is valuable for counterweights, balance components, vibration control parts, medical shielding, and compact industrial assemblies where space is limited.

Wear Resistance

Tungsten and tungsten-based materials can resist abrasion and mechanical wear. This makes them attractive for high-load components, contact surfaces, tooling-related parts, and assemblies that need a long service life under friction.

Pure Tungsten, Tungsten Alloy, and Tungsten Carbide

The word tungsten can refer to several different material families. The correct choice depends on the application and on how much machining risk the design can tolerate.

Material Main Strength Common CNC Design Note
Pure tungsten Highest temperature capability and density Brittle and difficult to machine; avoid unnecessary sharp internal features
Tungsten heavy alloy Better toughness and more practical machinability Often a better option for precision machined weights, shielding, and structural parts
Tungsten carbide Exceptional hardness and wear resistance Usually treated as a tooling or wear material rather than a normal machined metal

Advantages and Limitations

Tungsten is a high-performance choice, not a default material. It should be specified when the operating requirement justifies the manufacturing difficulty.

Advantage Manufacturing Limitation
Handles extreme temperatures Machining time is usually longer than common metals
Very high density Material cost and shipping weight can be significant
Excellent wear resistance Cutting tools wear quickly without a controlled process
Good dimensional stability in demanding service Brittleness can cause cracking, edge breakage, or scrap
Useful for shielding and compact mass Tight tolerances require stable fixturing and careful inspection planning

Applications for Tungsten Machined Parts

Industry Typical Uses Important RFQ Detail
Aerospace Balance weights, hot-zone parts, ballast, and high-density components Define load, temperature, and inspection requirements
Medical and imaging Radiation shielding, collimators, dense inserts, and instrument components Confirm material traceability and cleanliness expectations
Electronics Contacts, heat-related parts, and dense precision features Specify surface condition and burr limits
Industrial equipment Wear parts, tooling supports, vibration damping parts, and heavy-duty mechanisms Identify wear surfaces and critical fits
Research and energy High-temperature fixtures, shielding, and specialty test hardware Share operating environment and thermal cycling assumptions

CNC Machining Challenges

Tungsten machining is difficult because the material combines high hardness, high density, and limited ductility. These properties can increase cutting forces, accelerate tool wear, and make small features vulnerable to chipping. The production plan should be built around rigidity, conservative parameters, sharp tooling, coolant control, and realistic tolerance targets.

Challenge Practical Control Method
Tool wear Use suitable carbide or wear-resistant tooling and monitor tool life closely
Brittle edge damage Add sensible edge breaks, avoid fragile geometry, and control entry and exit cuts
High cutting forces Use rigid workholding, short tool overhang, and stable cutting paths
Heat at the cutting zone Tune speeds, feeds, coolant, and pass depth to protect the tool and part
Tolerance drift Inspect critical features during setup and confirm dimensions after finishing
Surface finish variation Define required roughness and whether polishing, grinding, or another finish is needed

Design Tips for Tungsten CNC Parts

  • Use tungsten only where density, heat resistance, shielding, or wear resistance is truly needed.
  • Prefer tungsten heavy alloy when the part needs better toughness and more predictable machinability.
  • Avoid extremely thin walls, knife edges, deep narrow slots, and sharp internal corners unless they are essential.
  • Call out critical dimensions clearly instead of applying tight tolerances across every feature.
  • Specify any required deburring, edge break, surface roughness, cleaning, or surface treatment.
  • Share service temperature, load, corrosion exposure, and inspection requirements with the supplier before quoting.

How MTSPi Approaches Difficult-Material RFQs

For tungsten and other difficult metals, MTSPi reviews the 3D model, 2D drawing, material callout, tolerance stack, surface finish, and expected quantity before committing to a process route. Depending on the geometry, the project may use CNC milling, CNC turning, grinding support, or multi-axis strategies such as 5-axis CNC machining. Inspection planning is handled through MTSPi’s quality assurance workflow so critical dimensions and documentation needs are clear.

FAQ

Is tungsten harder than steel?

Yes. Tungsten is harder and much denser than most common steels, which helps with wear resistance but also makes machining more difficult.

Can tungsten be CNC machined?

Yes. Tungsten can be CNC machined, but it requires appropriate tooling, rigid fixturing, controlled cutting parameters, and careful inspection.

Why is tungsten difficult to machine?

Its hardness, density, and brittleness can increase cutting force, tool wear, cracking risk, and tolerance-control difficulty.

What is the difference between tungsten and tungsten carbide?

Tungsten is a pure metal. Tungsten carbide is a tungsten-carbon compound known for extreme hardness and is often used in cutting tools and wear components.

Is tungsten more expensive than stainless steel?

Usually yes. Tungsten material and processing costs are typically higher, so the specification should be tied to a real performance need.

Related MTSPi Resources

Categories
Blog CNC Materials Guides Quality & Tolerances

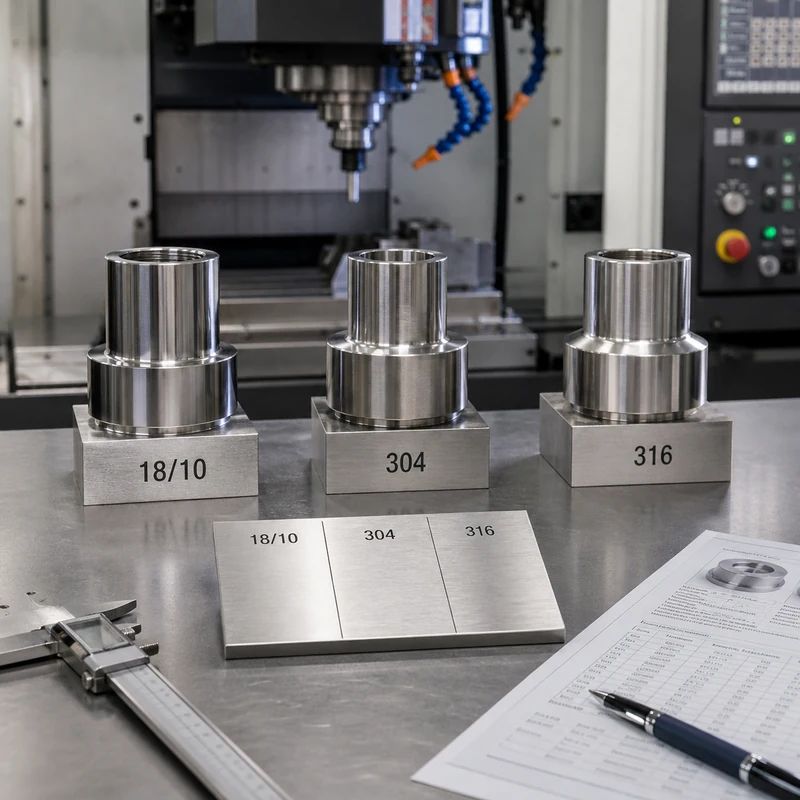
18/10 vs 304 vs 316 Stainless Steel for CNC Machined Parts

18/10, 304, and 316 stainless steel are often grouped together because all three are austenitic stainless options with useful corrosion resistance. For CNC machined parts, the practical question is not just which grade sounds better. The right choice depends on corrosion exposure, machining difficulty, material cost, surface finish, passivation needs, and inspection requirements. MTSPi supports stainless steel CNC machining for prototypes and production components where grade selection affects both performance and total cost.

Quick Answer: 18/10 vs 304 vs 316

18/10 stainless steel usually describes about 18 percent chromium and 10 percent nickel. It is close to the 304 stainless family and is common in food-contact and consumer applications. 304 is the common general-purpose stainless grade for industrial parts. 316 adds molybdenum, which improves resistance to chlorides, salt exposure, and pitting corrosion, but it normally costs more and requires more careful machining control.

Material Best Use Main CNC Note
18/10 stainless steel Decorative, food-related, and consumer stainless parts Confirm the actual certified grade if the drawing requires traceability
304 stainless steel General industrial brackets, shafts, housings, fittings, and food equipment Usually easier and more economical to machine than 316
316 stainless steel Marine, chemical, medical-style, pharmaceutical, and coastal components Better corrosion resistance, with higher cost and tool-wear risk

What 18/10 Stainless Steel Means

18/10 is a composition description. Chromium helps form the passive oxide film that protects stainless steel, while nickel stabilizes the austenitic structure and improves toughness and surface appearance. The term is useful for consumer goods, but it is not always precise enough for engineered CNC parts. If a component needs material certificates, regulated traceability, or a controlled standard, the drawing should call out the recognized stainless grade rather than only saying 18/10.

Why 304 Stainless Steel Is Common in CNC Parts

304 stainless steel is widely available and offers a strong balance of corrosion resistance, availability, formability, weldability, and cost. It is often the starting point for CNC metal machining when the part needs stainless performance but will not face heavy salt, chloride, or chemical exposure. It can still work harden and create stringy chips, so sharp tooling, coolant, and stable cutting parameters matter.

Where 316 Stainless Steel Performs Better

316 stainless steel is selected when corrosion risk is the leading concern. Its molybdenum content improves resistance to pitting and crevice corrosion in chloride-rich environments. That makes 316 a better candidate for marine hardware, washdown equipment, chemical processing components, medical-style instruments, outdoor assemblies, and parts that must tolerate aggressive cleaning. It is not automatically stronger or better for every part; its main advantage is corrosion resistance.

Factor 18/10 304 316
Typical role Commercial composition description General-purpose stainless grade Harsh-environment stainless grade
Chromium About 18 percent About 18 to 20 percent About 16 to 18 percent
Nickel About 10 percent About 8 to 10.5 percent About 10 to 14 percent
Molybdenum Usually none Usually none About 2 to 3 percent
Corrosion resistance Good in mild service Good for general service Best in chloride exposure
Machinability Similar to 304-family grades Usually better than 316 More demanding
Cost Often close to 304 Usually lower Usually higher

Corrosion Resistance and Service Environment

The largest difference appears around chlorides. 304 can perform well indoors, in clean freshwater exposure, and in many general industrial assemblies. If the part sees salt water, coastal air, aggressive washdown, chemical cleaning, or trapped moisture, 316 is often safer. Geometry still matters: crevices, blind pockets, poor drainage, and scratches can reduce corrosion performance even when the alloy is well chosen.

Environment Likely Starting Grade Reason
Dry indoor machinery 304 Severe corrosion resistance is usually unnecessary
Food-contact parts 304 or 316 Cleaning chemistry decides the better option
Coastal outdoor hardware 316 Chloride exposure increases pitting risk
Marine components 316 Salt exposure favors molybdenum-bearing stainless
Decorative consumer parts 18/10 or 304-family stainless Appearance and polish may matter more than extreme corrosion resistance

CNC Machining Differences

Both 304 and 316 can be machined accurately, but neither should be treated like free-machining steel. Austenitic stainless generates heat, can work harden, and may form burrs around holes, threads, slots, and thin edges. 316 is generally more difficult because it is tougher and can increase tool wear. For tight-tolerance parts, the RFQ should define critical dimensions, surface roughness, edge requirements, and whether inspection is needed before or after finishing.

Surface Finish and Passivation

Stainless performance depends on the finished surface, not only the alloy. Machining marks, embedded contamination, sharp burrs, and poor cleaning can reduce corrosion resistance. Depending on the application, stainless parts may need passivation, electropolishing, brushing, polishing, bead blasting, or another surface treatment. Post-finish dimensions should be specified when polishing or electropolishing could affect a critical tolerance.

How to Choose for a CNC Machined Part

Choose When It Makes Sense Check First
18/10 The part is cosmetic, consumer-facing, or food-related and certification is not critical Whether a recognized 304-family grade will actually be supplied
304 The part needs general corrosion resistance, good availability, and reasonable cost Exposure to chlorides, cleaning chemicals, and outdoor weather
316 The part faces salt, chemicals, medical-style cleaning, or corrosion-sensitive service Higher material cost, machining time, and finish requirements

RFQ Details That Prevent Material Mistakes

A complete RFQ helps the supplier quote the real requirement. Include the 3D model, 2D drawing, grade and standard, material certificate requirement, production quantity, finish, inspection level, and packaging needs. MTSPi’s CNC machining materials resources can help compare stainless steel with aluminum, brass, copper, titanium, and engineering plastics before the grade is locked.

Quality Checks for Stainless Parts

Material choice should connect directly to inspection. MTSPi can support dimensional checks, thread gauges, surface roughness review, visual inspection, and documentation through its quality assurance process. For corrosion-critical parts, finish certificates or passivation records may be just as important as dimensional results.

FAQ

Is 18/10 stainless steel the same as 304?

It is usually close to 304 in composition, but 18/10 is a composition description. Use a recognized grade callout when certification or traceability matters.

Is 316 always better than 304?

No. 316 is better for chloride, marine, chemical, and harsh cleaning exposure. For mild indoor or general industrial use, 304 may be more economical.

Which grade is easier to machine?

304 is generally easier to machine than 316. Both require sharp tools, coolant control, and appropriate cutting parameters to reduce work hardening and burrs.

Can MTSPi machine 304 and 316 stainless steel?

Yes. MTSPi can quote CNC milling, CNC turning, and multi-axis machining for stainless parts based on drawings, CAD files, quantity, finish, and inspection requirements.

Related MTSPi Resources

Categories
Blog Guides Quality & Tolerances

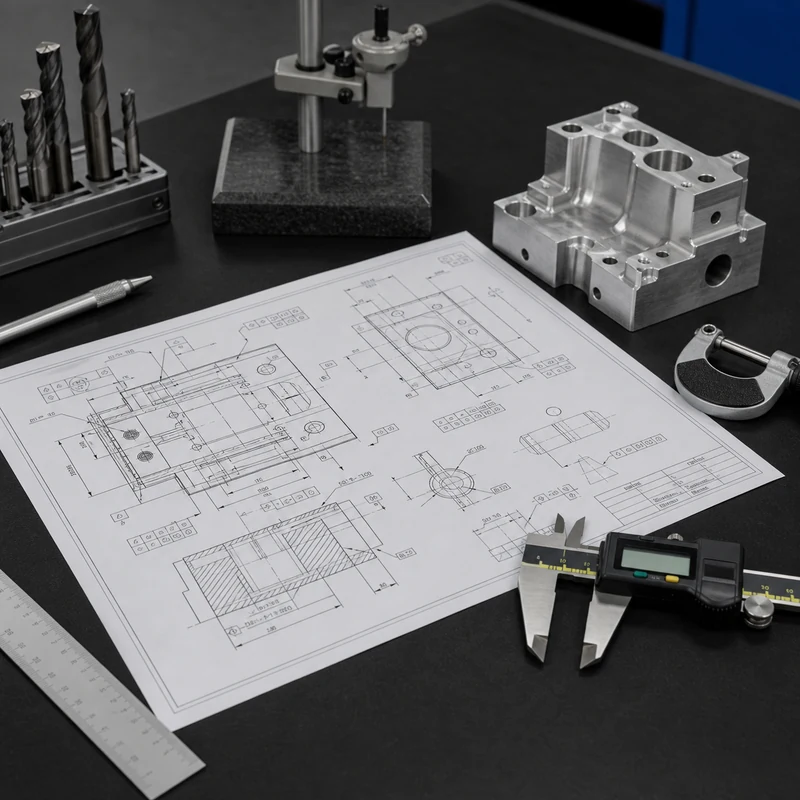
Engineering Drawing Symbols for CNC Machining Quotes

An engineering drawing is more than a picture of a part. For CNC machining, it defines dimensions, tolerances, materials, finishes, threads, inspection requirements, and notes that control how the part should be quoted and produced.

When symbols or abbreviations are missed, the result can be an inaccurate quote, the wrong toolpath, unnecessary rework, or a part that passes size checks but fails assembly. MTSPi reviews CNC machining drawings together with CAD files so unclear requirements are caught before production.

Why Drawing Symbols Matter

A small callout can change the whole manufacturing plan. A simple hole may need drilling only, while a counterbored and tapped hole may need several tools. A general tolerance may be easy to hold, while a tight position tolerance may require a more controlled setup and CMM inspection.

Drawing information What it affects Why it matters in quoting
Dimension Feature size and tool selection Defines the basic material removal plan.
Tolerance Process choice and inspection time Tight limits can add setup and measurement cost.
Surface finish Tooling, feed, finishing, or polishing Finish requirements can change cycle time.
Hole note Drilling, boring, tapping, counterboring Compound hole features need more operations.
GD&T Datum setup and measurement method Controls relationship between features, not just size.

Common Dimension and Feature Abbreviations

Abbreviation or symbol Meaning CNC machining note
DIA Diameter Used for holes, shafts, bosses, and circular features.
R Radius Affects cutter size, corner cleanup, and stress concentration.
TOL Tolerance Defines acceptable variation from nominal size.
REF Reference Information only unless the drawing states otherwise.
THK Thickness Important for plate, sheet, wall, and step features.
DP or DEPTH Depth Controls blind holes, pockets, slots, and threaded features.

Hole and Thread Callouts

Hole notes deserve careful review because they often combine several instructions in one short line. Diameter, depth, thread size, thread depth, countersink angle, counterbore diameter, and through-hole condition can all appear together.

Callout Meaning Manufacturing impact
THRU The hole passes through the part Tool must break through the full thickness.
TAP Internal thread required Needs tapping, thread milling, or forming depending on material.
CBORE Counterbore recess Adds a flat-bottom recess for a fastener head.
CSK Countersink Adds an angled recess and angle control.
M6 x 1 Metric thread size and pitch Requires matching thread tool and inspection gauge.

Fastener features also affect assembly and cost. If a part has many tapped holes, deep threads, or difficult counterbores, review them early with reduce CNC machining cost and the intended assembly method.

Surface Finish and Inspection Notes

Surface finish symbols and roughness values control how smooth a surface must be. A cosmetic face, sealing face, sliding surface, and hidden clearance pocket should not automatically receive the same finish requirement.

Requirement What to clarify Inspection method
Ra value Which surfaces need the value Roughness tester or agreed visual standard
No burrs Edges affected and acceptable break size Visual check, magnification, or edge standard
Critical dimension Sampling plan and report format Caliper, micrometer, pin gauge, CMM, or fixture
Flatness or parallelism Datum and measurement area CMM, surface plate, height gauge, or fixture

For parts with tight tolerances, ask how the supplier will measure the feature before machining starts. MTSPi connects the drawing to CNC machining quality inspection so the inspection plan matches the acceptance requirement.

GD&T Symbols in CNC Projects

Geometric Dimensioning and Tolerancing controls the shape, orientation, and location of features relative to datums. It is especially important when parts must assemble with other components or when hole patterns, flat surfaces, and mating features need controlled relationships.

GD&T concept Plain-English meaning CNC planning issue
Datum Reference feature used for measurement Fixture and inspection setup must match the drawing intent.
Position Allowed location error of a feature Hole patterns may need controlled setup and CMM reporting.
Flatness How much a surface may vary from flat Thin parts may need stress and clamping control.
Parallelism How closely one feature aligns with another Setup sequence and datum handling matter.
Runout Circular variation during rotation Turning process and chucking method are important.

File Package Checklist for an RFQ

  • 3D CAD file for geometry, preferably STEP or another neutral format.
  • PDF drawing with tolerances, material, finish, threads, and notes.
  • Quantity, target lead time, and whether prototypes or production batches are needed.
  • Critical features that affect assembly, sealing, motion, or appearance.
  • Inspection report, material certificate, or finish documentation requirements.

Clear drawing data helps the supplier choose between CNC milling service, CNC turning service, finishing, and inspection options without guessing.

Conclusion

Engineering drawing symbols and abbreviations turn design intent into manufacturing instructions. For CNC machining, the most important items are dimensions, tolerances, hole notes, surface finish, GD&T, material, and inspection requirements. A careful drawing review before quoting saves time, reduces ambiguity, and gives both buyer and supplier a clearer path to acceptable parts.

Categories
Blog CNC Materials Guides Quality & Tolerances

420 vs 316 Stainless Steel for CNC Machined Parts

420 and 316 stainless steel are both useful CNC materials, but they solve different engineering problems. One is normally chosen for hardness and wear resistance. The other is chosen when corrosion resistance, toughness, and long service life in wet or chemical environments matter more.

For a machined part, the right choice depends on load, exposure, surface finish, heat treatment, tolerance, and inspection requirements. MTSPi reviews these tradeoffs together with stainless steel CNC machining and the full part drawing before recommending a material route.

Quick Comparison

Requirement 420 stainless steel 316 stainless steel CNC buyer note
Stainless family Martensitic Austenitic Different structures create different machining and performance behavior.
Main advantage Hardness and wear resistance Corrosion resistance and toughness Start with the part’s failure risk, not just the alloy name.
Heat treatment Can be hardened Usually not hardened by heat treatment Specify target hardness if 420 is selected for wear.
Corrosion behavior Moderate Strong, especially around chlorides 316 is usually better for marine, medical, food, and chemical exposure.
Typical CNC use Shafts, tools, wear pads, molds, blades Housings, fittings, medical parts, marine parts Geometry and environment decide the final choice.

What 420 Stainless Steel Does Well

420 stainless steel contains enough carbon to be hardened by heat treatment. After hardening, it can provide higher surface hardness and better wear resistance than many common austenitic stainless grades. That makes it useful for parts that rub, slide, cut, or need to hold a working edge.

Common examples include shafts, valve parts, mold components, wear blocks, tooling features, and mechanical parts where corrosion exposure is limited. When the part includes milled pockets, turned diameters, slots, or threaded features, MTSPi may compare CNC milling service and CNC turning service routes to control distortion and finish.

Where 316 Stainless Steel Is Stronger

316 stainless steel is usually selected when the part must survive moisture, cleaning chemicals, salt exposure, or biological and food-contact environments. Its molybdenum content improves resistance to chloride attack, which is why buyers often consider it for marine, medical, chemical, and food-processing components.

316 is not the best choice when maximum hardness is the primary requirement, but it is often a better long-term material for parts exposed to corrosive service. It also pairs well with finishing and cleaning requirements planned through surface treatment.

Machinability and Production Planning

Manufacturing factor 420 stainless steel 316 stainless steel
Tool wear Depends heavily on hardness condition Can work harden if cutting is not controlled
Heat control Important after hardening or near tight features Important because heat and rubbing can worsen work hardening
Burr risk Varies with heat treatment and feature size Can be noticeable on small holes, slots, and thin edges
Inspection focus Hardness, wear surfaces, critical diameters Corrosion-critical surfaces, finish, dimensions, passivation notes

A material that looks cheaper on paper can become expensive if it needs extra passes, slower cutting, special inspection, or post-machining treatment. The RFQ should include material condition, quantity, finish, hardness if needed, and which dimensions are critical.

How to Choose Between 420 and 316

Choose this priority Better starting point Reason
High hardness after heat treatment 420 stainless steel It can be hardened for wear and edge retention.
Marine or chloride exposure 316 stainless steel It offers stronger corrosion resistance.
Medical or cleaning-heavy environment 316 stainless steel It is commonly used where corrosion resistance and cleanliness matter.
Wear part in a mostly dry environment 420 stainless steel Hardness may matter more than corrosion resistance.
General corrosion-resistant CNC component 316 stainless steel It is often the safer choice when exposure is uncertain.

Drawing and Quality Notes

If 420 is chosen for hardness, state the target hardness range and whether heat treatment occurs before or after machining. If 316 is chosen for corrosion resistance, state any passivation, polishing, cleaning, or surface roughness requirements. These details should appear in CNC machining drawings so quoting, machining, and inspection use the same assumptions.

For higher-risk parts, combine material certificates, dimensional reports, hardness checks, and surface finish checks through CNC machining quality inspection. This reduces the chance that a material choice looks correct but fails at receiving inspection or in service.

Conclusion

Choose 420 stainless steel when hardness, wear resistance, and heat-treatable strength are the main design goals. Choose 316 stainless steel when corrosion resistance, toughness, and long-term stability in wet or chemical environments are more important. For CNC machined parts, the best decision comes from matching material behavior to the real operating environment, not from treating all stainless steels as interchangeable.

Categories
Blog Design, Cost & Sourcing Quality & Tolerances

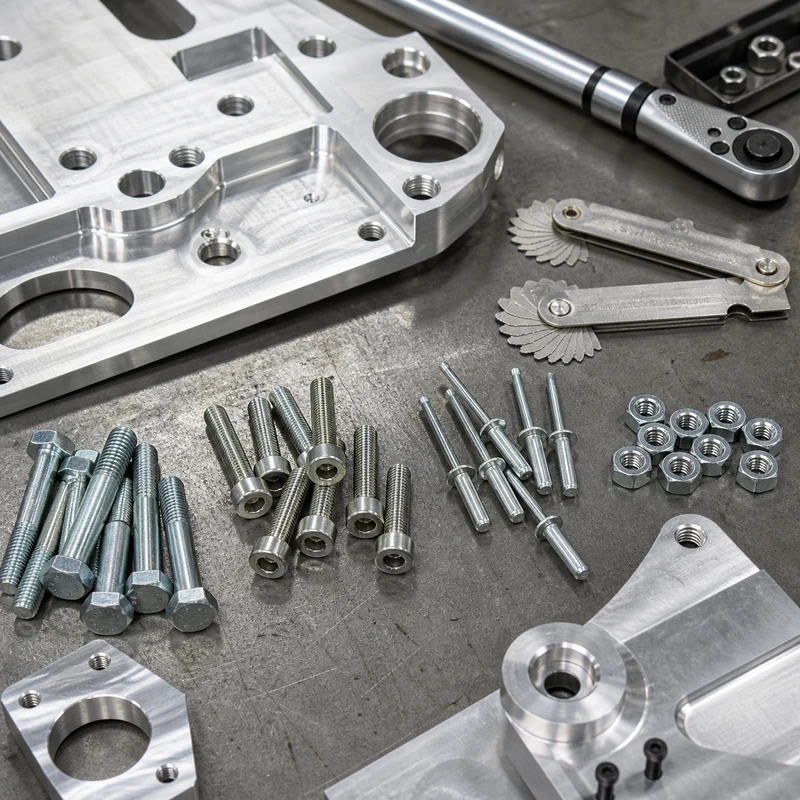
Bolt vs Screw vs Rivet vs Nut: Fastener Choices for CNC Parts

Bolts, screws, rivets, and nuts all join parts, but they do it in different ways. Choosing the wrong fastener can create assembly delays, weak clamping, damaged threads, difficult maintenance, or unnecessary machining cost.

For CNC machined parts, fastener selection should be reviewed with material, wall thickness, access direction, thread depth, tolerance, finish, and service load. These details are best included early in CNC machining drawings rather than solved after parts are cut.

Quick Comparison

Fastener How it works Typical connection CNC design note
Bolt External thread clamps parts, usually with a nut Removable Needs clearance holes, access, and suitable bearing area.
Screw Threads into a tapped hole or directly into material Removable Needs thread engagement and enough wall thickness.
Rivet Deforms during installation to lock parts together Permanent Useful when future disassembly is not expected.
Nut Internal thread pairs with a bolt or threaded rod Removable threaded joint Needs wrench access and anti-loosening plan if vibration exists.

When to Use Bolts

Bolts are useful when a strong, serviceable joint is needed. They are common in machine frames, fixtures, housings, structural brackets, and assemblies that need maintenance access. A bolt usually works with a nut, although a tapped component can sometimes replace the nut.

In CNC parts, designers should confirm head clearance, tool access, washer or bearing surface, grip length, and whether the bolt will load the part in tension, shear, or both.

When to Use Screws

Screws are often chosen when the assembly is compact or when the fastener must thread directly into the machined part. Machine screws in tapped holes are common in covers, enclosures, instrument housings, panels, and precision fixtures.

The key design issue is thread engagement. Soft materials such as aluminum or plastic may need more thread depth, inserts, or a larger diameter. MTSPi can review material choice through CNC material options before the threaded features are finalized.

When to Use Rivets

Rivets create a permanent mechanical joint. They can be useful for sheet metal, light structures, covers, and assemblies where loosening must be avoided and future disassembly is not required. Some rivets can be installed from one side, which helps when rear access is limited.

The tradeoff is repairability. Removing a rivet usually damages or changes the joint, so rivets should not be used where routine service, adjustment, or repeated inspection access is expected.

What Nuts Add to an Assembly

Nuts are not usually used alone. They complete a threaded joint with a bolt or threaded rod. Hex nuts, lock nuts, flange nuts, and prevailing-torque nuts solve different access and vibration problems.

For CNC machined assemblies, nut access should be checked in the model. A strong joint on paper can become expensive if there is no room for a socket, wrench, washer, or locking feature.

Design Checks for CNC Machined Fastener Features

Design check Why it matters Practical action
Thread depth Too little engagement can strip threads Match thread length to material and load.
Edge distance Holes too close to edges can crack or deform Leave enough material around holes.
Counterbore and countersink Head style affects surface fit and tool access Call out dimensions clearly on the drawing.
Vibration Threaded joints can loosen Consider lock nuts, thread lockers, washers, or rivets.
Finish buildup Coatings can affect threads and holes Plan masking or post-finish thread checks.

Fastener choices also affect machining cost. Extra tapped holes, deep threads, tight position tolerances, and difficult counterbores can increase cycle time. Review these details with reduce CNC machining cost if the assembly has many fasteners.

Conclusion

Use bolts for strong removable joints, screws for compact threaded fastening, rivets for permanent connections, and nuts to complete bolted assemblies. The best choice depends on load, access, service needs, material, and machining cost. Define the fastener strategy early so the CNC parts are easier to make, inspect, assemble, and maintain.

Categories
Blog Industries & Applications Quality & Tolerances

Aerospace CNC Machining Supplier Evaluation Guide for 2026

Aerospace CNC machining places heavy demands on geometry control, material knowledge, documentation, and consistency. A useful supplier evaluation should look beyond a list of machine names and focus on whether the shop can control risk across the full manufacturing route.

For MTSPi customers, the evaluation starts with part geometry, tolerance stack, material, finish, quantity, and required evidence. Those inputs help determine whether a job belongs on 5-axis machining, a turning center, a Swiss-type machine, or a simpler milling process.

What Aerospace Buyers Should Evaluate First

Evaluation point What good looks like Why it matters
Process capability The supplier can explain setup, access, fixturing, and datum strategy Complex parts fail when the route is vague.
Material experience Clear plan for aluminum, titanium, stainless, and nickel alloy behavior Aerospace materials can move, work harden, or wear tools quickly.
Inspection CMM or suitable measurement plan tied to drawing risk Tight tolerances need evidence, not assumptions.
Documentation Revision control, material records, and inspection reports Receiving teams need traceable proof.
Production fit Prototype, low-volume, or repeat-batch process is clear Capacity should match the program stage.

Machine Capability Is Only Part of the Answer

A 5-axis machine is valuable for angled features, compound surfaces, and reduced setups, but it does not automatically make a supplier qualified. Programming, toolpath verification, workholding, cutter selection, and inspection access decide whether the part can be produced reliably.

Simple aerospace brackets may still be best handled by CNC milling service. Shafts, pins, sleeves, and threaded features may need CNC turning service or Swiss-type machining. The practical route depends on the drawing, not on a marketing label.

Material and Finish Questions

Aluminum, titanium, stainless steel, and nickel alloys each need different cutting and finishing controls. If the part requires anodizing, passivation, polishing, bead blasting, or other surface treatment, the supplier should consider finish allowance before final machining.

Ask whether the shop has experience with the exact material grade, stock form, wall thickness, and inspection features on your drawing. A general claim of aerospace capability is not enough for a difficult component.

Inspection Planning for Aerospace Parts

Inspection should be planned before cutting starts. Critical datums, hole positions, profiles, thread depths, flatness, perpendicularity, and surface finish callouts may each require different tools. MTSPi aligns these requirements through CNC machining quality inspection so the final report supports real acceptance criteria.

Part feature Common concern Useful control
Thin wall pocket Distortion after roughing Balanced stock removal and interim checks
Datum hole pattern Position error across setups Stable fixture and CMM report
Titanium bracket Heat, tool wear, and burrs Controlled parameters and deburring plan
Precision shaft Runout and diameter repeatability Turning process with suitable gauge checks

Questions to Ask Before Sending an RFQ

  • Which features drive the machining route?
  • What tolerance or GD&T callouts add the most cost?
  • Can the supplier suggest design changes that reduce risk without changing function?
  • What inspection evidence will be supplied with the parts?
  • How will prototype feedback transfer into the next production batch?

Conclusion

Aerospace supplier selection is not about copying a ranking. It is about finding a machining partner that can explain the process, control the material, inspect the critical features, and provide documentation that matches the project risk. A clear evaluation checklist makes that decision more defensible.

Categories
Blog Industries & Applications Quality & Tolerances

How to Evaluate Medical CNC Machining Suppliers in 2026

Medical CNC machining requires more than accurate cutting. Buyers need a supplier that can understand device function, material traceability, surface condition, inspection records, and repeatable production controls. A low quote is not helpful if the part cannot be validated later.

This guide reframes supplier selection into practical checks that engineering and purchasing teams can use before ordering prototypes or production parts from a custom CNC machining services provider.

Start With the Part Risk

Not every medical component carries the same level of risk. A fixture, diagnostic enclosure, surgical instrument component, and implant-related prototype have different documentation and process needs. Before comparing suppliers, define how the part is used, what surfaces are critical, and which dimensions affect function.

Review area What to confirm Why it matters
Material Exact grade, certificate need, and biocompatibility expectation Prevents substitutions that create validation issues.
Tolerance Critical dimensions, datum structure, and inspection method Keeps precision focused where the device needs it.
Finish Ra value, polishing, passivation, anodizing, or cleaning needs Controls contact surfaces, corrosion, and assembly behavior.
Documentation Inspection report, material certificate, and revision control Supports receiving inspection and engineering records.

Material Experience Matters

Common medical machining materials include stainless steel, titanium, aluminum, cobalt alloys, PEEK, and other engineering plastics. Each behaves differently during cutting and finishing. MTSPi can review options such as titanium CNC machining, stainless steel CNC machining, and PEEK CNC machining when buyers need a practical material route.

The supplier should be able to explain tool wear, burr risk, heat control, cleaning expectations, and whether the selected finish is compatible with the material. For small parts, the workholding plan can be just as important as the machine list.

Prototype and Production Are Different Tests

A supplier that can make one good prototype is useful, but medical programs often need stable repeatability. Ask how the shop controls setup changes, inspection frequency, lot traceability, and feedback from prototype runs into low-volume production.

For early development, speed and engineering feedback may matter most. For repeated orders, the focus shifts toward process stability, revision discipline, packing, and consistent inspection evidence.

Inspection Capabilities to Ask About

Feature type Typical inspection method Supplier question
Tight hole position CMM, optical measurement, or fixture check How is datum setup controlled?
Small turned features Micrometer, pin gauge, thread gauge, or CMM Can the process hold size across the lot?
Surface finish Visual standard and roughness measurement Which surfaces need controlled finish?
Threads Go/no-go gauge and drawing callout review Are thread class and depth unambiguous?

Inspection should match the failure mode. For practical planning, combine the drawing with quality assurance expectations before production begins.

Supplier Evaluation Checklist

  • Can the supplier explain the machining sequence and likely risk points?
  • Does the quote identify material grade, finish, tolerance, and inspection scope?
  • Can prototype feedback be carried into production without losing revision control?
  • Are burrs, cleaning, and packaging addressed for small or delicate parts?
  • Will the inspection report match the drawing features that matter most?

Conclusion

The right medical CNC machining supplier is the one that can connect material choice, machining strategy, inspection, and documentation into a controlled workflow. A strong evaluation process helps buyers avoid vague quotes and move from prototype to repeatable production with fewer surprises.

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

How to Evaluate Medical CNC Machining Suppliers in 2026

We'll Send You Back with Price Immediately!