Categories
Blog Design, Cost & Sourcing Manufacturing Process Comparisons

How to Evaluate Injection Molding Companies in the USA: A 2026 Supplier Guide

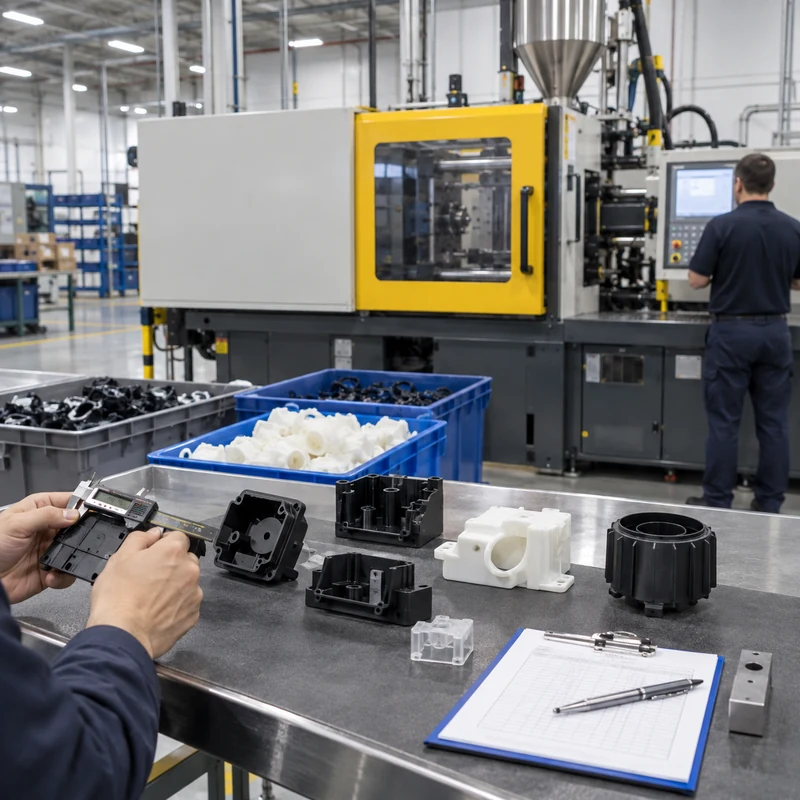
Searching for injection molding companies in the USA produces long lists, but a supplier’s location or machine count does not show whether it fits your part. The useful question is whether its tooling, process control, material experience, quality system, capacity, communication, and commercial model match your program.

This guide provides a repeatable selection method for product teams. It does not rank companies by marketing visibility. Instead, it shows how to build a shortlist and compare evidence before committing to tooling.

Quick Supplier Selection Framework

Start with the part and program, not the supplier list. Define annual volume, resin, part size, cosmetic class, tolerance, regulatory needs, assembly content, target launch, and expected design changes. Eliminate suppliers that cannot support the required press size, resin family, documentation, or validation. Audit the remaining candidates using the same scorecard.

Eight Criteria That Matter Most

Criterion Evidence to request Risk if ignored
Tooling capability Mold design review, toolroom scope, maintenance plan Slow changes and recurring defects
Material experience Similar resin examples and drying controls Warp, splay, brittleness, color variation
Process control Documented windows and setup records Lot-to-lot inconsistency
Quality system Inspection plan, calibration, traceability Undetected defects and weak containment
Capacity Press availability and contingency plan Launch or replenishment delays
Engineering support DFM examples and mold-flow capability Tooling that locks in avoidable problems
Secondary operations Assembly, inserts, decorating, packaging Extra suppliers and handling risk
Commercial fit Transparent tooling ownership and change terms Unexpected fees and difficult transfers

Match the Supplier to Your Production Stage

A prototype or bridge program values speed, flexible tooling, and frequent engineering communication. A stable high-volume program values automation, cavity efficiency, preventive maintenance, material purchasing leverage, and dependable replenishment. A regulated program adds validation, traceability, change control, and record retention.

One supplier may be excellent at complex medical molding but expensive for a simple industrial housing. Another may run commodity resins efficiently but lack the engineering depth for optical parts or tight-tolerance inserts. Capability must be evaluated against the actual part family.

Tooling Questions to Ask Before Purchase

  • Who owns the mold, CAD data, and spare components?
  • Where will the mold be built, sampled, maintained, and stored?
  • What steel, insert, hot-runner, cooling, venting, and ejection approach is proposed?
  • How many shots is the quoted tool expected to support?
  • What is included in the sampling and approval cycle?
  • How are engineering changes priced and documented?
  • Can the mold be transferred, and is it compatible with another press base?

Quality and Validation

Request a control plan that links drawing requirements to measurement methods and sampling frequency. Critical dimensions may need a capability study. Cosmetic surfaces need an approved limit sample and controlled lighting. Materials may require certificates, lot traceability, moisture control, or regulatory declarations.

First Article Inspection is useful, but it is not the entire validation. A few acceptable parts do not prove a stable process. Ask how the supplier establishes the molding window and verifies performance across normal material, machine, cavity, and environmental variation.

Total Cost Beyond Piece Price

Cost component What to compare
Tooling Build, samples, spares, maintenance, modifications
Unit cost Resin, cycle time, cavities, labor, scrap
Quality Inspection, validation, containment, returns
Logistics Freight, packaging, inventory, emergency shipments
Change risk Revision speed and cost before design freeze
Program support Engineering time, reporting, communication

When a Hybrid Supply Chain Makes Sense

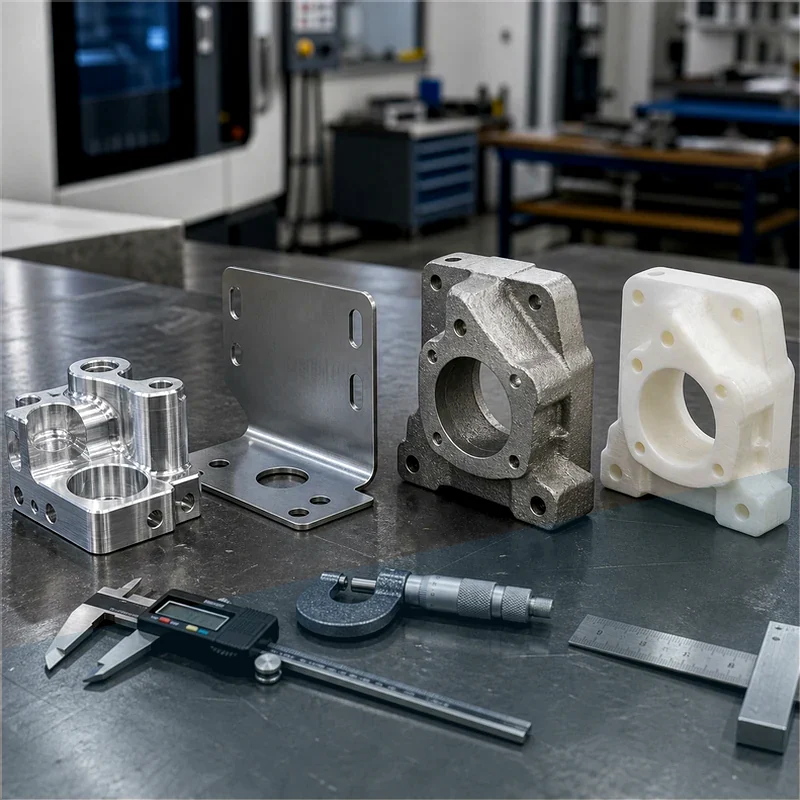
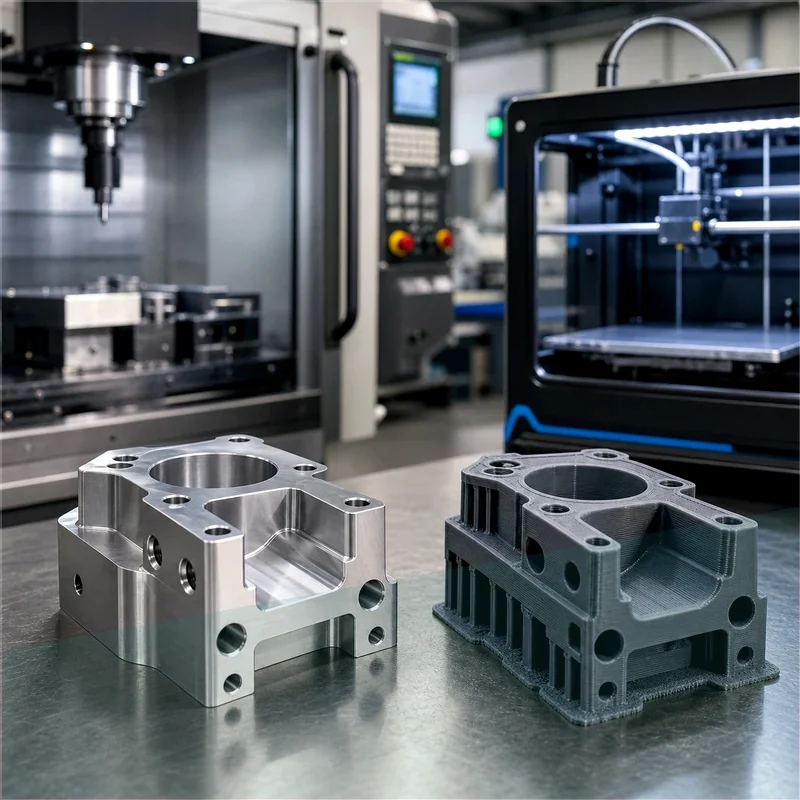
Some teams combine US molding with overseas tooling, CNC prototypes, or low-volume bridge production. This can balance response time and cost, but only when ownership, tolerances, data exchange, and responsibility are explicit. Before cutting a production mold, CNC-machined or printed prototypes can verify assembly, ergonomics, fastener access, and major dimensions.

Red Flags During Supplier Review

  • A quote arrives with no questions about draft, wall thickness, gate location, resin, or tolerance.
  • The supplier cannot explain how critical dimensions will be controlled.
  • Tool ownership and transfer terms are vague.
  • Every defect is treated as an inspection problem rather than a process problem.
  • Capacity claims are not supported by a launch or contingency plan.
  • Communication changes after the purchase order is issued.

Practical RFQ Package

Send a clean 3D model, controlled 2D drawing, expected volumes, resin specification, color and cosmetic standard, mating-part information, packaging needs, validation level, and launch schedule. Identify must-have requirements separately from preferences. This gives each supplier the same basis and makes quotations easier to compare.

Frequently Asked Questions

Should I choose the lowest injection molding quote?

Not automatically. Compare the included tool construction, sample cycles, process validation, maintenance, quality controls, logistics, and change terms. A low quote with weak assumptions can create a higher total program cost.

How many suppliers should receive an RFQ?

Three to five qualified suppliers is usually enough for a meaningful comparison. A very broad RFQ can consume time without improving the decision if candidates have not been screened for fit.

Can CNC machining reduce injection molding risk?

Yes. CNC prototypes in production-intent material can validate geometry, assembly, threads, flatness, and interfaces before mold steel is committed.

Related MTSPi CNC Resources

Categories
Blog Design, Cost & Sourcing Quality & Tolerances

Welding Symbols Explained: Meaning, Types, and Drawing Notes for Machined Assemblies

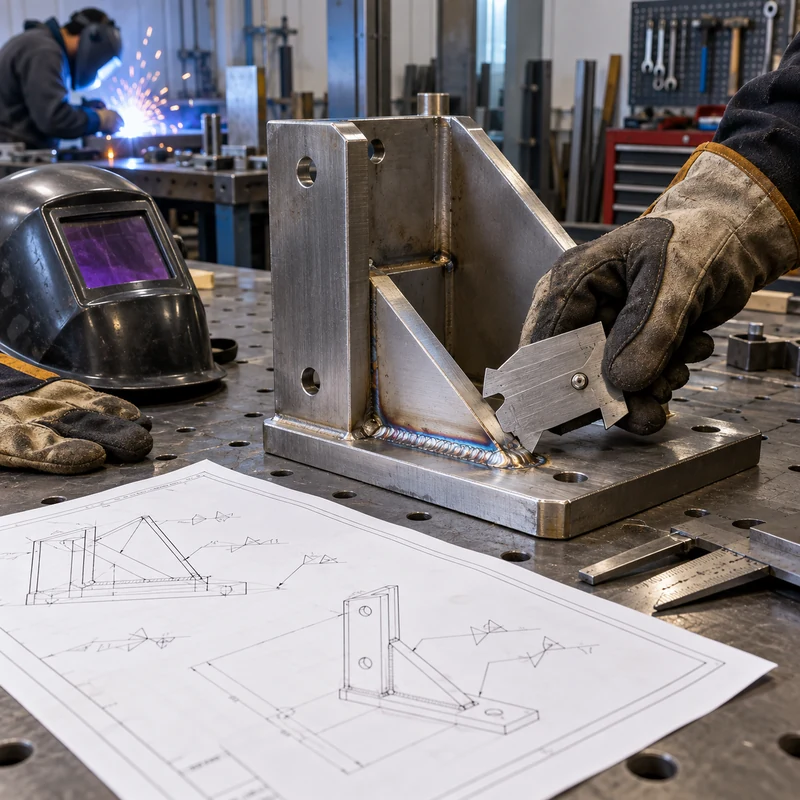
Welding symbols turn an assembly requirement into a compact manufacturing instruction. A few lines and numbers can define the joint, weld type, side, size, length, spacing, contour, finish, and whether the operation happens in the shop or in the field. That compression is useful, but it also means one missed mark can change cost, distortion, accessibility, and inspection.

This guide explains the notation from the viewpoint of designers and buyers of machined assemblies. It focuses on how weld callouts interact with CNC datums, post-weld machining, sealing surfaces, and quotation risk.

Quick Answer: How Do You Read a Welding Symbol?

Follow the same sequence every time: trace the arrow to the joint, identify the governing standard, check which side of the reference line contains the basic symbol, read size information on the left, read length and pitch on the right, then inspect the arrow-reference junction and contour marks for supplementary requirements.

Anatomy of a Welding Symbol

The arrow points to the physical joint. The horizontal reference line carries the weld information. An optional tail can identify the welding process, procedure, specification, or drawing note. A circle at the arrow junction generally indicates an all-around weld, while a flag indicates a field weld.

On drawings that follow AWS conventions, a symbol below the reference line applies to the arrow side and a symbol above applies to the other side. Symbols on both sides call for welding on both faces. ISO drawings can use different reference-line logic, so the title block or general notes must state the standard.

Common Weld Types and Their Uses

Weld type Typical symbol form Common application Machining implication
Fillet Triangle T-joints, lap joints, brackets Heat can pull machined faces out of position
Square groove Parallel edges Thin butt joints Edge squareness and root gap affect penetration
V or bevel groove Angled groove Thicker structural joints Preparation may be milled before welding
U or J groove Curved preparation Heavy sections with controlled filler volume Usually needs dedicated edge preparation
Plug or slot Hole or slot notation Joining overlapping plates Hole location and fit influence load transfer
Spot or seam Resistance-weld notation Sheet-metal enclosures Access and electrode clearance must be designed

How Fillet Weld Dimensions Work

The dimension to the left of a fillet symbol normally controls weld size. Information to the right controls weld length and, for intermittent welds, pitch. A continuous weld may have no length value. When welds appear on both sides, the symbols indicate whether the pattern is aligned or staggered.

Oversizing a fillet does not automatically improve an assembly. It adds heat, filler, time, and distortion. Specify the size required by the load and code, then decide whether intermittent welding can reduce heat without compromising fatigue, sealing, corrosion, or stiffness.

Groove Welds, Root Opening, and Penetration

Groove callouts describe both the weld and the edge preparation. The drawing may identify preparation depth, root opening, groove angle, backing, and complete or partial joint penetration. These details strongly affect labor because deeper preparation requires more cutting, filler, passes, cleaning, and inspection.

For a welded component that will be finish machined, leave enough material around the joint and critical surfaces. The machining allowance must cover predictable distortion without making the section unnecessarily heavy.

Contour and Finish Symbols

Flush, convex, and concave contour marks define the required weld profile. A letter may define the finishing method, such as grinding or machining. A flush requirement should be tied to function: bearing clearance, sealing, cosmetic appearance, or interference avoidance. Applying it everywhere can add substantial cost without improving performance.

AWS and ISO Welding Symbols

Topic AWS-style drawing ISO-style drawing
Reference line Usually one line May use a solid and dashed line
Side indication Above or below the line Depends on the selected ISO system
Fillet size Commonly leg size May identify throat or leg with a prefix
Units Often inches on US drawings Commonly millimetres
Best practice State AWS edition State ISO edition and system

Designing Machined Parts for Welding

  • Separate locating datums from heat-affected areas whenever possible.
  • Add tabs, slots, shoulders, or pilot features to make fixture positioning repeatable.
  • Provide torch access and space for clamps, backing, and inspection tools.
  • Machine sealing faces, precision bores, and bearing seats after welding when distortion cannot be tolerated.
  • Define whether dimensions apply before or after welding and finishing.
  • Use a realistic datum scheme for post-weld inspection rather than relying on free-state dimensions alone.

Weld Inspection Checklist

Inspection should match the consequence of failure. Visual checks can verify location, continuity, contour, undercut, porosity, and obvious cracking. Dimensional inspection checks distortion and feature position. Dye penetrant, magnetic particle, ultrasonic, or radiographic methods may be required for critical joints, but the drawing should identify the acceptance standard instead of leaving the shop to guess.

Common Drawing Errors

  • Mixing AWS and ISO conventions on one drawing.
  • Calling out a full-length weld when intermittent welding was intended.
  • Omitting the governing standard, units, or weld procedure reference.
  • Placing a weld where a tool, torch, or inspection probe cannot reach.
  • Requiring a ground-flush contour without identifying which surface controls function.
  • Dimensioning precision holes before welding with no allowance for post-weld correction.

Frequently Asked Questions

What does a circle at the arrow junction mean?

It normally calls for welding around the complete perimeter of the indicated joint. Confirm the governing standard and ensure every segment is physically accessible.

What is the difference between arrow side and other side?

The arrow side is the face indicated by the arrow. The other side is the opposite face. The symbol position maps the requirement to one or both faces according to the drawing standard.

Should precision features be machined before or after welding?

Rough machining can occur before welding, but tight bores, flat sealing faces, and positional features are often finished afterward so the machining operation removes weld-induced distortion.

Related MTSPi CNC Resources

Categories
Blog Guides Manufacturing Process Comparisons

SLA vs DLP Resin 3D Printing: Accuracy, Surface Finish, and Prototype Selection

SLA vs DLP Resin 3D Printing: Accuracy, Surface Finish, and Prototype Selection is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains SLA vs DLP from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Choose SLA or DLP based on part size, detail, surface finish, resin choice, and throughput. For final functional validation, compare printed resin limitations with CNC machined plastics or metals before approving the design.

Key Differences at a Glance

Point Option A Option B
Light method Laser traces each layer Projected image cures a layer
Speed Depends on scan length and geometry Often fast for full-layer exposure
Detail Very fine details possible Pixel size affects edge detail
Surface Smooth resin finish Smooth, sometimes pixel-related texture
Best use High-detail prototypes and appearance models Fast resin prototypes and small batches

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Use resin printing for appearance, fine detail, and early fit review.
  • Avoid assuming printed resin equals production ABS, nylon, aluminum, or steel.
  • Plan supports on non-critical surfaces when appearance matters.
  • Check thin walls and small pins against the printer and resin capability.
  • Use CNC machining for final material and tolerance validation.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

SLA vs DLP matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog Guides Manufacturing Process Comparisons

SLA vs FDM 3D Printing: Choosing the Right Prototype Before CNC Machining

SLA vs FDM 3D Printing: Choosing the Right Prototype Before CNC Machining is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains SLA vs FDM from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Choose SLA for smooth visual models and fine details. Choose FDM for quick, low-cost functional mockups, larger prototypes, and early fit checks. Move to CNC machining when the prototype must match production material, tolerance, surface finish, or strength.

Key Differences at a Glance

Point Option A Option B
Material Photopolymer resin Thermoplastic filament
Surface finish Smooth and detailed Visible layer lines
Strength Resin-dependent, sometimes brittle Better for basic functional handling
Cost Moderate, depends on resin and finishing Usually low for early prototypes
Best use Appearance, fine detail, small features Fit checks, fixtures, larger simple forms

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Use SLA when small details or smooth surfaces drive the review.
  • Use FDM when speed, size, and basic function matter more than appearance.
  • Do not validate tight production tolerances with low-resolution printed parts.
  • Prototype threaded or snap-fit features carefully because printed behavior differs from machined or molded parts.
  • Move critical functional tests to CNC or production-equivalent processes.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

SLA vs FDM matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog Design, Cost & Sourcing Manufacturing Process Comparisons

What Is Welding? Process Basics, Joint Types, and Machined-Part Design Notes

What Is Welding? Process Basics, Joint Types, and Machined-Part Design Notes is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains what is welding from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Welding is best for joining fabricated structures and metal assemblies. If a surface must remain flat, round, sealed, or tightly located, plan post-weld CNC machining or use a design that protects precision features from heat distortion.

Key Differences at a Glance

Point Option A Option B
MIG welding General fabrication and production assemblies Spatter, heat input, distortion
TIG welding Precise welds and thin materials Slower speed, operator skill
Spot welding Sheet metal overlap joints Access to both sides
Laser welding Small, precise, lower heat input joints Joint fit-up and equipment cost
Resistance welding High-volume sheet assemblies Material and thickness limits

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Place precision datums away from weld beads when possible.
  • Use tabs, slots, fixtures, or pilot features to control assembly location.
  • Allow access for the torch, electrode, or laser path.
  • Specify weld size and location clearly instead of using vague notes.
  • Plan post-weld machining for sealing faces, bearing seats, and critical holes.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

what is welding matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog CNC Materials Manufacturing Process Comparisons

Aluminum Gravity Casting: Process, Design Rules, and CNC Finishing Options

Aluminum Gravity Casting: Process, Design Rules, and CNC Finishing Options is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains aluminum gravity casting from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Use aluminum gravity casting for medium-volume aluminum parts with cast-friendly geometry and functional strength needs. Use CNC finishing for critical dimensions that casting alone cannot hold reliably.

Key Differences at a Glance

Point Option A Option B
Shape creation Mold forms near-net geometry Material is removed from stock
Best use Repeated cast shapes with moderate complexity Tight features, prototypes, precision interfaces
Tolerance Moderate before machining Tight when setup is controlled
Surface Cast texture or finished after processing Machined texture or specified finish
Tooling Mold required Fixtures and cutting tools required

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Keep wall thickness transitions gradual to reduce shrink and hot spots.
  • Add machining allowance on critical surfaces.
  • Avoid isolated heavy sections unless feeding and cooling are designed.
  • Define which surfaces are as-cast and which are CNC machined.
  • Plan datum strategy before mold tooling is finalized.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

aluminum gravity casting matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog Design, Cost & Sourcing Industries & Applications

Multilayer PCB Guide for Mechanical Engineers: Design, Enclosures, Heat, and CNC Interfaces

Multilayer PCB Guide for Mechanical Engineers: Design, Enclosures, Heat, and CNC Interfaces is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains multilayer PCB from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Multilayer PCBs need early mechanical coordination. Board outline, mounting holes, keepouts, connector locations, thermal pads, and shielding requirements should be frozen before machining enclosures or fixtures.

Key Differences at a Glance

Point Option A Option B
Board outline Controls fit inside housing Use current PCB STEP or DXF data
Standoffs Affects board stress and assembly height Machine stable bosses with correct clearance
Thermal pads Moves heat from components Create flat contact surfaces and controlled gaps
Connectors Need alignment with openings Inspect port position and tolerance stack
EMI Metal can shield or interfere Plan grounding and clearance zones

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Import PCB STEP files into the enclosure CAD model.
  • Add tolerance around connectors based on both PCB and machining variation.
  • Avoid unsupported board spans near heavy connectors or buttons.
  • Define conductive and non-conductive contact areas clearly.
  • Use prototype enclosures to validate assembly before production.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

multilayer PCB matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog Manufacturing Process Comparisons Quality & Tolerances

Precision Metal Stamping: What Determines Part Accuracy and When CNC Is Better

Precision Metal Stamping: What Determines Part Accuracy and When CNC Is Better is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains precision metal stamping from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Stamping is ideal for high-volume sheet metal parts with repeatable 2D or formed features. CNC machining is better when quantities are low, geometry is thicker or more complex, tolerances are very tight, or the design is still changing.

Key Differences at a Glance

Point Option A Option B
Best volume Medium to high volume Prototype to low-volume precision batches
Tooling Dedicated die required Soft tooling and fixtures
Geometry Sheet metal cuts and forms 3D shapes, pockets, bores, threads
Design changes Can be expensive after hard tooling Easier to revise
Accuracy drivers Die wear, springback, material thickness Machine rigidity, toolpath, setup, inspection

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Use generous bend radii where possible to reduce cracking and springback variation.
  • Keep holes away from bends unless the tooling plan supports them.
  • Define burr direction when assembly or safety is affected.
  • Prototype critical interfaces with CNC or soft tooling before hard dies.
  • Do not choose stamping only because the final volume is uncertain.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

precision metal stamping matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog CNC Milling & Turning Design, Cost & Sourcing

Counterbore vs Countersink Holes: Design Differences, Uses, and CNC Machining Notes

Counterbore vs Countersink Holes: Design Differences, Uses, and CNC Machining Notes is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains counterbore vs countersink from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Use a counterbore for socket head cap screws, washers, and flat bearing seats. Use a countersink for flat-head screws where the conical head must sit flush with the surface.

Key Differences at a Glance

Point Option A Option B
Shape Cylindrical recess with flat floor Conical recess
Fastener Socket head cap screw, bolt head, washer Flat-head screw
Seat contact Flat bearing surface Angled bearing surface
Common angle Not angle-based 82, 90, or 100 degrees depending on standard
Inspection Diameter and depth Angle, major diameter, flushness

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Specify pilot hole diameter, counterbore diameter, counterbore depth, and tolerance where needed.
  • For countersinks, specify included angle and acceptable flushness if appearance matters.
  • Leave enough wall thickness around recessed holes to prevent breakout.
  • Avoid placing counterbores too close to edges, ribs, or deep pocket walls.
  • Match the hole callout to the actual fastener standard.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

counterbore vs countersink matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Categories
Blog Design, Cost & Sourcing Manufacturing Process Comparisons

SLM vs SLA: How to Choose Between Metal and Resin 3D Printing

SLM vs SLA: How to Choose Between Metal and Resin 3D Printing is a practical manufacturing question because the answer affects cost, lead time, material behavior, inspection, and the path from prototype to production. For MTSPi CNC customers, the key is not simply naming a process, but understanding how the process connects with machined parts, fixtures, tolerances, surface requirements, and final assembly.

This guide explains SLM vs SLA from an engineering and purchasing point of view. It is written for product developers, mechanical engineers, sourcing teams, and buyers who need clear decisions rather than generic process descriptions.

Quick Answer

Choose SLM when the part needs metal strength, complex internal geometry, lightweight structures, or functional metal prototypes. Choose SLA when the goal is smooth resin models, cosmetic prototypes, fit checks, or detailed concept parts at lower cost.

Key Differences at a Glance

Point Option A Option B
Material Metal powders such as aluminum, stainless, titanium Photopolymer resins
Strength Functional metal performance after correct processing Plastic-like, resin-dependent behavior
Surface Often needs post-processing Usually smooth as printed
Cost Higher machine and powder cost Lower for visual and fit prototypes
Post-processing Support removal, heat treatment, CNC finishing Cleaning, curing, sanding, painting

How the Process Choice Affects Real Parts

A manufacturing method should be selected around the feature that actually controls function. Cosmetic surfaces, hidden support features, threads, bores, sealing faces, heat-transfer areas, and assembly datums do not carry the same risk. When those requirements are mixed together without priority, quotes become inconsistent and production becomes harder to control.

The safest workflow is to define the part requirement first, then match the process. A printed prototype may answer shape questions, a molded sample may answer appearance questions, and a CNC machined sample may answer tolerance, material, and functional questions. Many successful projects use more than one method before the final design is locked.

Design and Manufacturing Considerations

  • Use SLM for metal features that cannot be made efficiently by milling or turning alone.
  • Use SLA for visual models, ergonomic checks, and assembly reviews before cutting metal.
  • Do not assume printed tolerances are the same as CNC-machined tolerances.
  • Add machining stock to SLM features that need precise bores, sealing faces, or threads.
  • Select resin by test purpose: appearance, heat resistance, transparency, or fit check.

Cost, Lead Time, and Risk Factors

Cost is driven by setup, tooling, material, machine time, inspection, finishing, and revision risk. A low unit price is not always the lowest project cost if it creates rework later. For prototypes and low-volume orders, flexibility can be more valuable than a process with a lower theoretical unit cost.

  • Use standard materials and standard feature sizes when they do not weaken the design.
  • Separate critical tolerances from general dimensions so the supplier knows where to focus.
  • Confirm surface finish and cosmetic requirements before production begins.
  • Avoid late changes to mounting holes, connector openings, datum faces, and threaded features.
  • Send CAD files and 2D drawings together when tolerances, threads, or finishes matter.

Quality Checks Before Production

A good quality plan checks the features that influence assembly and performance. Depending on the part, this may include dimensional inspection, thread gauges, surface roughness, flatness, perpendicularity, burr control, coating thickness, visual appearance, and fit with mating parts.

When This Topic Matters for CNC Buyers

SLM vs SLA matters when a team is comparing prototype routes, validating a design, replacing a weak supplier, or trying to reduce manufacturing cost without damaging function. The best choice is usually the process that answers the current engineering question with the least unnecessary risk.

MTSPi CNC Engineering Notes

MTSPi CNC supports precision CNC milling, turning, rapid prototyping, low-volume production, finishing, and inspection for custom parts. If your project uses molding, casting, welding, PCB assemblies, or 3D printing, CNC machining can still be important for datums, holes, threads, sealing faces, fixtures, and production-ready prototypes.

Frequently Asked Questions

Can this process replace CNC machining?

Sometimes it can replace CNC for non-critical geometry, but CNC is often still needed when tight tolerances, real engineering material, threads, flat sealing faces, or precise mating features are required.

What files help MTSPi CNC review a project?

STEP or STP files are useful for geometry. A 2D drawing is important for tolerances, materials, threads, surface finish, inspection requirements, and notes that are not obvious from the CAD model.

How do I reduce manufacturing risk?

Define critical features, avoid unnecessary tight tolerances, confirm material and finish requirements, and use prototypes to validate assembly before committing to higher-volume tooling or production.

Related MTSPi Resources

Request A Quote

We'll Send You Back with Price Immediately!

DEC 1-31

XMAS SPECEIL

Up to

40% off

SLM vs SLA: How to Choose Between Metal and Resin 3D Printing

We'll Send You Back with Price Immediately!